Company introduction
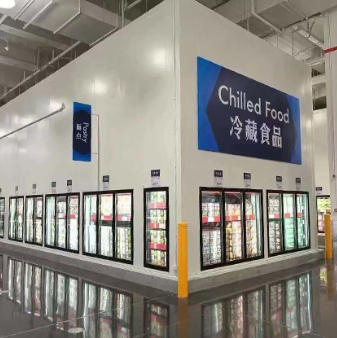
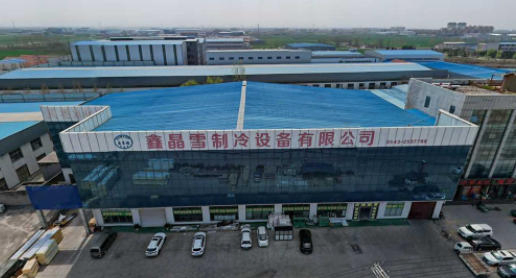
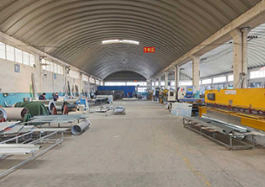
Shandong Xinrong Refrigeration Co., Ltd is a comprehensive refrigeration equipment enterprise integrating R&D, manufacturing and sales. Its main business covers refrigerated display cabinets, refrigerated warehouses, commercial refrigerators, compressors and related components. The company has established a full-chain professional team covering product research and development, process design, lean production and quality control, providing high-reliability and high-response service to global buyers. In terms of technological research and development as well as product delivery, the company possesses the ability to independently iterate on core technologies for commercial refrigeration equipment. It focuses on breaking through key technologies such as precise temperature control algorithms, efficient energy-saving structural design, and modular integration optimization. It can quickly convert diversified and dynamic customer demands from the international market into customized product solutions. For different terminal application scenarios (such as supermarkets, chain restaurants, medical institutions, and convenience stores), the company can flexibly adapt to key parameters such as voltage system, size, and functional configuration, achieving highly customized products that truly meet the differentiated needs of overseas customers. In terms of cost management, the company has achieved vertical integration throughout the entire process from raw material procurement, core component manufacturing, large-scale assembly to global distribution. This has effectively avoided the efficiency losses and cost increments caused by multi-level agency and outsourcing collaboration. Relying on a stable supply chain system and large-scale production capacity, the company significantly reduces the unit manufacturing cost while ensuring quality, thereby forming a stepped pricing mechanism with competitiveness and flexibility in the B2B international trade platform. In terms of delivery guarantee, the company has an independently controllable production planning system and does not rely on third-party outsourcing. It can implement dynamic production scheduling based on the urgency of foreign trade orders, the customer's level, and the delivery cycle, ensuring the timely delivery of high-priority orders (including rush orders). The sales and production departments implement an end-to-end direct connection mechanism, with real-time synchronization of order information, which increases the efficiency of demand changes, replenishment instructions, and technical collaboration responses by more than 50%, significantly enhancing the order fulfillment rate and customer satisfaction. In terms of quality control and after-sales service, the company implements a full-process quality management system covering the three stages of "incoming materials - process - factory delivery". All products have obtained mainstream international safety and energy efficiency certifications such as CE and UL, meeting the entry requirements of target markets. At the same time, the company has its own professional technical support team, providing full-life-cycle after-sales support including installation and commissioning, remote diagnosis, spare parts supply, on-site maintenance and technical training, to ensure that customers can use the products without worries.
Company video
R&D Capacity
- R&D Engineers
- 1 people
- Customization Options
- Customization from Samples, Customization from Designs, Full Customization, Minor Customization, Flexible customization
- ODM Service Available
- Yes
- OEM Service Available
- Yes
- New Products Launched in Last Year
- No
Trade Capacity
- Export Year
- 2 years
- Main Markets
- Europe
- Nearest Port
- Qingdao Port
- Terms of Payment
- LC, T/T, PayPal, Western Union
- Average Lead Time
- Peak Season Lead Time: within 15 workdays Off Season Lead Time: within 15 workdays
- Overseas Agent/Branch
- No
- Supply Chain Partners
- 8
- Minimum Order Quantity
- Negotiable
- Number of Foreign Trading Staff
- 2
- International Commercial Terms(Incoterms)
- CIF, FOB, CFR, EXW
General Information
- Address
- Binzhou, Shandong, China
- Plant Area
- 500 square meters
- Business Type
- Trading Company
- Main Products
- Refrigeration Equipment, Display Refrigerator, Beverage Cooler, Refrigeration Unit, Refrigeration Compressor, Condensing Unit, Cold Storage Room, Cold Room Panel
- Registered Capital
- 3,000,000 RMB
- Number of Employees
- 3
- Repeat Buyers Choice
- 30%~50%
- Year of Establishment
- 2023-05-08
- Cooperated with Fortune 500
- No