Company introduction
Anhui Xinben Mechanical & Electrical Engineering Co., Ltd. Boasts solid industrial experience, mature manufacturing technologies and a sound R&D system. The company is an integrated manufacturer specialized in the design, customized development, precision production and global sales of new energy batteries and energy storage solutions, covering complete services of product research and development, production, sales and after-sales support. Headquartered in Hefei, a core hub of China's new energy manufacturing and technological innovation, the company enjoys superior geographical conditions, complete industrial supporting facilities, convenient transportation and sufficient talent reserves, which underpin its steady development and continuous technical upgrading in the new energy industry. Through years of in-depth industry cultivation, we have built a diversified and professional product system tailored for various new energy storage scenarios. Our core product lineup includes high-safety, long-cycle lithium iron phosphate battery packs, intelligent residential energy storage batteries for household power supply and peak-valley power regulation, high-efficiency lithium-ion batteries serving as premium alternatives to traditional lead-acid batteries, and integrated large-scale energy storage power stations for industrial, commercial and grid-level energy storage projects. Different from ordinary manufacturers with single product lines, we focus on customized solution development based on differentiated customer needs and application scenarios. We provide targeted one-stop energy storage solutions for diverse demands, ranging from small-capacity outdoor portable power supplies and medium-capacity home energy storage devices to high-stability large-capacity energy supply systems for industrial parks, commercial facilities and communication base stations, fully meeting global diversified market requirements. Strong manufacturing capacity and reliable product quality form our core competitive strengths. To ensure stable, consistent and high-quality products, our production base is equipped with advanced intelligent production equipment and professional testing systems. Fully automated assembly lines enable standardized, large-scale and streamlined production, effectively reducing manual errors, improving production efficiency and product yield, and ensuring stable mass delivery for orders of all sizes. We adopt professional high-efficiency aging equipment for battery performance verification. All finished batteries and packs undergo long-term aging tests under simulated real working conditions to eliminate potential performance degradation and circuit instability risks, guaranteeing stable and durable performance during long-term operation. We have established a high-precision international-standard testing laboratory, which professionally tests key battery indicators such as capacity, internal resistance, cycle life, safety performance and temperature adaptability. It supports full-process testing from raw material inspection and semi-finished product testing to finished product calibration and R&D verification. Our rigorous full-cycle quality control ensures excellent product flexibility, stability and reliability. Even under volatile market conditions and fluctuating raw material prices, we maintain stable production capacity and sufficient inventory, ensuring reliable delivery and credible service for global customers. We adopt standardized management to ensure stable product quality and sustainable operation. Certified with ISO 9001 quality management system, we standardize all procedures from R&D, production and inspection to sales and after-sales service for continuous quality and efficiency improvement. Most of our products are equipped with CE, RoHS and UN 38.3 certifications, removing global market access barriers and boosting our overseas development.
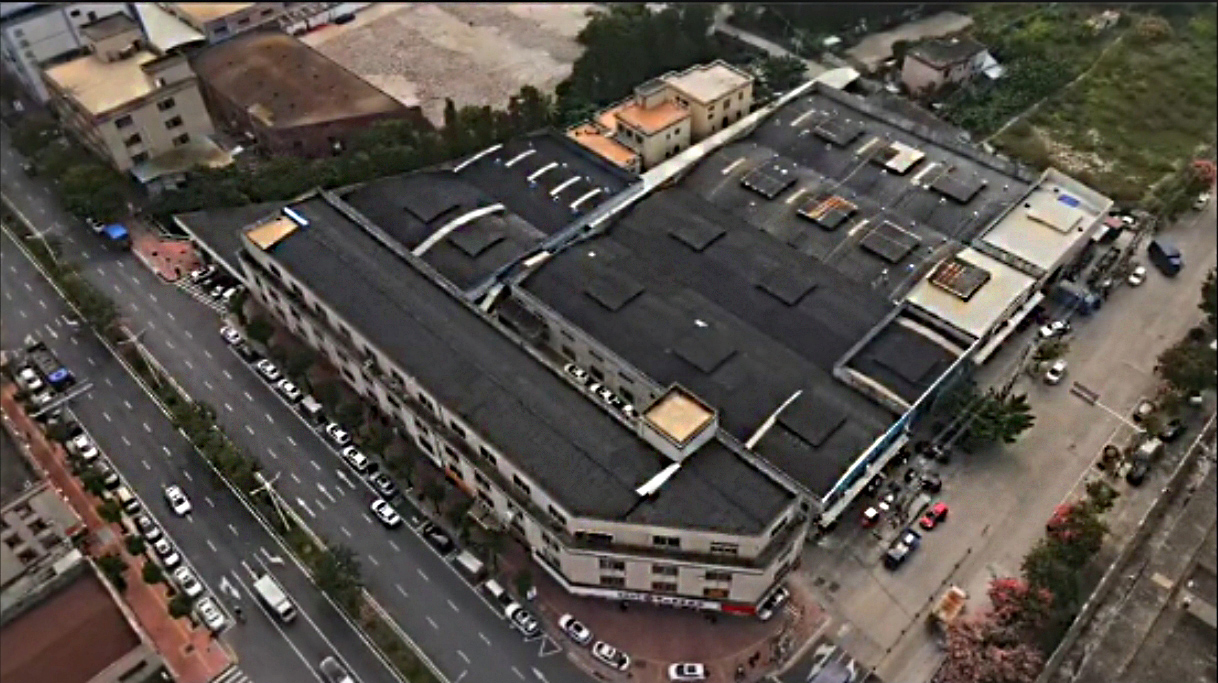
Company video
R&D Capacity
- R&D Engineers
- 1 people
- Customization Options
- Customization from Samples, Customization from Designs, Full Customization, Flexible customization, Minor Customization
- ODM Service Available
- Yes
- OEM Service Available
- Yes
Trade Capacity
- Export Year
- 2012-01-01
- Main Markets
- North America, South America, Eastern Europe, Southeast Asia, Africa, Oceania, Mid East, Eastern Asia, Western Europe
- Nearest Port
- SHENZHEN, SHANGHAI
- Terms of Payment
- LC, T/T, PayPal, Western Union
- Average Lead Time
- Peak Season Lead Time: one month Off Season Lead Time: within 15 workdays
- Overseas Agent/Branch
- No
- Supply Chain Partners
- 5
- Minimum Order Quantity
- 5 Sets
- Number of Foreign Trading Staff
- 3
- International Commercial Terms(Incoterms)
- FOB, EXW, CFR, CIF, DDP, DAP
General Information
- Address
- Room 230, Hanhai Chuanggu Entrepreneurship Park, 1858 Innovation Avenue, Changning Community Service Center, High tech Zone, Hefei City, Anhui Province
- Plant Area
- 122 square meters
- Main Products
- Home Energy Storage System, C&I Energy Storage System
- Registered Capital
- 5,000,000 RMB
- Number of Employees
- 10
- Repeat Buyers Choice
- 30%~50%
- Year of Establishment
- 2019-11-19
- Cooperated with Fortune 500
- No