Company introduction
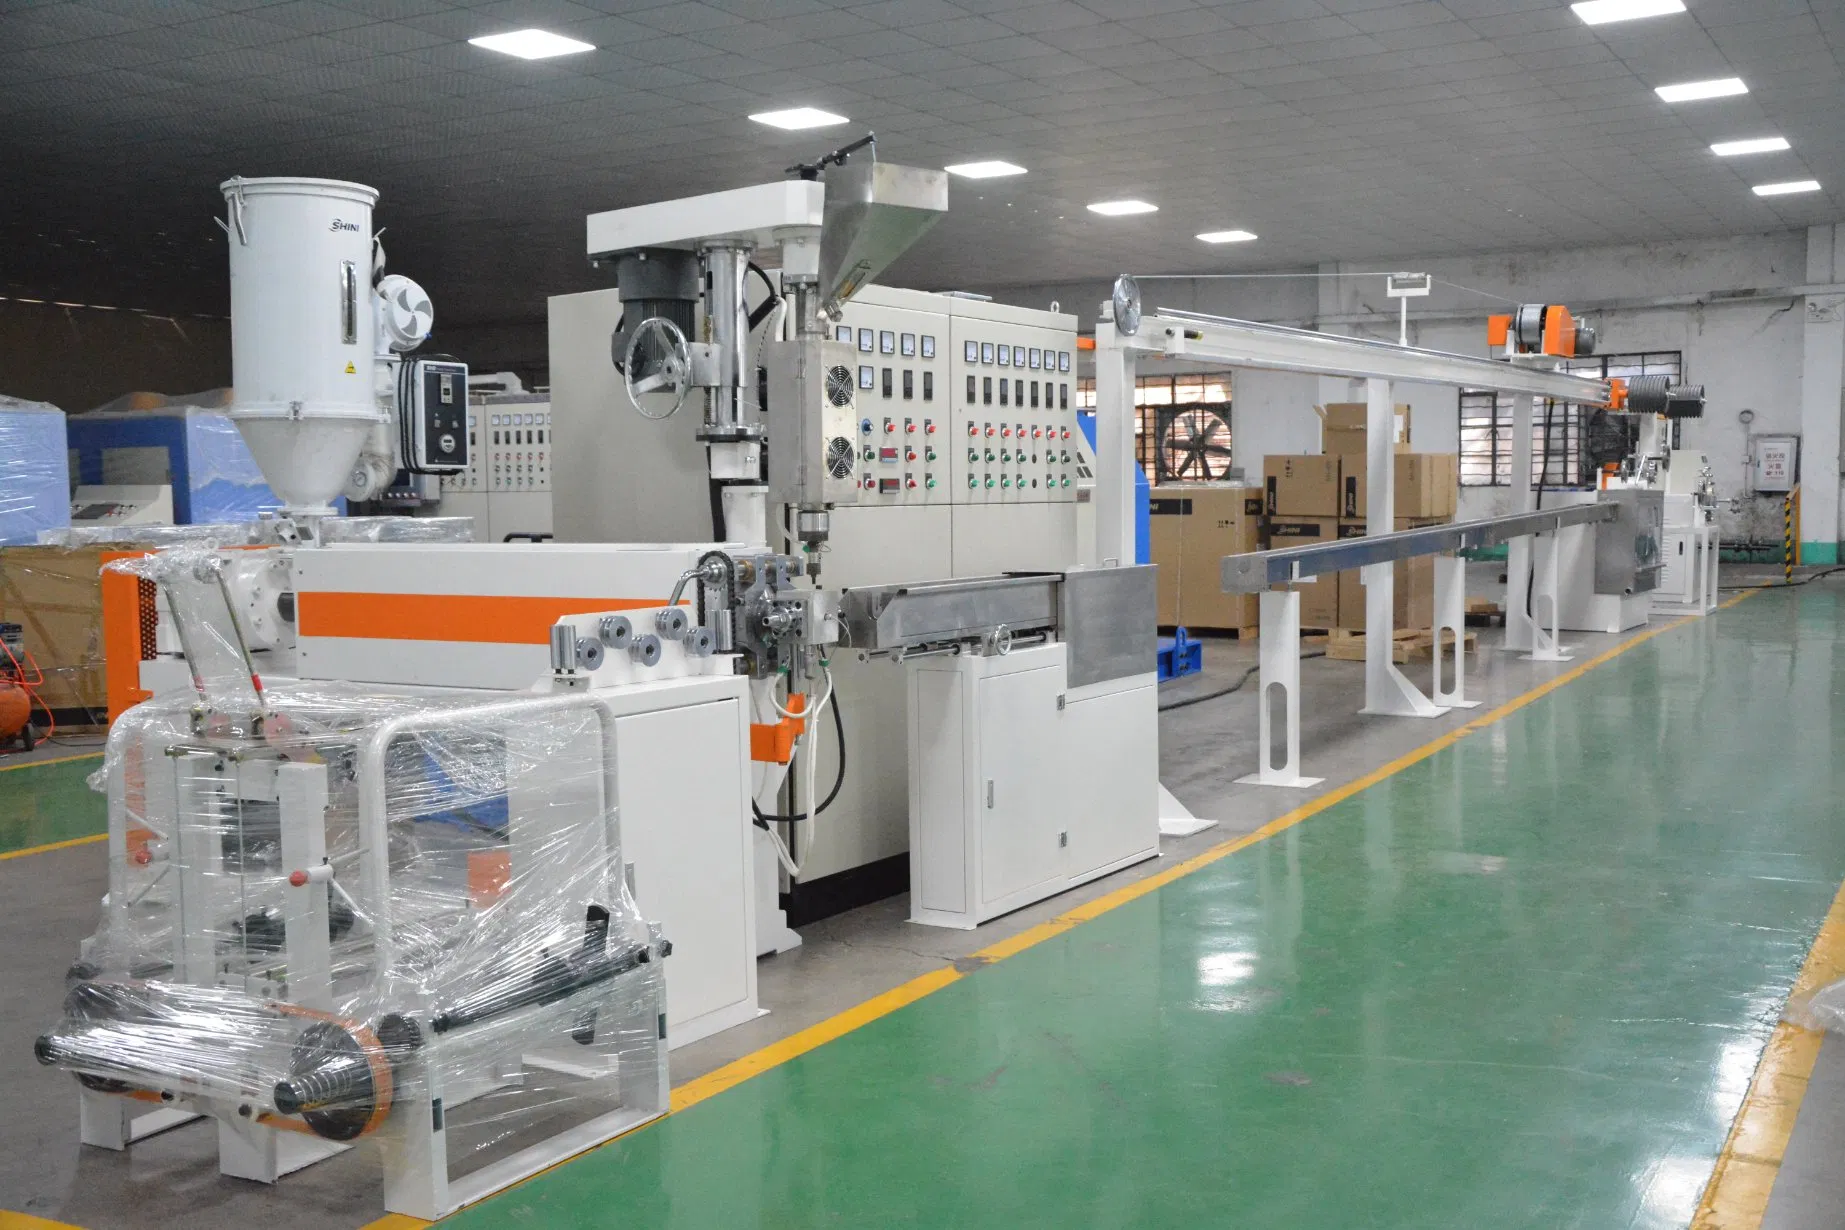
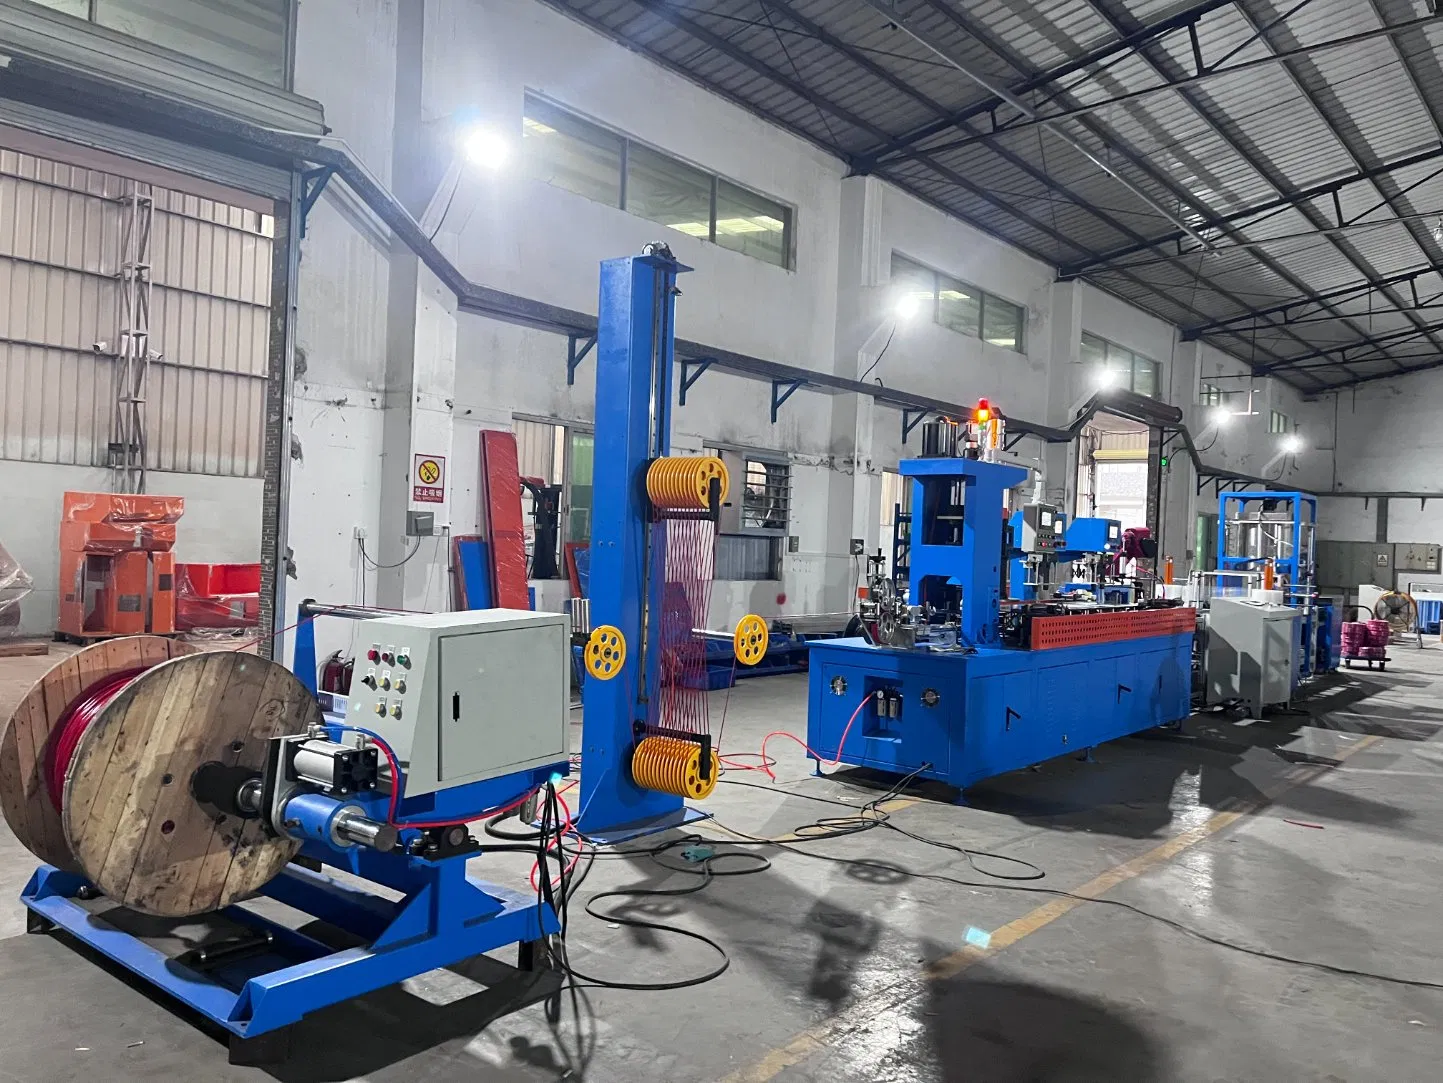
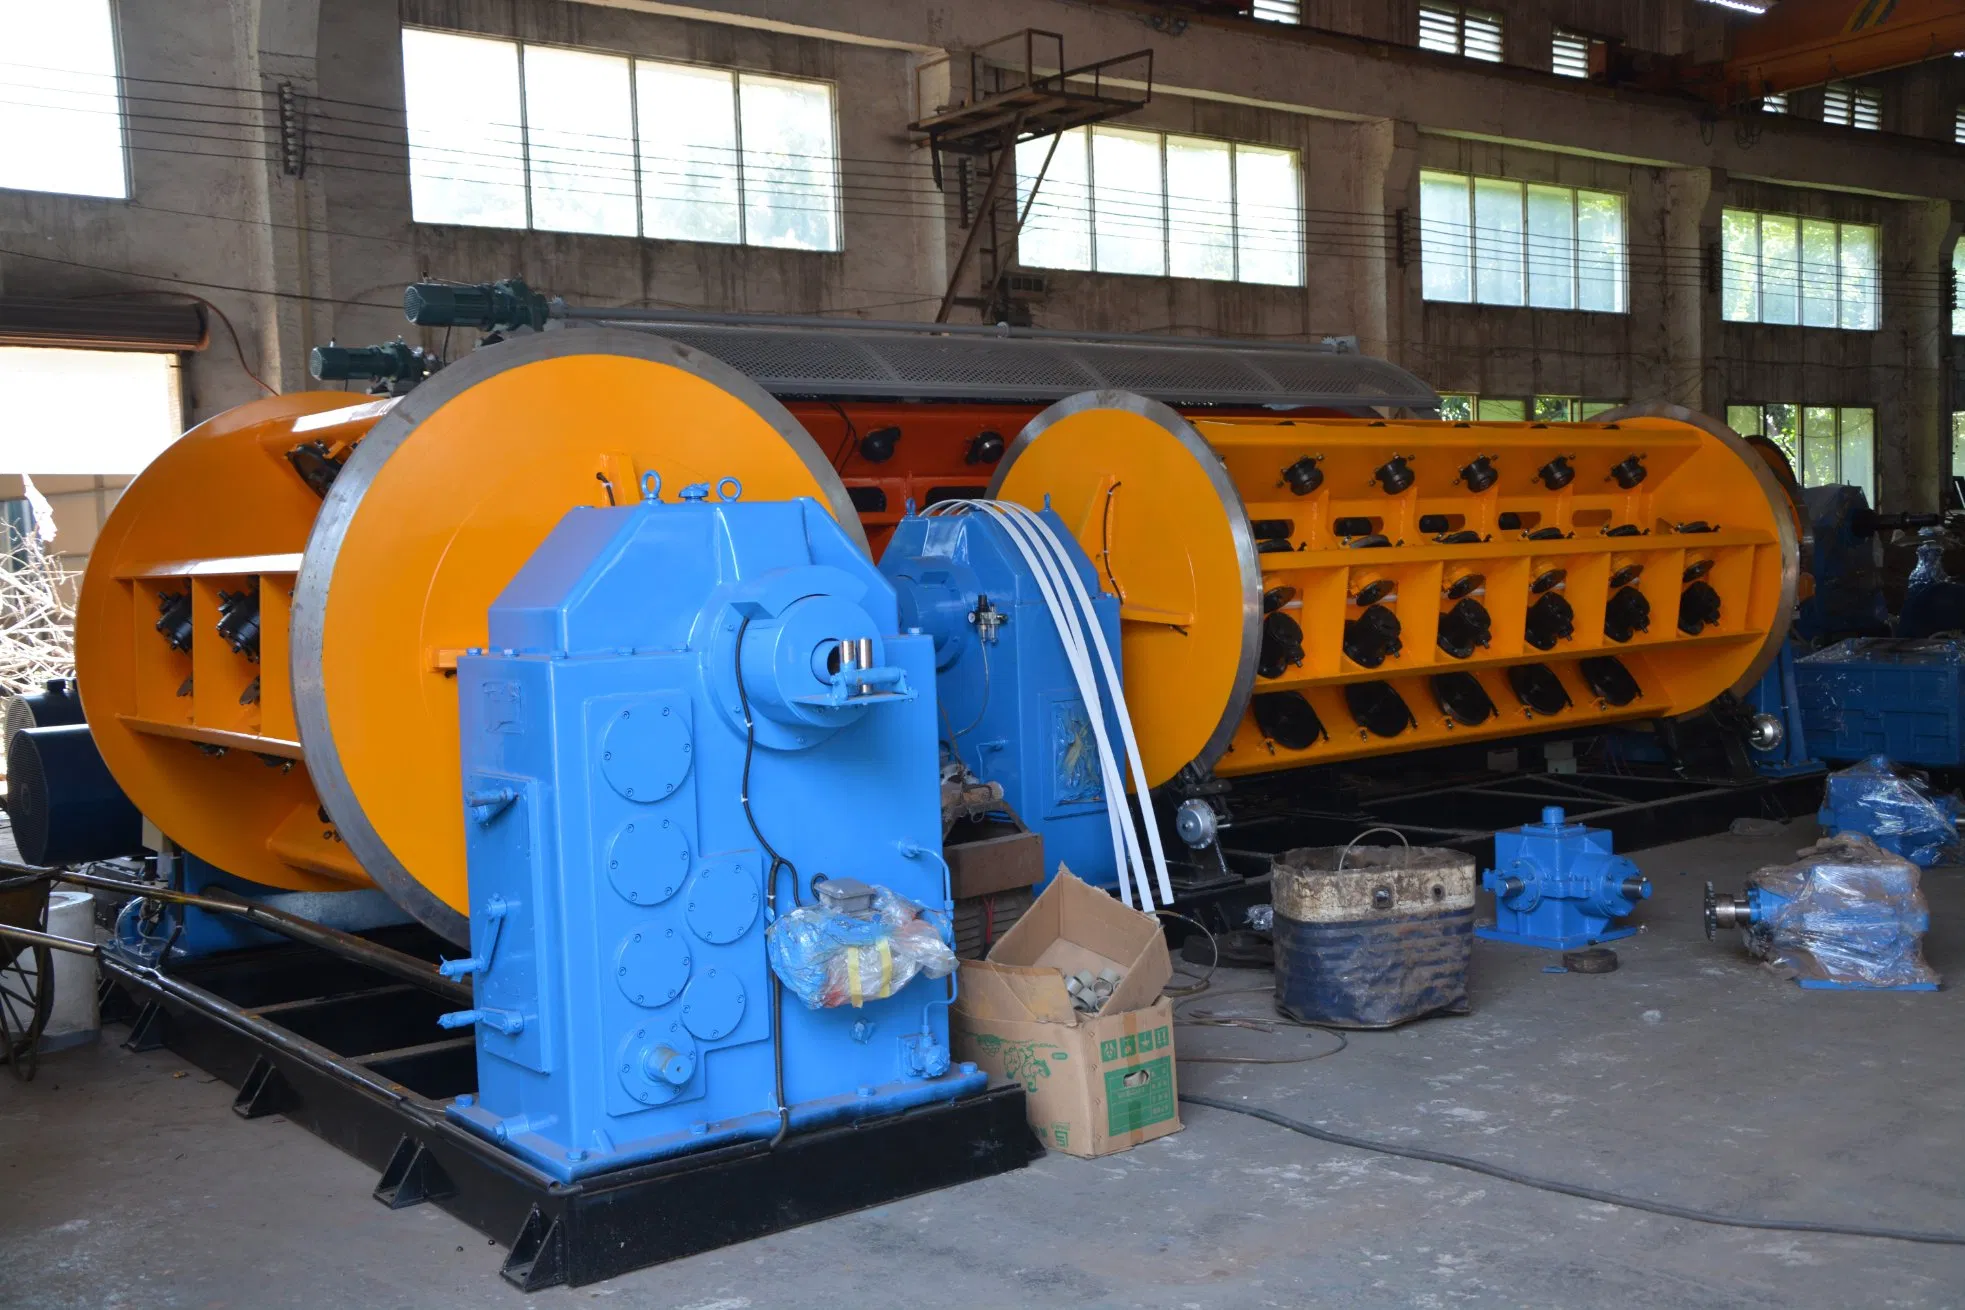
Shenzhen Sam Electrical Technology Co., Ltd. is located in Nanshan District, Shenzhen (a top GDP region in China), with production facilities in Dongguan and Jiangsu. Our core competitiveness lies in one-stop turnkey services for the wire and cable industry, including plant construction, raw material supply, equipment layout, testing laboratory construction and cable packaging. We have long been committed to helping customers obtain high-quality products at competitive prices. A key strength is our comprehensive, high-quality product and solution system. We provide reliable core production equipment (upward continuous casting machines, wire drawing machines, annealing machines, extrusion machines, stranding machines, bunching machines, etc. ) and customized supporting solutions to ensure seamless integration of equipment and processes, maximizing production efficiency and product quality. For example, we customized a solution for a Southeast Asian railway cable client to meet extreme climate and strict technical requirements, optimizing insulation processes with professional equipment. This helped the client supply qualified cables for a Belt and Road light rail project, achieving a 99.8% product qualification rate. Since establishment, we have adhered to the philosophy of "Providing customers with satisfactory equipment and first-class services". With a professional technical team and rich industry experience, we have served clients in hundreds of regions worldwide (Middle East, South Africa, Europe, Southeast Asia, etc. ), establishing long-term strategic partnerships. For instance, we provide continuous technical support and maintenance for a North African eco-friendly cable enterprise, helping it reduce production costs by 15% and improve efficiency by 20% through process optimization and intelligent monitoring. Unlike ordinary equipment suppliers, our integrated services (from project planning to after-sales support) enable us to quickly address customer needs, solve production pain points, and create higher added value. A notable case: For an African client troubled by high raw material costs and outdated processes, we provided a full set of equipment, a centralized procurement system and production management experience, cutting raw material costs by 8% and realizing digital transformation of production lines, laying a solid foundation for its market expansion and grid upgrading projects.
Company video
R&D Capacity
- R&D Engineers
- 1 people
- Customization Options
- Customization from Designs, Full Customization, Minor Customization, Flexible customization
- ODM Service Available
- Yes
- New Products Launched in Last Year
- Yes
Trade Capacity
- Export Year
- 4 years
- Main Markets
- Europe
- Nearest Port
- shenzhen port
- Terms of Payment
- LC, T/T, D/P, PayPal, Western Union, Small-amount payment
- Average Lead Time
- Peak Season Lead Time: one month Off Season Lead Time: one month
- Overseas Agent/Branch
- No
- Supply Chain Partners
- 15
- Minimum Order Quantity
- 1 set
- Number of Foreign Trading Staff
- 3
- International Commercial Terms(Incoterms)
- FOB, CIF, CFR, EXW
General Information
- Address
- B303 Building 2, Phase 1, Software Park, Nanshan District, Shenzhen, Guangdong, China
- Plant Area
- 98 square meters
- Main Products
- wire and cable plant construction, cable raw material supply, cable equipment layout, cable testing laboratory construction, and wire and cable packaging
- Registered Capital
- 1,000,000 RMB
- Repeat Buyers Choice
- < 10%
- Year of Establishment
- 2022-08-11