Company introduction
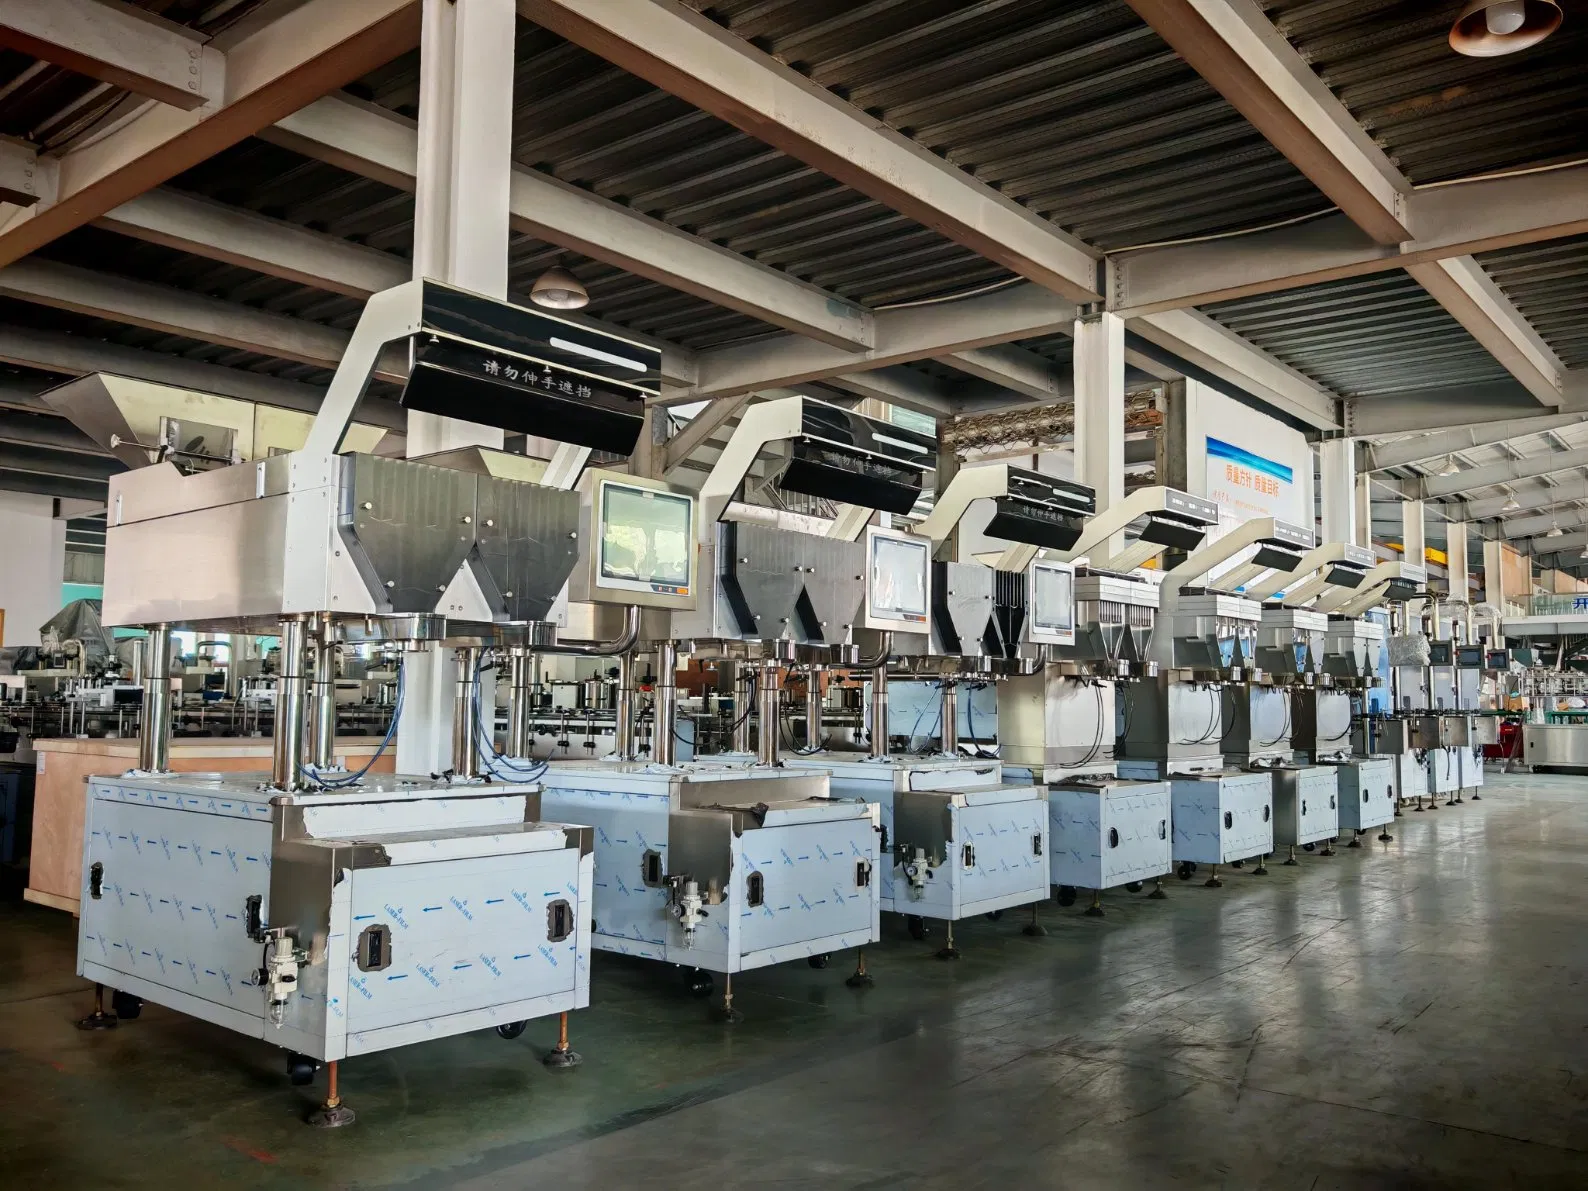
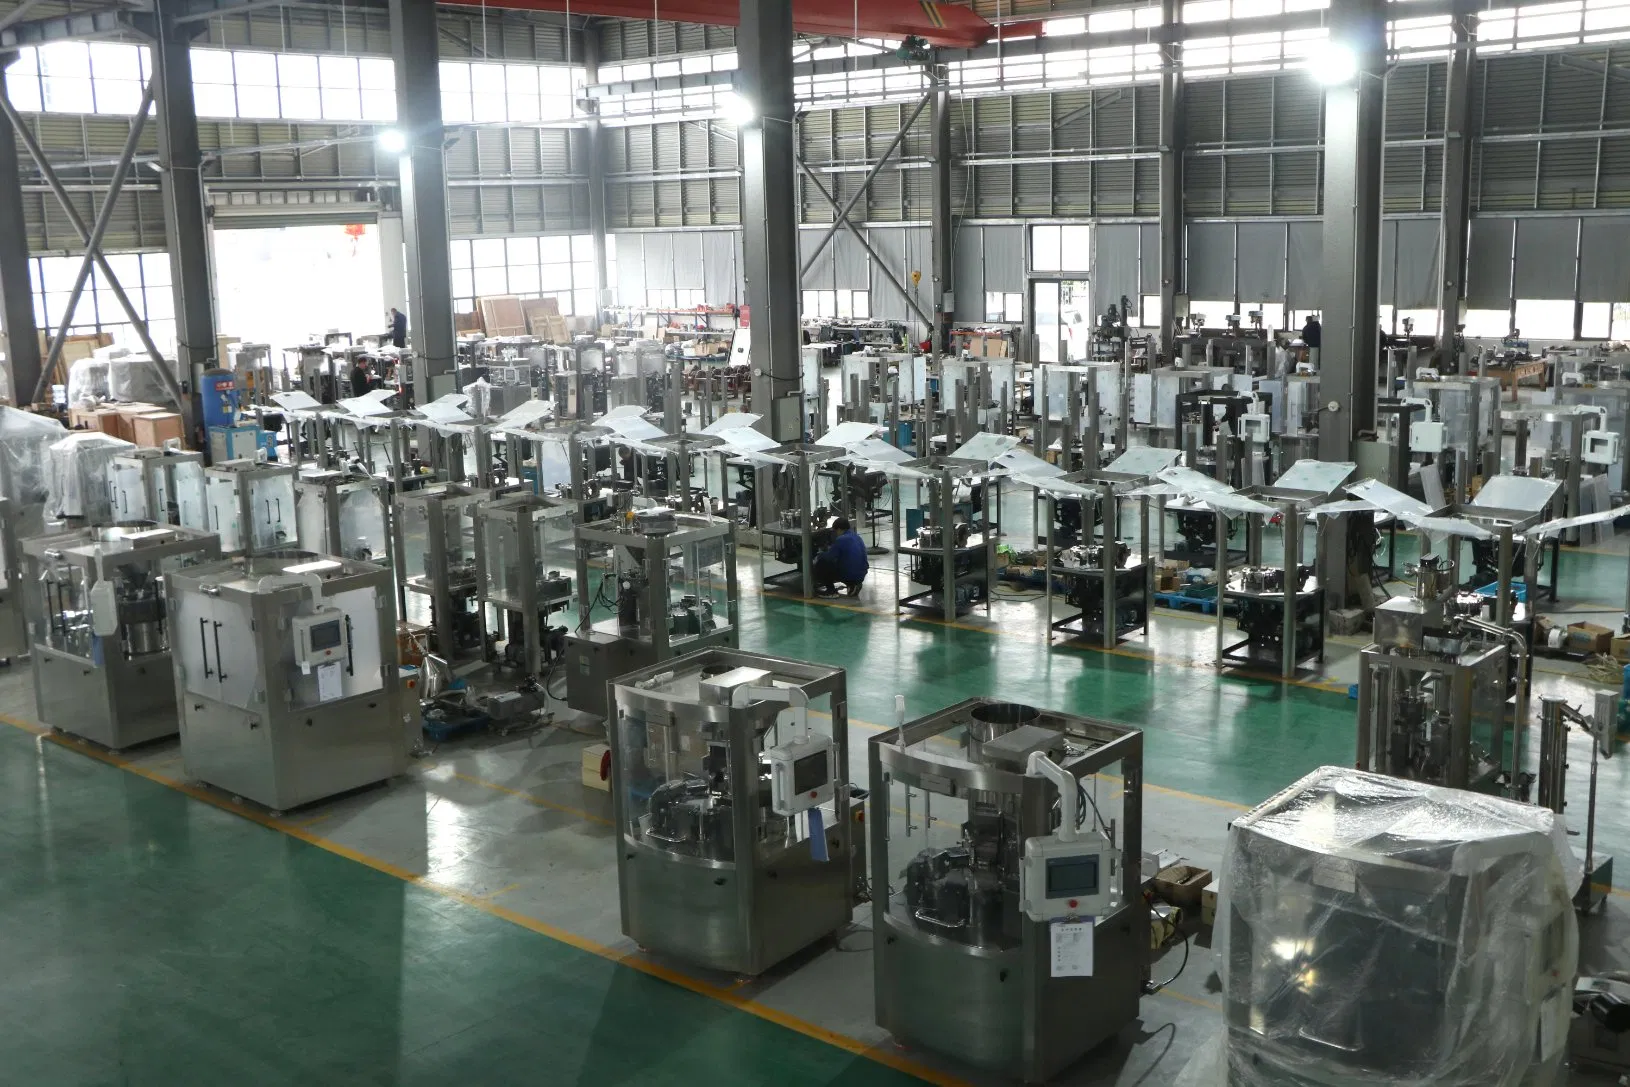
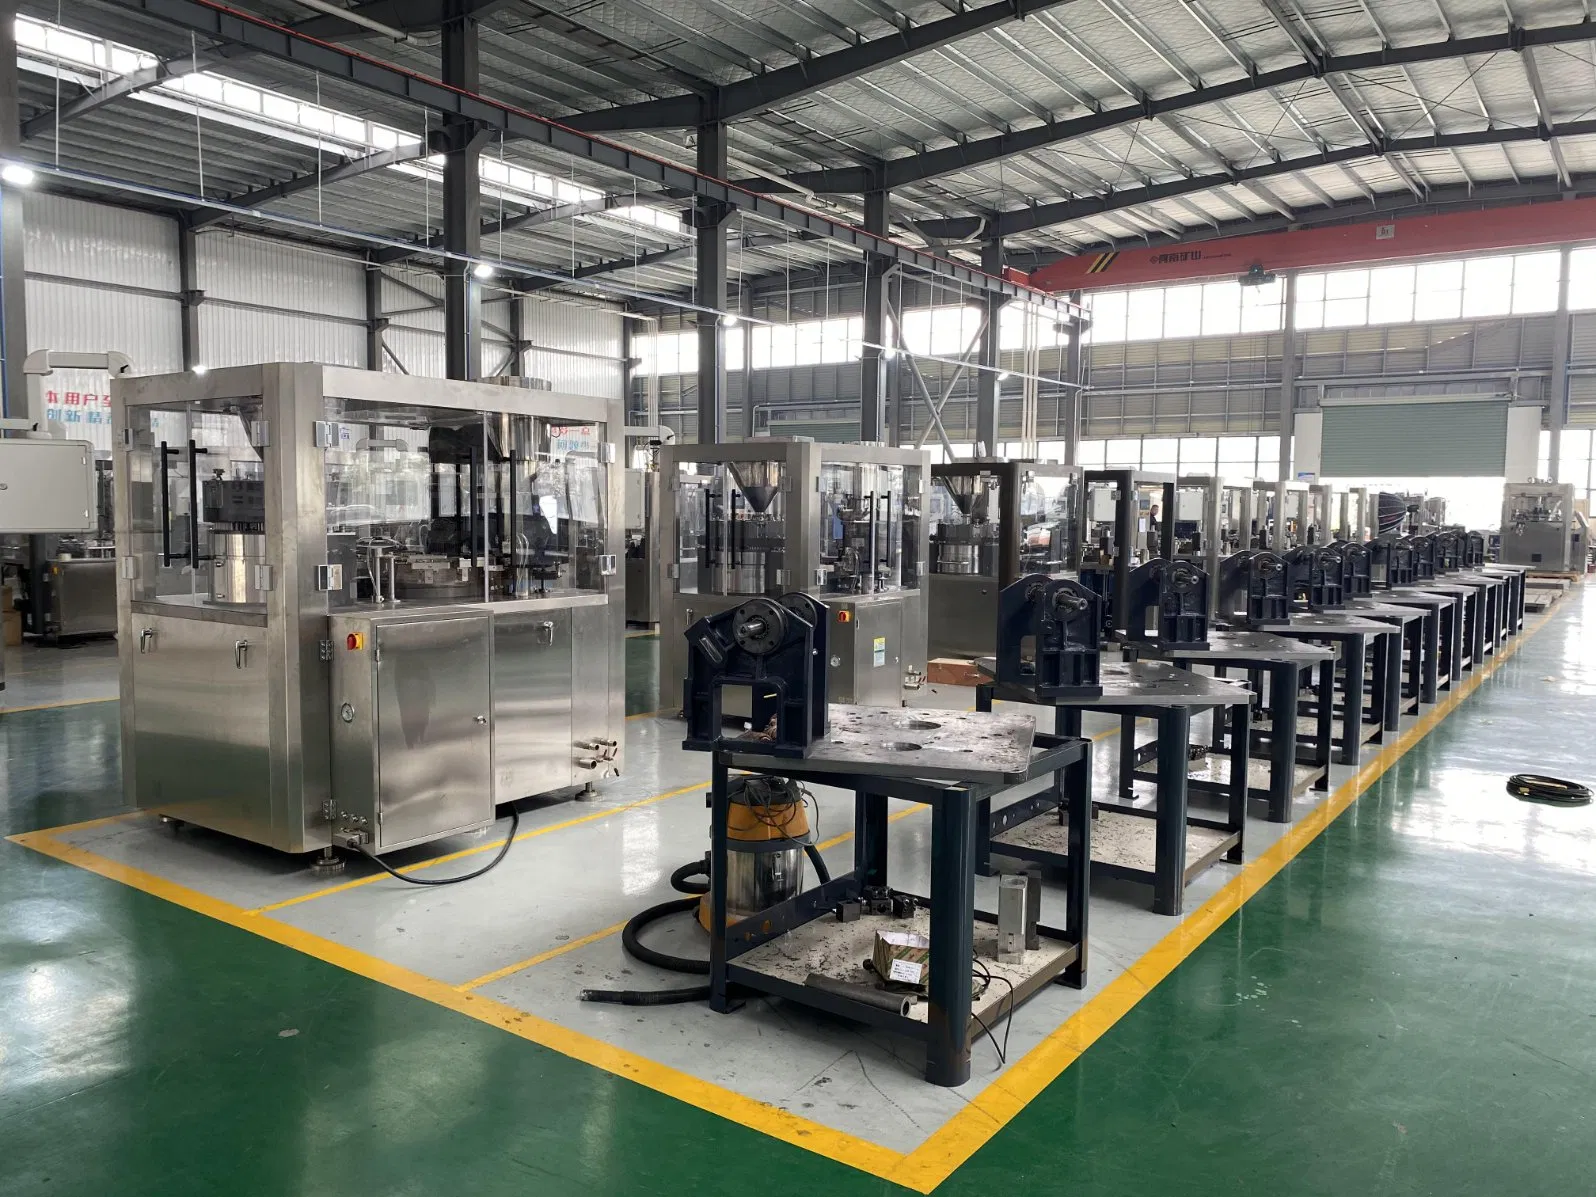
Company Overview: Hunan Innov Equipment Co., Ltd. Founded in 2014, Hunan Innov Equipment Co., Ltd. is a premier manufacturer and solution provider for the pharmaceutical and packaging machinery sectors. We serve the pharmaceutical, nutraceutical, and healthcare industries globally. By bridging cutting-edge technology with practical applications, we help businesses optimize efficiency and scale confidently. Our adherence to industry standards ensures every machine meets stringent international quality benchmarks. Our Core Product Portfolio Our robust equipment portfolio streamlines every manufacturing phase, categorized into two primary divisions: 1. Advanced Pharmaceutical Processing Machinery Engineered for precision and hygiene, our machinery ensures active ingredient integrity from raw material to finished dosage form. Granulators & Dryers: Wet and dry granulation systems, and fluid bed dryers, designed to achieve optimal moisture content, uniform particle size, and superior flowability. Capsule Filling Machines: Semi to fully automatic models deliver precise dosing for powders and pellets, minimizing material waste and maximizing output. Tablet Presses: High-speed rotary presses with intelligent pressure control and automated rejection, guaranteeing consistent tablet weight, hardness, and flawless appearance. Softgel Encapsulation Machines: Tailored for nutraceutical markets, providing seamless liquid encapsulation for high bioavailability and extended shelf life. 2. Intelligent Packaging Solutions Our packaging lines are built for high speed, adaptability, and uncompromising barrier protection. Blister Packing Machines: Utilizing advanced thermoforming and cold-forming technologies for superior protection against moisture, light, and oxygen. Electronic Counting Lines: Featuring advanced optical sensors for precise bottle-filling accuracy, effectively eliminating costly overfills or dangerous underfills. Cartoning Machines: Automated cartoners that integrate upstream to fold, load, and seal cartons at high speeds, accommodating complex leaflets and batch coding. Case Packers: Completing end-of-line automation with reliable collating, loading, and sealing of corrugated boxes for safe global distribution. Engineering Excellence and R&D At our core is a senior engineering team with over 15 years of industry experience. This deep expertise drives our R&D, allowing us to provide technical guidance and continuously upgrade technologies. Heavy investment in research ensures our machinery reflects modern engineering, keeping clients at the forefront of innovation. Tailored Solutions and Dedicated Sales Understanding no two facilities are identical, our sales team takes a consultative approach. We meticulously analyze your operational requirements, floor space, and budget to provide customized turnkey solutions that seamlessly fit your business needs. Unwavering After-Sales Support To ensure uninterrupted operations, our technical department offers 24-hour support, remote troubleshooting, on-site installation, and operator training. Dedicated technicians and a robust spare parts inventory guarantee stable operation and minimize downtime worldwide. Our Philosophy Adhering to "Quality First and Customer-Oriented, " we provide reliable equipment and lifecycle services. We believe your success is our success, and are dedicated to advancing global healthcare through superior machinery, building lasting partnerships based on mutual trust, excellence, and shared growth.
Company video
Trade Capacity
- Export Year
- 2014-11-01
- Main Markets
- North America, South America, Eastern Europe, Southeast Asia, Africa, Oceania, Mid East, Eastern Asia, Western Europe
- Nearest Port
- Ningbo/Shanghai
- Terms of Payment
- LC, T/T, D/P, Western Union, Small-amount payment
- Average Lead Time
- Peak Season Lead Time: one month Off Season Lead Time: within 15 workdays
- International Commercial Terms(Incoterms)
- FOB, EXW, CFR, CIF, DAT, FAS, DDP, CIP, FCA
General Information
- Address
- Oaks Colorful Plaza, No. 858 Dujuan Road, Wangyue Street, Yuelu District, Changsha, Hunan, China
- Main Products
- Capsule Filling Machine, Tablet Press Machine, Blister Packing Machine, Cartoning Machine, Bottle Counting Machine Line, Plastic Ampoule Filling Sealing Machine, Powder Mixer, Softgel Encapsulation Machine, Granulator, Tube Filling Sealing Machine