Company introduction
Company Profile Founded in 2016 and headquartered in Yantai, Shandong Province, China, Shandong Zhongsheng Pharmaceutical & Chemical Equipment Co., Ltd. is a national high-tech enterprise and a recognized "Little Giant" company under China's specialized and sophisticated SME development program. The company is also identified as a gazelle enterprise in Shandong Province, reflecting its strong innovation capability, rapid growth, and solid industry position. Zhongsheng specializes in the research, development, and manufacturing of energy-efficient and environmentally friendly equipment for the pharmaceutical and chemical industries. With a clear focus on green manufacturing and sustainable industrial development, the company provides integrated, system-level solutions that combine advanced process technologies, intelligent control systems, and high-performance equipment. Core Business Areas The company's business is structured around four primary segments: Distillation and separation systems Molecular sieve membrane dehydration systems Waste gas, wastewater, and solid waste treatment systems Integrated energy-saving process systems Among these, energy-efficient distillation systems form the core of Zhongsheng's business, accounting for approximately 89% of total revenue. Through continuous innovation and engineering expertise, the company has established a strong competitive advantage in this field. Distillation is a fundamental unit operation in pharmaceutical and chemical production, but it is also one of the most energy-intensive processes. Zhongsheng addresses this challenge by developing advanced distillation solutions that significantly reduce energy consumption while maintaining high separation efficiency and operational stability. Flagship Technology and Product Advantages Zhongsheng's flagship product, the "Ultra Energy-Efficient Self-Heat-Recovery Distillation System, " represents a key technological breakthrough in separation engineering. The system is based on heat cascade utilization and system-level optimization. By efficiently recovering and reusing latent heat generated during the distillation process, it minimizes external energy input and maximizes thermal efficiency. Compared with conventional distillation systems, Zhongsheng's solution offers: More than 20% improvement in energy efficiency 30% to 50% reduction in overall energy consumption Significant reduction in carbon emissions Enhanced process stability and controllability The technology is particularly suitable for complex separation scenarios, including azeotropic systems, heat-sensitive materials, and multi-component mixtures commonly found in pharmaceutical and fine chemical production. Integrated Process Innovation A key strength of Zhongsheng lies in its ability to integrate multiple advanced technologies into a unified process solution. The company has developed a proprietary process route that combines: Self-heat recovery distillation Membrane separation technology Heat pump integration This integrated approach enables comprehensive optimization of separation processes, improving energy efficiency, product quality, and overall system performance. Rather than providing standalone equipment, Zhongsheng delivers turnkey solutions that cover the entire project lifecycle, including process design, equipment manufacturing, system integration, intelligent control, and ongoing optimization. This system-oriented capability allows the company to better meet the complex and evolving needs of its customers.
Company video
R&D Capacity
- Own Brand
- Yes
- R&D Engineers
- 34 people
- Production Machines
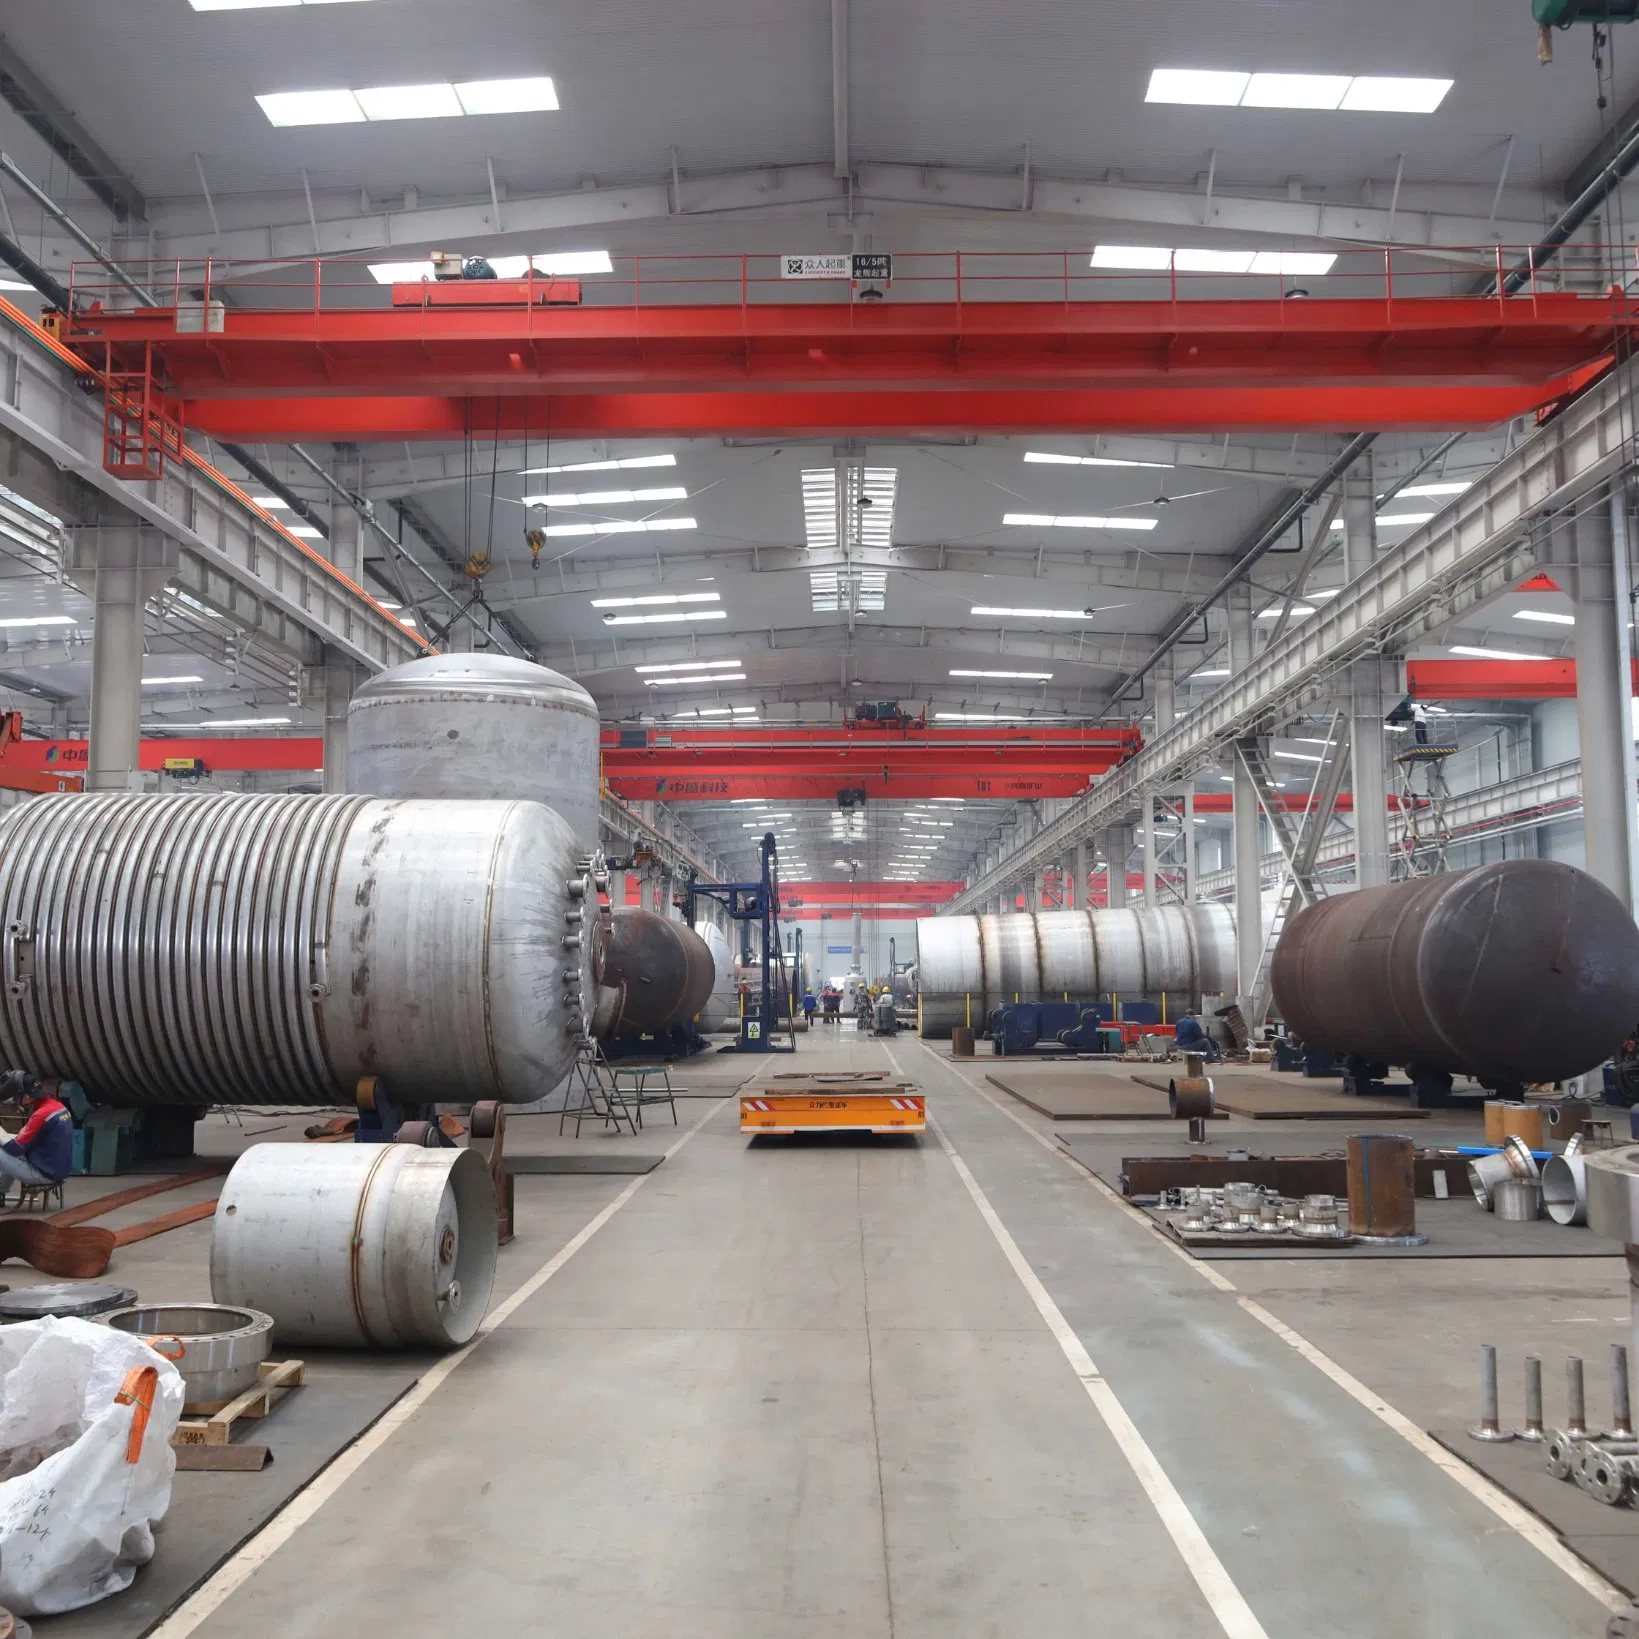
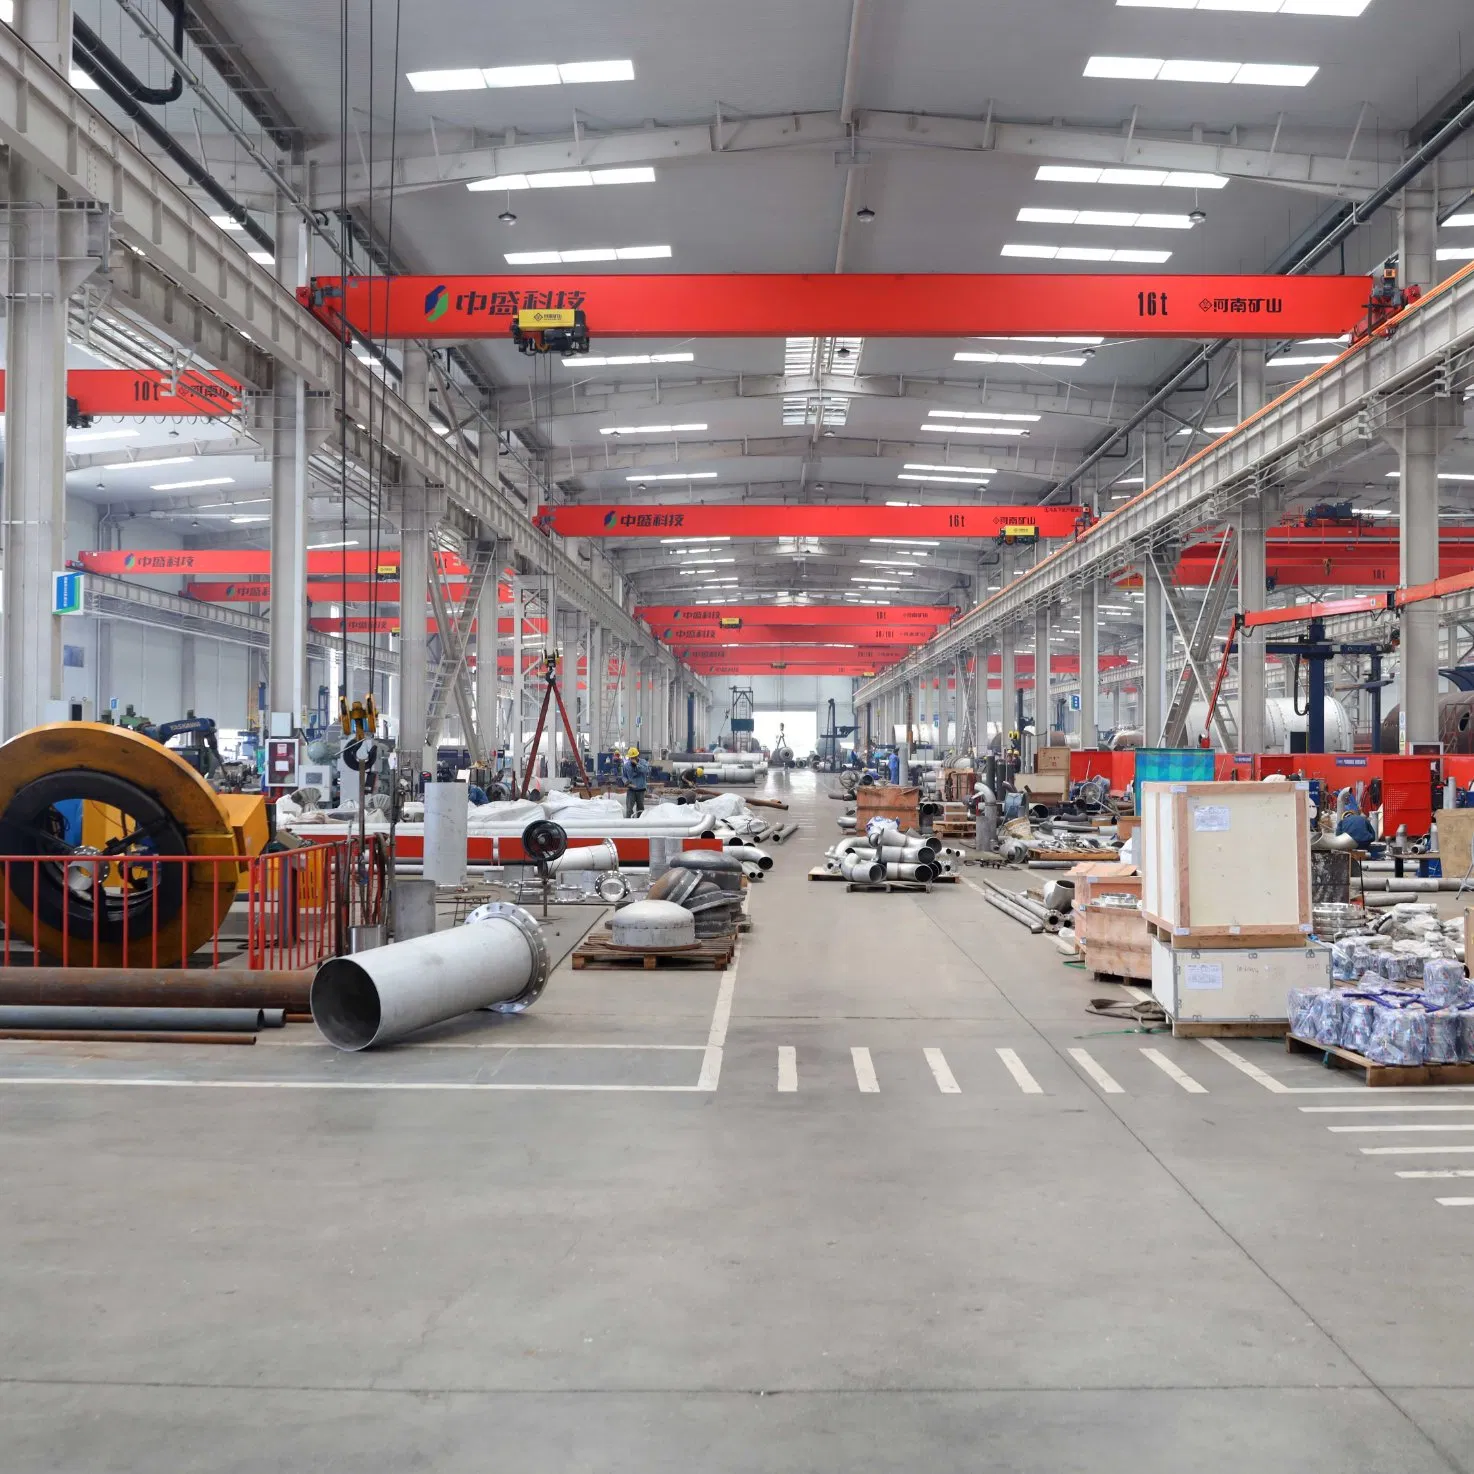
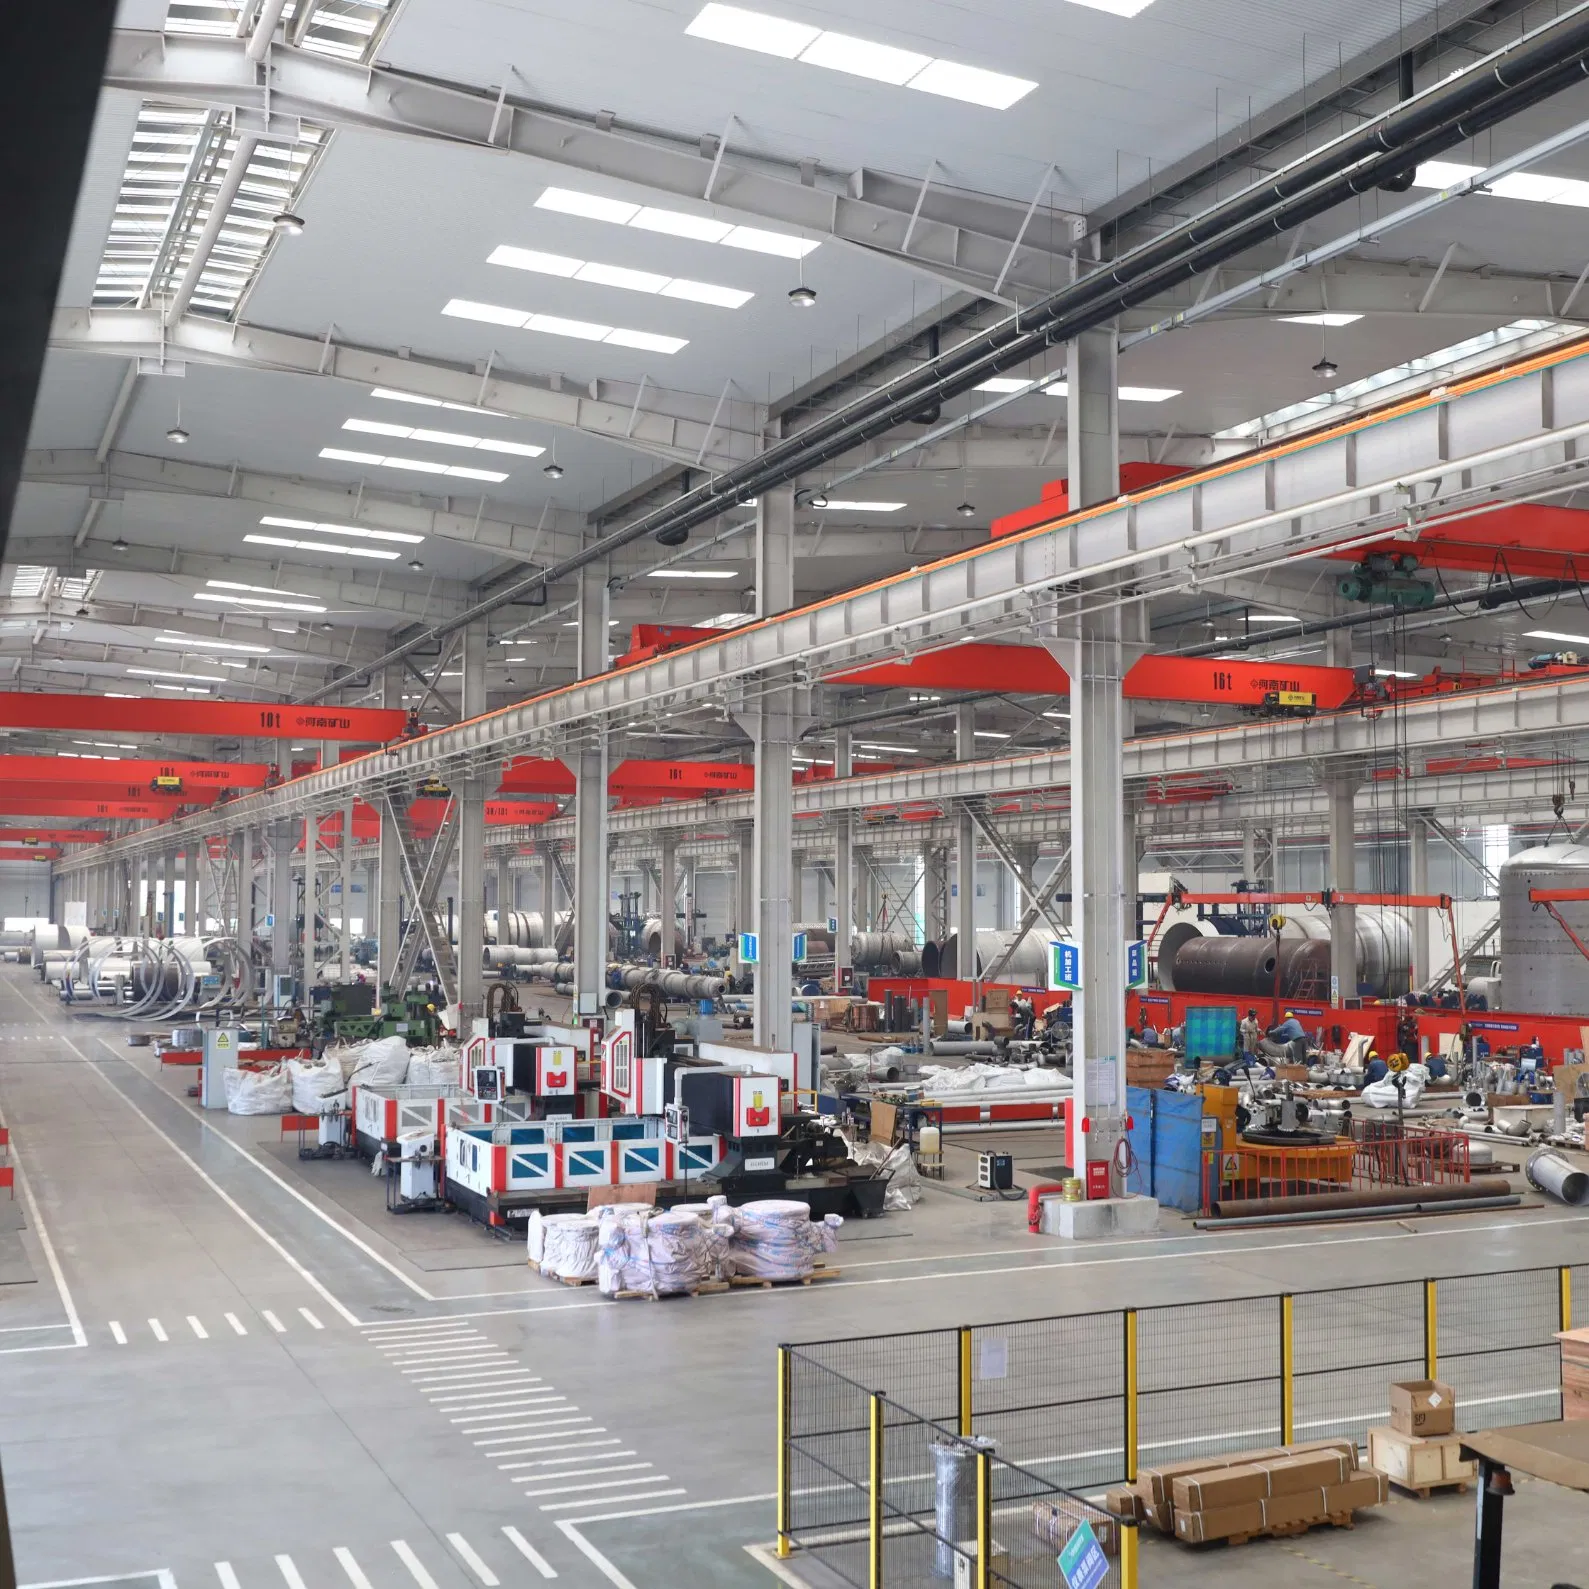
- Cutting Machine, Bending Machine, CNC Machining Center, Drilling Machine, Lathe, Rolling Machine, Welding Machine, Welding Robot, Cutting Machine, Cutting Machine, Punching Machine, Laser Cutting Machine, Plasma Cutting Machine
- Customization Options
- Flexible customization, Minor Customization, Full Customization, Customization from Designs, Customization from Samples
- ODM Service Available
- Yes
- New Products Launched in Last Year
- Yes
Trade Capacity
- Export Year
- 1 year
- Main Markets
- Domestic
- Nearest Port
- Qingdao Port
- Terms of Payment
- T/T
- Average Lead Time
- Peak Season Lead Time: 1-3 months Off Season Lead Time: 1-3 months
- Overseas Agent/Branch
- No
- Supply Chain Partners
- 24
- Minimum Order Quantity
- 1 Set
- Number of Foreign Trading Staff
- 6
- International Commercial Terms(Incoterms)
- FOB, EXW
General Information
- Address
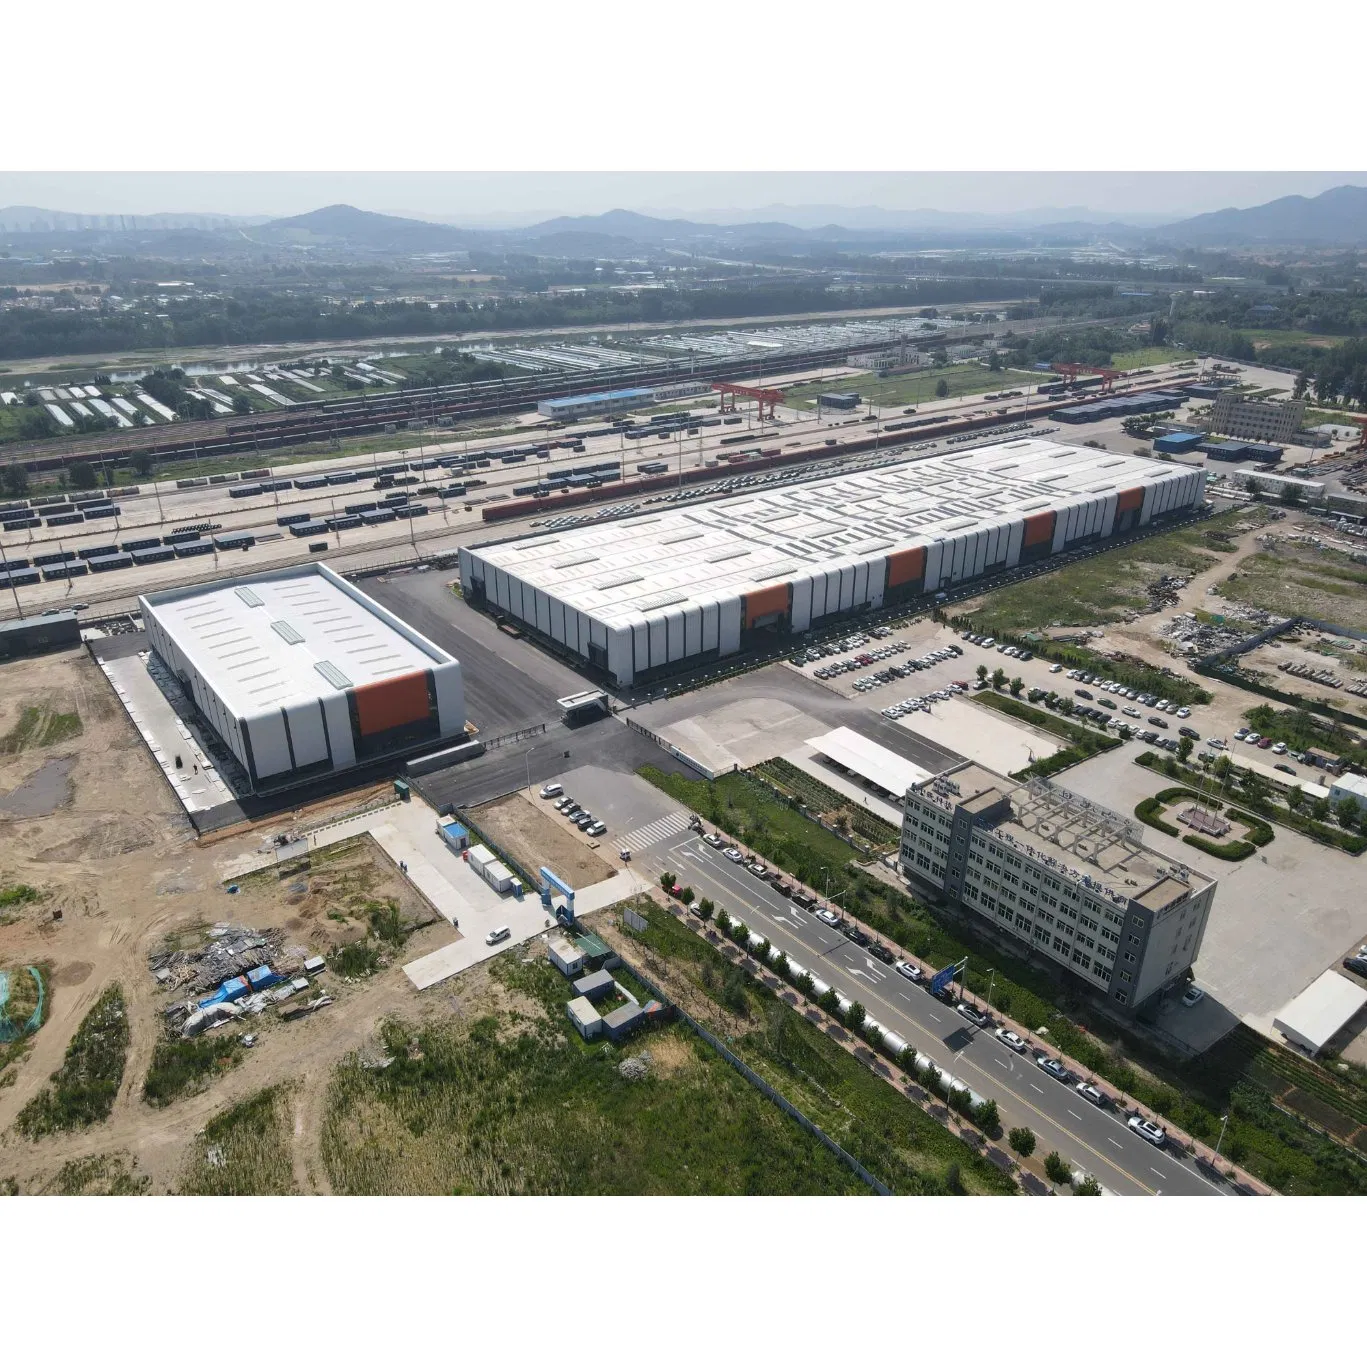
- Yu'an Rd. No. 2, Menlou Subdistrict, Fushan Dist., Yantai City, Shandong Province, Yantai, Shandong, China
- Plant Area
- 27946 square meters
- Business Type
- Manufacturer/Factory & Trading Company
- Main Products
- Distillation Technology and Equipment, Environmental Technology and Equipment, Energy Technologies and Equipment
- Registered Capital
- 25,734,000 RMB
- Number of Employees
- 191
- Repeat Buyers Choice
- 10%~30%
- Year of Establishment
- 2016-12-23
- Cooperated with Fortune 500
- No
- Management System Certification
- ISO9001:2015, ISO45001:2018, ISO14001
Production Capacity
- Production Lines
- 4
- QA/QC Inspectors
- 10 people
- Traceability of Raw Materials
- Yes
- Inspection Type for Finished Products
- 100% inspection(Visual inspection & Function inspection)
- Inspection Method for Finished Products
- Have instructions and uniformly followed