Loading…
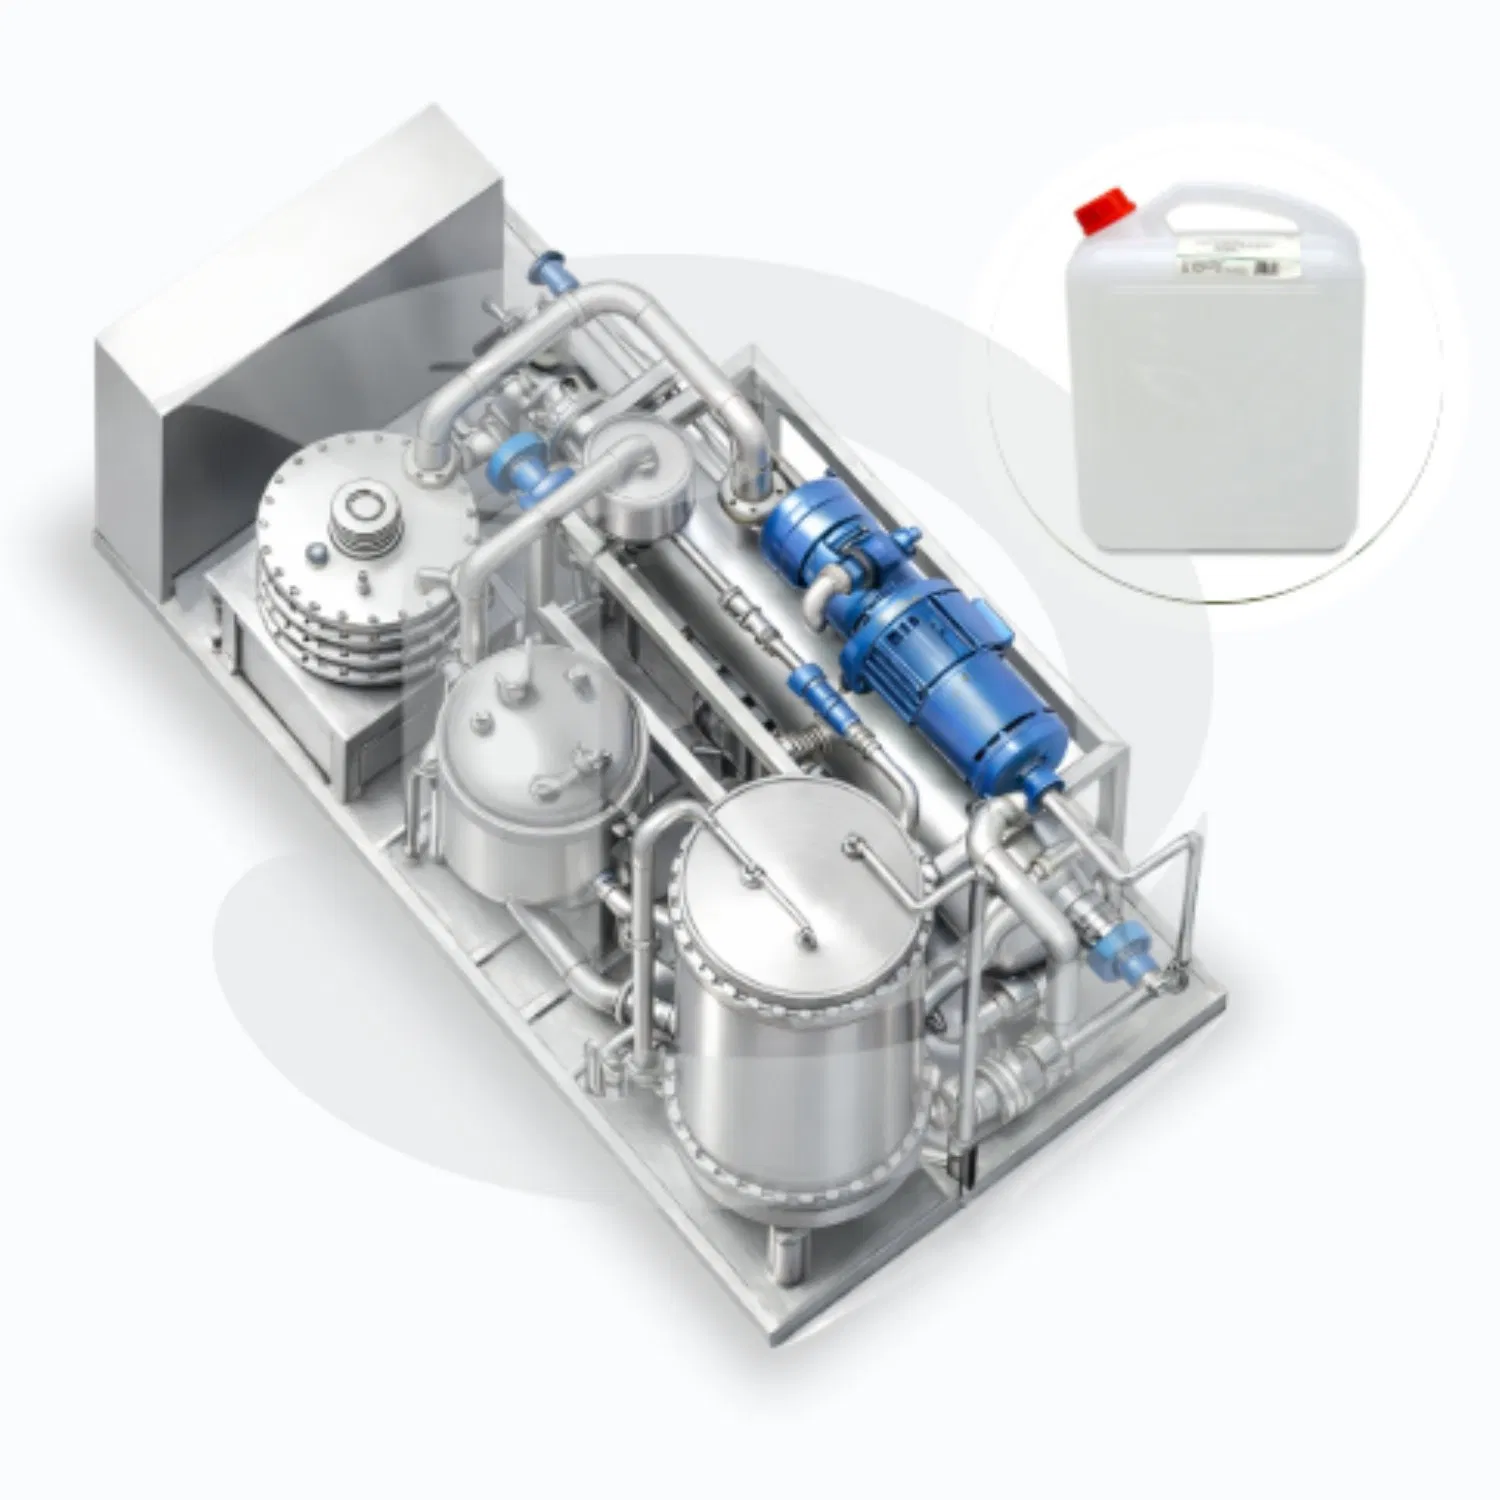
Pressure-Durable High-Gravity Heat Pump Ethanol Separation Solvent Recovery Molecular Distillation Refinery System
5.0InStock Source-listed auditby Jiangsu Super Distillation Technology Co., Ltd.
₹1,08,55,000≈ $130,000 · indicative, confirm with supplier
Description
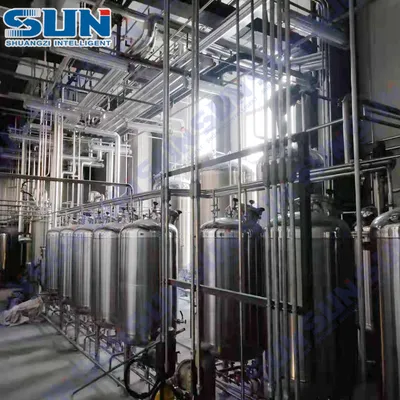
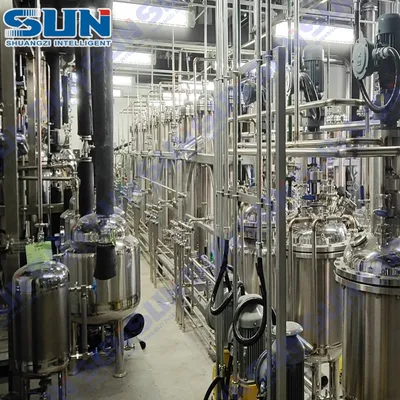
Pressure-Durable High-Gravity Heat Pump Ethanol Separation Solvent Recovery Molecular Distillation Refinery System. Supergravity Separation: Centrifugal field hundreds to thousands times stronger than normal gravity for enhanced mass transfer. Heat Pump Energy Recovery: Bidirectional heat and cold utilization via reverse Carnot cycle for highly efficient energy recovery. Compact Footprint: System footprint is typically one tenth of a conventional distillation column. Electric Operation: Runs on electricity only, eliminating need for steam or cooling water utilities. Low Fouling Design: Enhanced turbulence reduces fouling tendency with automatic CIP for online cleaning. Heat-Sensitive Material Friendly: Low liquid holdup and short residence time reduce thermal stress on sensitive materials. 1-Year Warranty: Comprehensive 1-year warranty coverage for the equipment. Skid-Mounted Delivery: Delivered as skid-mounted modules for easy installation in space-limited areas.
Specifications
TypeDistillation Equipment
Warranty1year
Model NO.VHPS
CustomizationAvailable
After-sales Service1year