Loading…
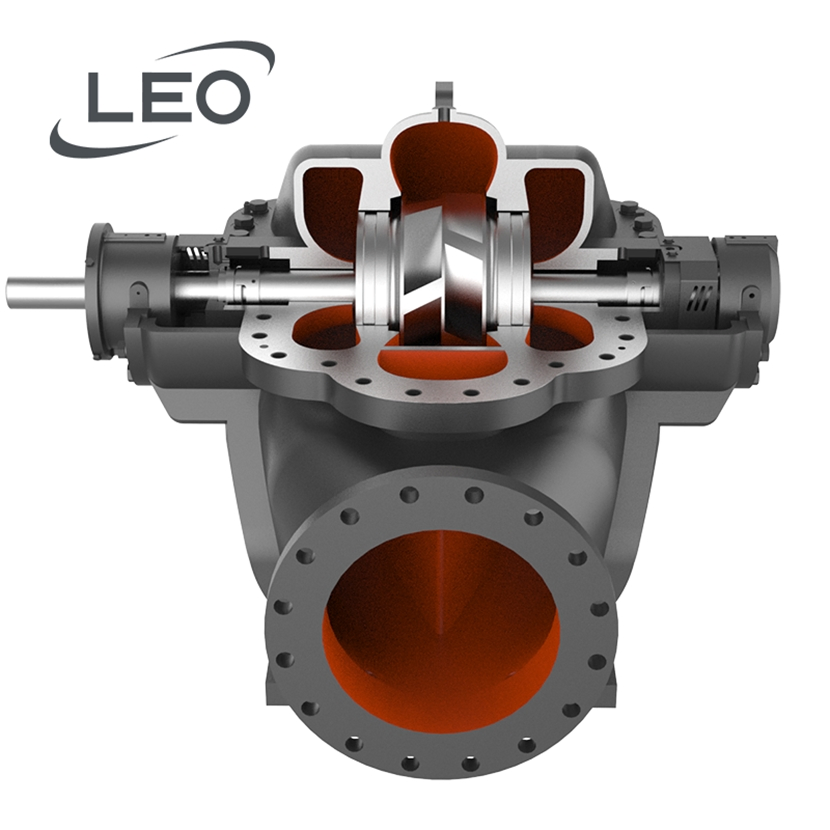
Industrial Single Stage Double Suction Centrifugal Water Pump Circulating Pump
5.0InStock Source-listed auditby LEO GROUP PUMP (HUNAN) CO., LTD.
₹2,50,500≈ $3,000 · indicative, confirm with supplier
Payment
Description
Industrial Single Stage Double Suction Centrifugal Water Pump Circulating Pump. High Efficiency Design: Meets GB/T19762 energy efficiency standards with optimized hydraulic performance and low NPSH. Robust Construction: Features horizontal split casing, double-suction impeller, and stainless steel shaft sleeve for durability. Superior Sealing System: Equipped with mechanical seals or non-asbestos packing options for leak-free long-term operation. Stable Bearing Performance: Short span enlarged diameter design with grease lubrication and optional vibration monitoring. Customizable Options: Accepts OEM/ODM services with customizable direction of rotation and shaft seal types. Wide Application Range: Suitable for water supply, drainage, and cooling systems in steel, petrochemical, and mining industries. Comprehensive Warranty: Includes a one-year warranty covering mechanical defects and quality assurance. Flexible Motor Configuration: Supports 3-phase motors with IP55 protection and F insulation class for various power needs.
Specifications
Max.Head50-80m
WarrantyOne Year
Model NO.GSX250-480
Max.Capacity>400 L/min
CustomizationAvailable