Loading…
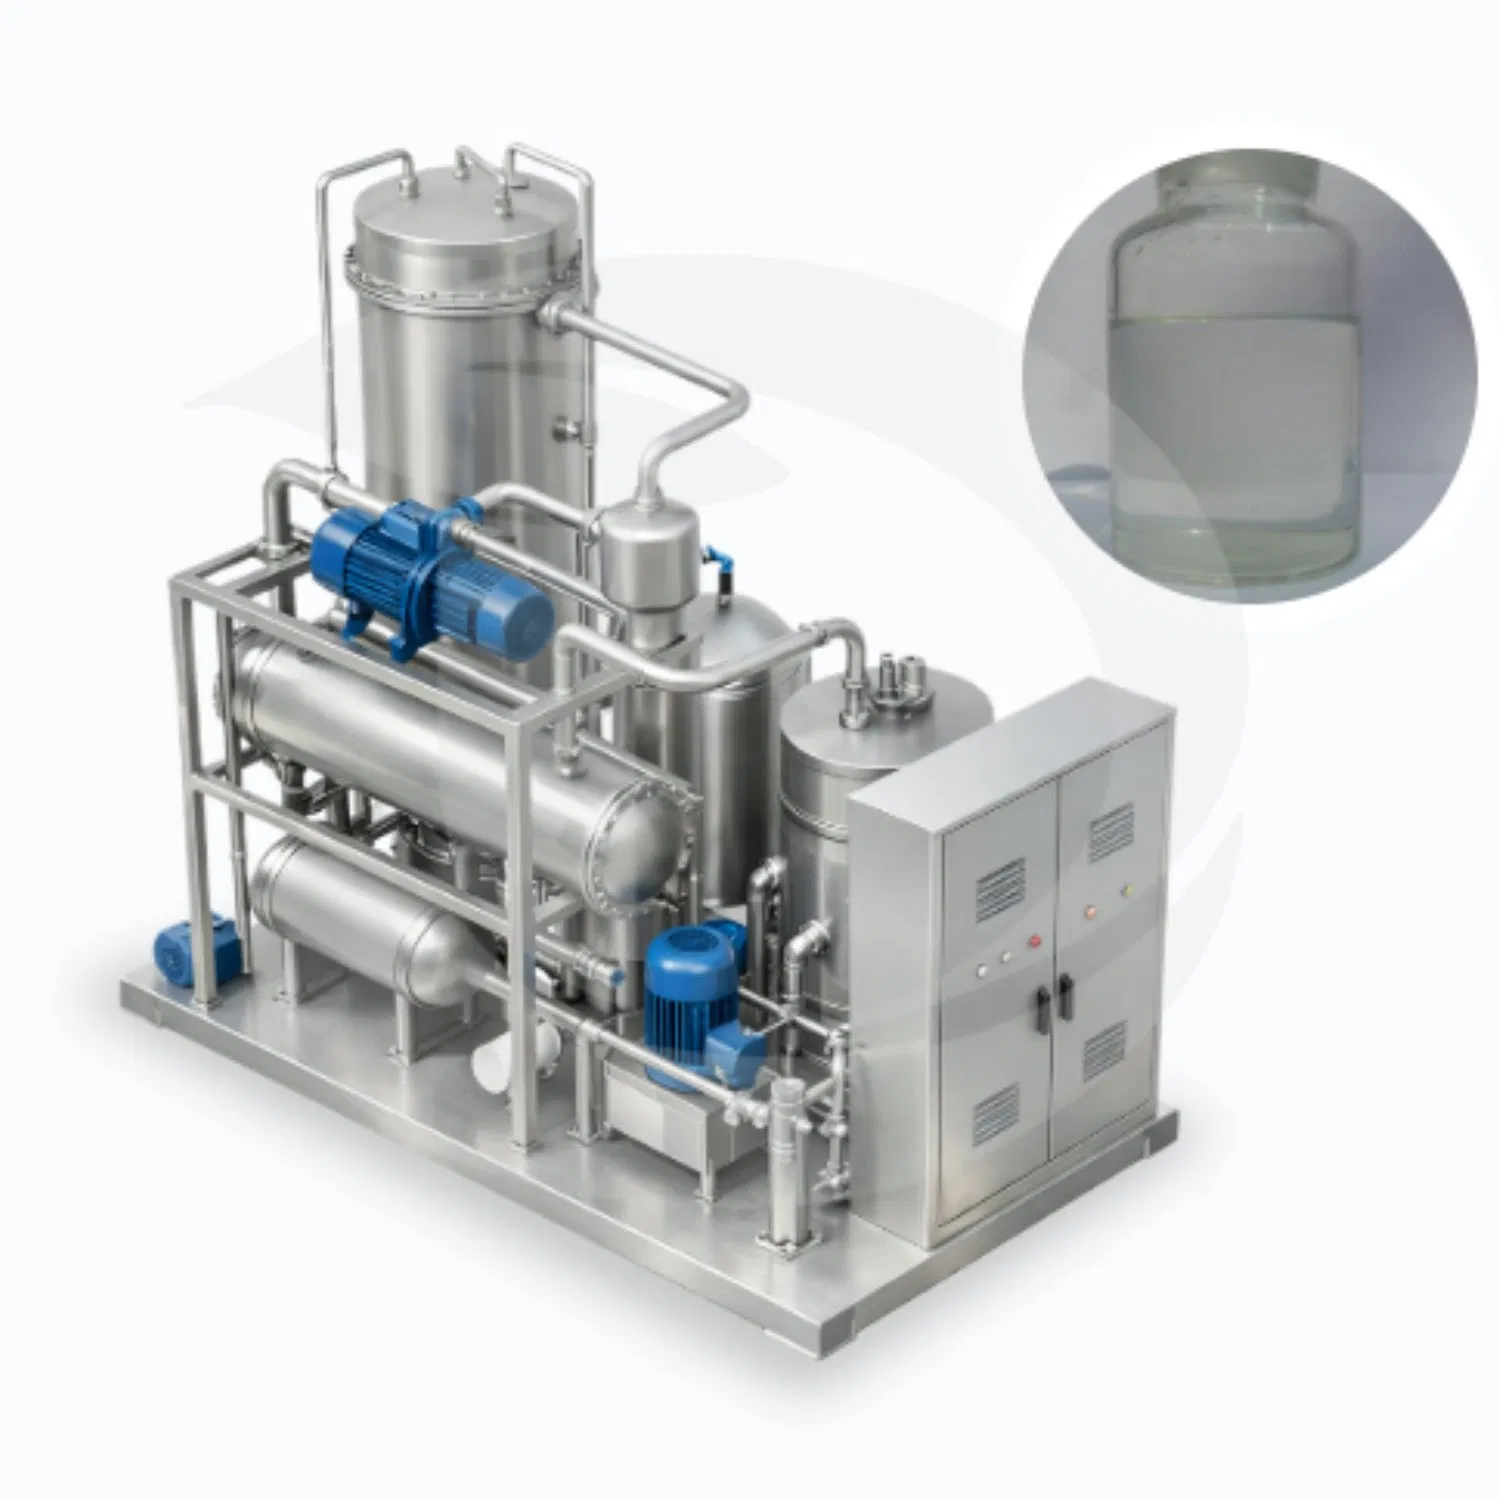
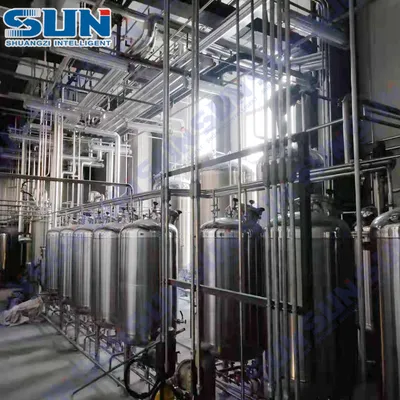
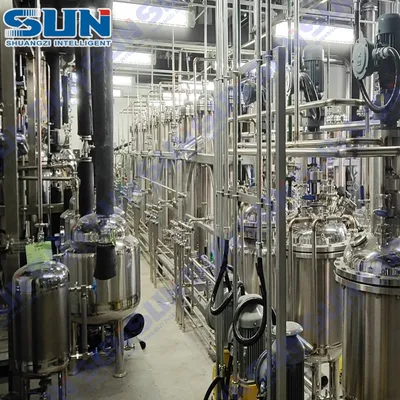
Thermo-Stable High-Gravity Heat Pump Ethanol Solvent Recovery System Molecular Distillation Refinery Skid-Mounted Unit
5.0InStock Source-listed auditby Jiangsu Super Distillation Technology Co., Ltd.
₹1,08,55,000≈ $130,000 · indicative, confirm with supplier
Description
Thermo-Stable High-Gravity Heat Pump Ethanol Solvent Recovery System Molecular Distillation Refinery Skid-Mounted Unit. Supergravity Separation: Centrifugal field 1000x gravity, 20x interfacial area, 1000x mass transfer rate. Heat Pump Energy Recovery: Closed-loop cycle with bidirectional heat/cold utilization for high efficiency. Compact Footprint: Size is 1/10th of traditional columns, ideal for space-limited skid-mounted units. Electric Operation: Runs solely on electricity, eliminating need for steam or cooling water. Low Fouling Design: Enhanced turbulence reduces fouling; includes automatic CIP for online cleaning. Heat-Sensitive Material Safe: Low holdup and short residence time minimize thermal stress on sensitive products. 1-Year Warranty: Comprehensive 1-year warranty coverage for mechanical defects and parts. Comprehensive After-Sales: Includes installation guidance, commissioning, training, and lifetime technical support.
Specifications
TypeDistillation Equipment
Warranty1year
Model NO.VHPS
CustomizationAvailable
After-sales Service1year