Loading…
Monoethanolamine for Surfactant Manufacturing Mea
InStock Source-listed auditby Shandong on The Way New Material Technology Co., Ltd.
₹66,800≈ $800 · indicative, confirm with supplier
Supplier information
Audited supplier
Description
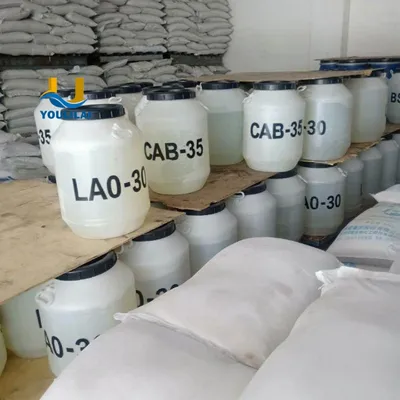
Monoethanolamine for Surfactant Manufacturing Mea. High Purity Grade: 99.9% content with strict quality control for reagent and industrial use. Versatile Applications: Used in gas treatment, personal care, agrochemicals, and textile industries. Flexible Customization: Offers full, minor, and sample-based customization options for clients. Stable Physical Properties: Clear, colorless to pale yellow liquid with specific density and boiling point. Secure Packaging: Available in 250kg IBC containers, 25kg jerrycans, or bulk tanker trucks. Long Shelf Life: Maintains quality for 24 months when stored in cool, dry, and ventilated areas. Comprehensive Documentation: Provides commercial invoice, packing list, COA, and certificates upon request. Competitive Pricing: Integrated industry and trade model ensures high quality and competitive prices.
Specifications
Water0.023
Content99.9%
AppearanceLiquid
Grade StandardReagent Grade, Medicine Grade, Electron Grade, Industrial Grade, Agriculture Grade
Distillatevolume98