Loading…
Coating Spray Process Thermal Spray on Railway Pin, Locomotive Pin, Rolling Stock Pin
4.0InStockby Xiangtan Shicheng Trading Co., Ltd.
₹37,575≈ $450 · indicative, confirm with supplier
Supplier information

Description
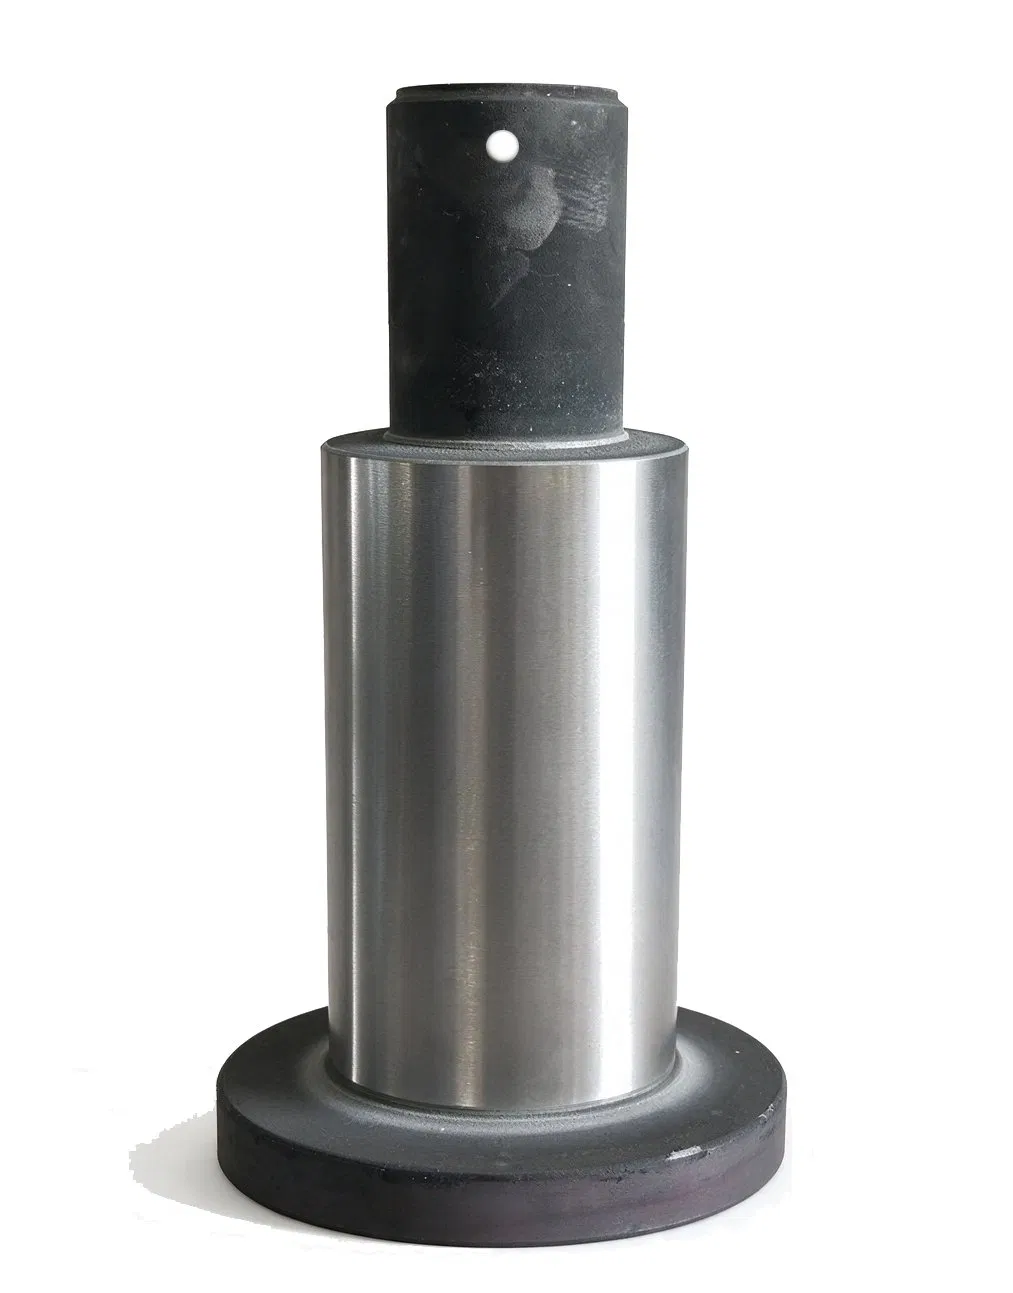
Coating Spray Process Thermal Spray on Railway Pin, Locomotive Pin, Rolling Stock Pin. Heat treatment: Quench and temper overall, plus surface hardening (induction hardening or carburizing). The core stays tough and the surface stays hard. Working surface precision: Cylindrical ground, surface roughness Ra 0.4 to 1.6 microns, roundness 0.02 to 0.05 mm, fitted with the pin bore at H8/f7. Mechanical requirements: High impact resistance, bending fatigue strength, abrasive wear resistance, and fretting wear resistance. Geometry: Flanged or headed end for axial location; radial cross-hole at the opposite end for a cotter pin, exactly the small hole visible on top of the pin .
Specifications
Model NO.ODM/OEM/Incoming process/custom
Power SourceFuel Gas
Service ModesOEM/ODM Customized Per Drawing or Sample
Coating MaterialTungsten Carbide ,Chromium-Based
Application FieldAutomotive, Railways