Loading…

Reverse Osmosis RO Machine for Commercial Use 0.25-0.5 Ton/Hr
5.0InStock Source-listed auditby Ningbo Eonjoy International Trade Co., Ltd.
₹80,160≈ $960 · indicative, confirm with supplier
Payment
LC, T/T, D/P, PayPal, Western Union, Small-amount payment
Incoterms
FOB, CIF, CFR, EXW
Description
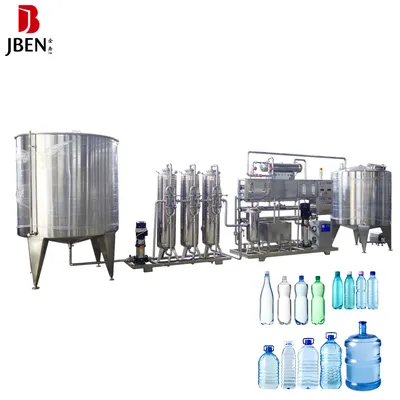
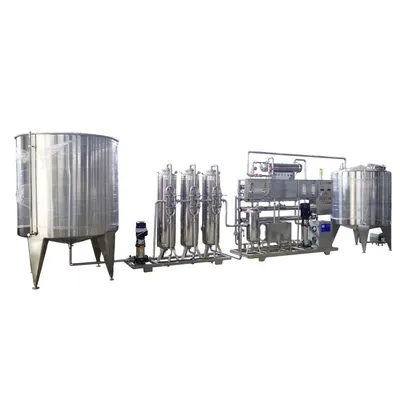
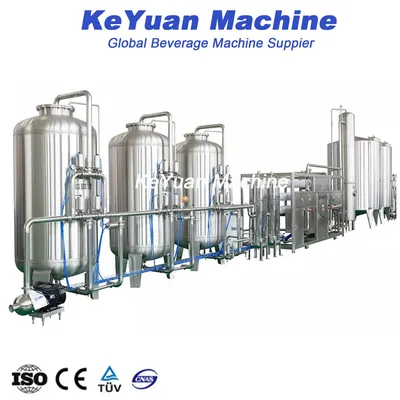
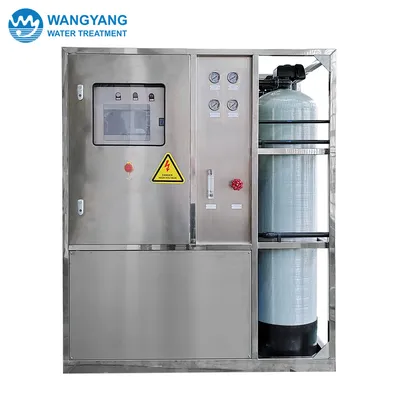
Reverse Osmosis RO Machine for Commercial Use 0.25-0.5 Ton/Hr. Industrial grade RO membrane element, stable salt rejection rate 97%-99.5%. Remove dissolved salts, heavy metals, colloids, bacteria and organics to produce qualified industrial pure water. Complete multi-stage pretreatment system including multimedia filter, activated carbon filter, water softener and security filter. Automatic dosing for scale inhibition to reduce membrane fouling and. Automatic PLC control system with touch screen. Real-time monitoring of conductivity, pressure and flow. Support automatic membrane flushing, fault alarm and multiple pressure protection. Variable frequency high pressure booster system, adjust operating pressure adaptively to save energy. Optimized concentrated water recycling design, water recovery rate reaches 60%-75% to save raw wat. Anti-corrosion industrial structure. Stainless steel frame, UPVC or 304 stainless steel pipeline. Pressure resistant membrane housing, prevent leakage in humid workshop environment. Modular skid-mounted integrated design, compact structure, easy transportation and installation. Capacity expandable, single stage or double stage RO system customizable. Wide range of raw water adaptability, suitable for tap water, groundwater and surface water. Widely used in electronics, electroplating, food, pharmacy, boiler feed water, chemical and photovoltaic in. Multiple safety protection: low water level protection, high/low pressure protection, pump overload protection. Automatically stop operation under abnormal conditions. It can be equipped with EDI ultra-pure water module, UV sterilizer and water tank system to meet higher water purity requirements.
Specifications
Model NO.0.25-0.5Ton/hr
ApplicationIndustry
CertificationISO9001
CustomizationAvailable
Salt Rejection Rate98.0%