Loading…
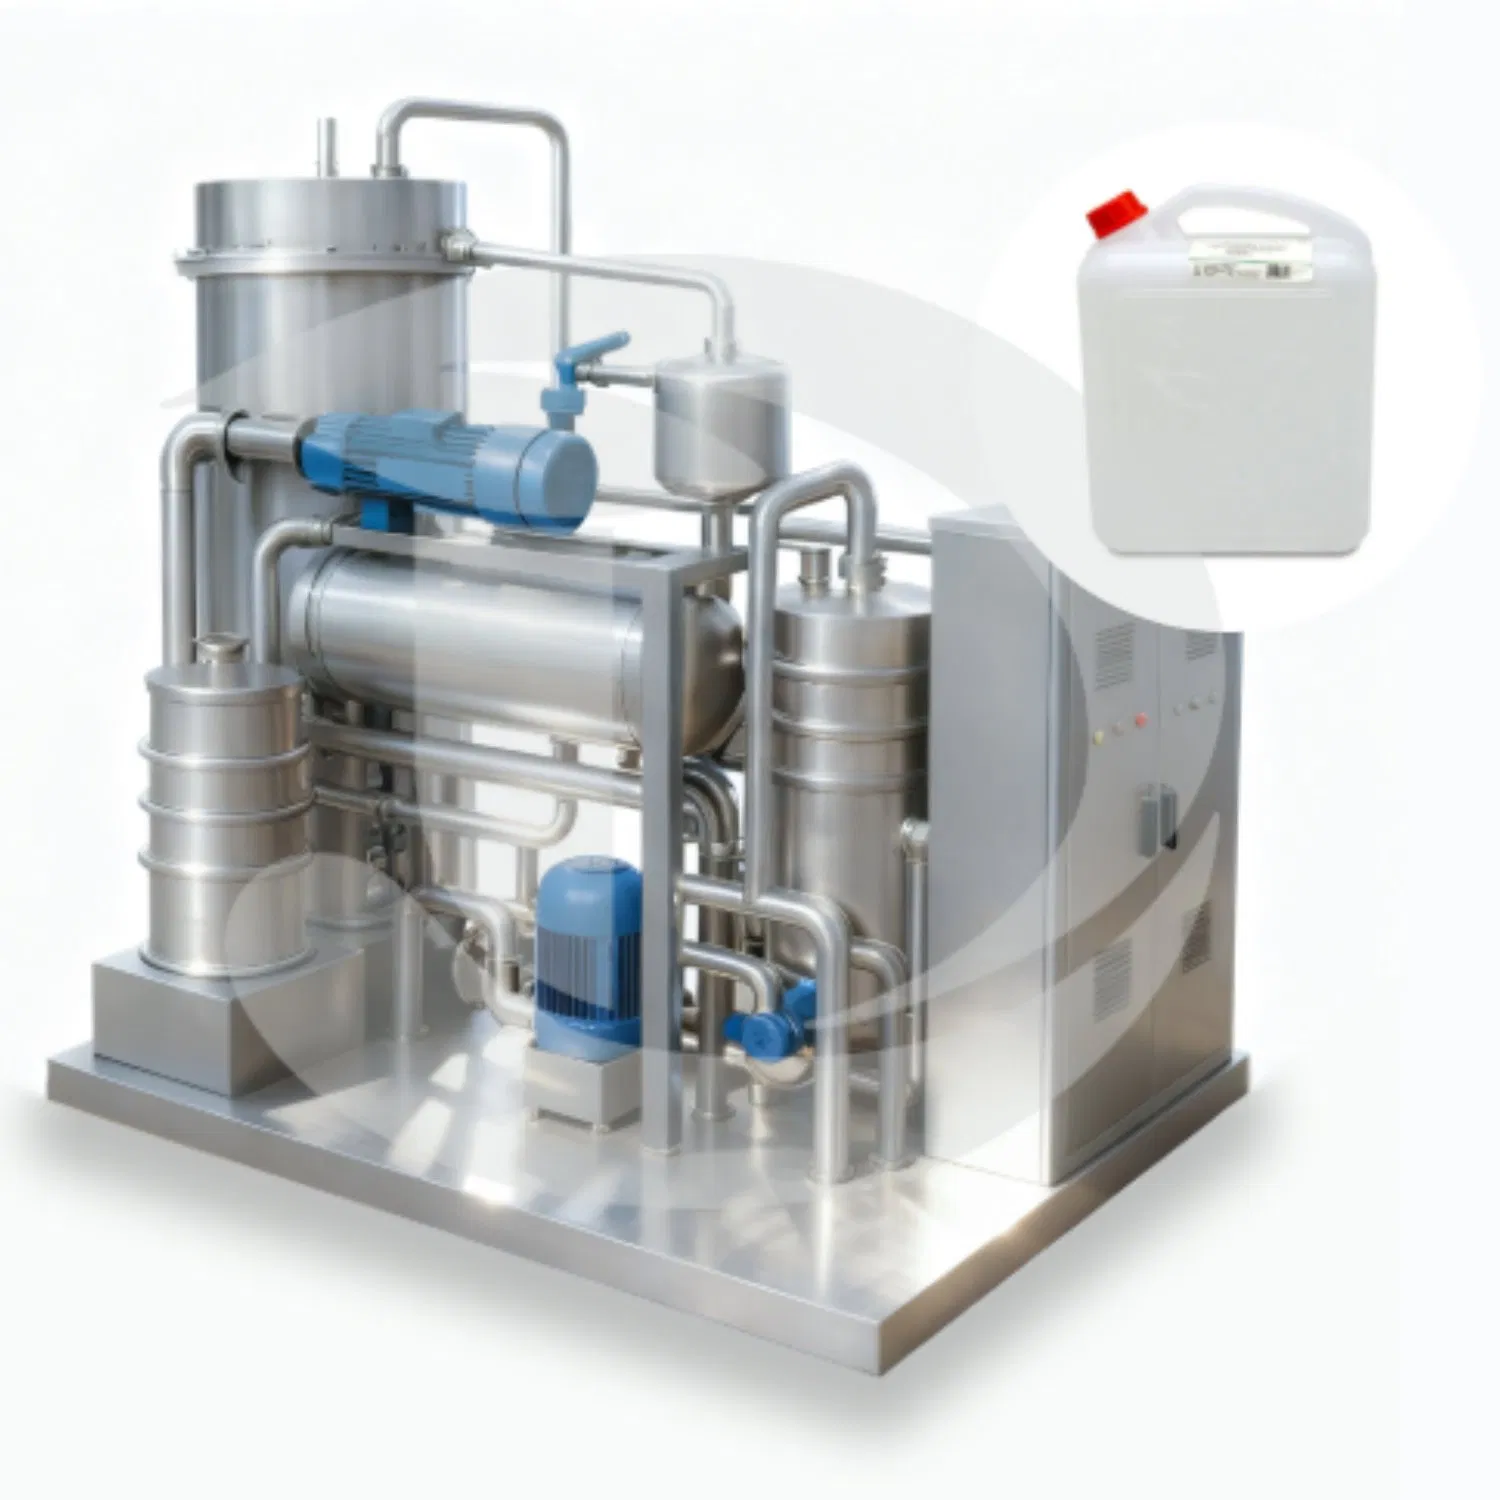
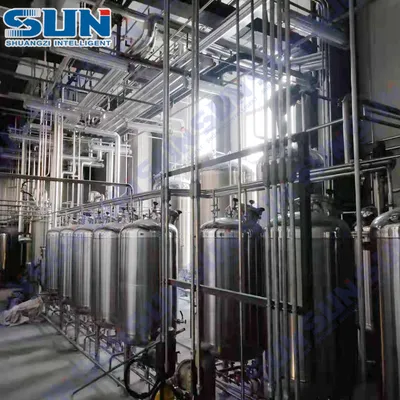
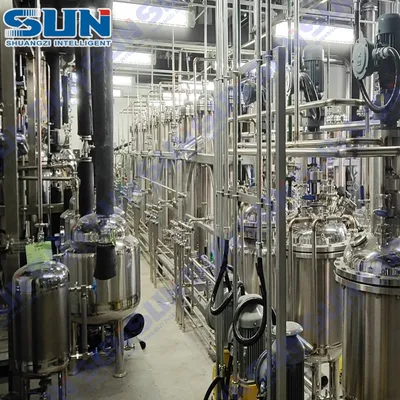
Flame-Retardant High-Gravity Heat Pump Ethanol Separation Solvent Recovery Distillation Refinery System
5.0InStock Source-listed auditby Jiangsu Super Distillation Technology Co., Ltd.
₹1,08,55,000≈ $130,000 · indicative, confirm with supplier
Description
Flame-Retardant High-Gravity Heat Pump Ethanol Separation Solvent Recovery Distillation Refinery System. Supergravity Mass Transfer: Centrifugal field increases interfacial area by 20x and mass transfer rates by 1-3 orders of magnitude. Heat Pump Energy Recovery: Closed-loop reverse Carnot cycle enables bidirectional heat/cold utilization for highly efficient energy recovery. Compact Footprint: System footprint is typically one-tenth of conventional distillation columns, suitable for space-limited installations. Electric Operation: Runs on electricity without requiring steam or cooling water, simplifying utilities and installation. Low Fouling & CIP: Enhanced turbulence reduces fouling; includes automatic CIP function for online cleaning and easy maintenance. Wide Solvent Compatibility: Suitable for methanol, ethanol, acetone, DMF, DMSO, and many other organic solvents. Heat-Sensitive Material Friendly: Low liquid holdup and short residence time reduce thermal stress, ideal for heat-sensitive or high-viscosity materials. Comprehensive EPC Service: Provides turnkey services from consultation and feasibility studies to fabrication, installation, and long-term maintenance.
Specifications
TypeDistillation Equipment
Warranty1year
Model NO.VHPS
CustomizationAvailable
After-sales Service1year