Loading…
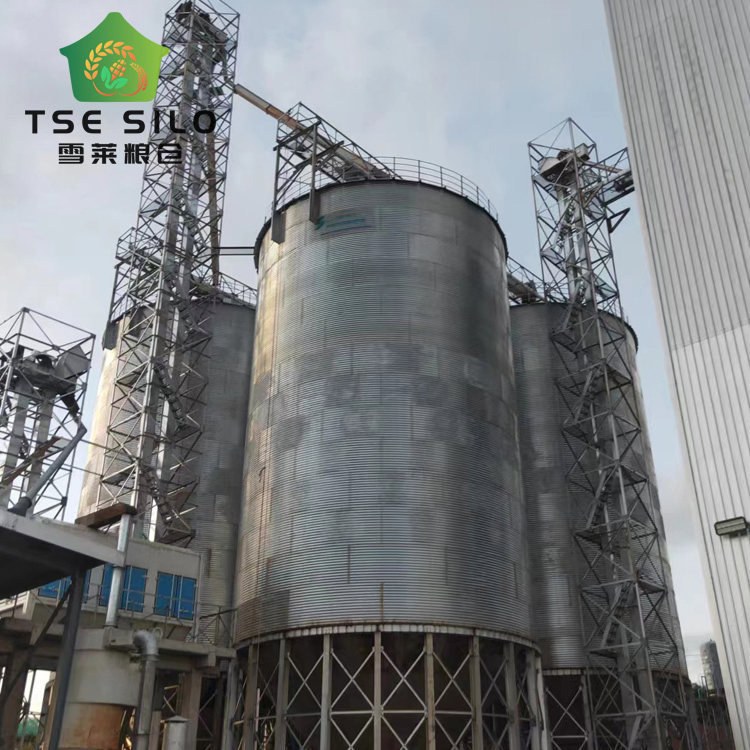
Factory Vertical Grain Bucket Elevator
5.0InStock Source-listed auditby Shandong Shelley Grain Steel Silo Co., Ltd.
₹4,17,500≈ $5,000 · indicative, confirm with supplier
Payment
LC, T/T, D/P, PayPal, Western Union, Small-amount payment
Incoterms
FOB, CIF, CFR, EXW
Description
Factory Vertical Grain Bucket Elevator. Heat and Fire Resistant: Constructed with carbon steel featuring heat and fire resistant properties for safe grain transport. High Capacity Range: Offers working capacity ranging from 10 to 800 cubic meters per hour for various bulk materials. Customizable Height: Height can be customized to meet specific installation requirements and facility layouts. Anti-Explosion Safety: Equipped with anti-explosion openings at head, tube, and booth to prevent dust explosion risks. Anti-Slip Mechanism: Features cage type booth wheel and non-return device to prevent belt slipping and material backflow. Waterproof Design: Utilizes bitting type tube technology ensuring excellent waterproof quality for long-term durability. Low Power Consumption: Designed with reasonable transmission structure to minimize energy usage during operation. Comprehensive Certifications: Holds ISO, BV, and CE certifications ensuring compliance with international safety and quality standards.
Specifications
WarrantyOne Year
Model NO.TDTG50/23
StructureConveyor System
CustomizationAvailable
After-sales Service24 Hours Online