Loading…
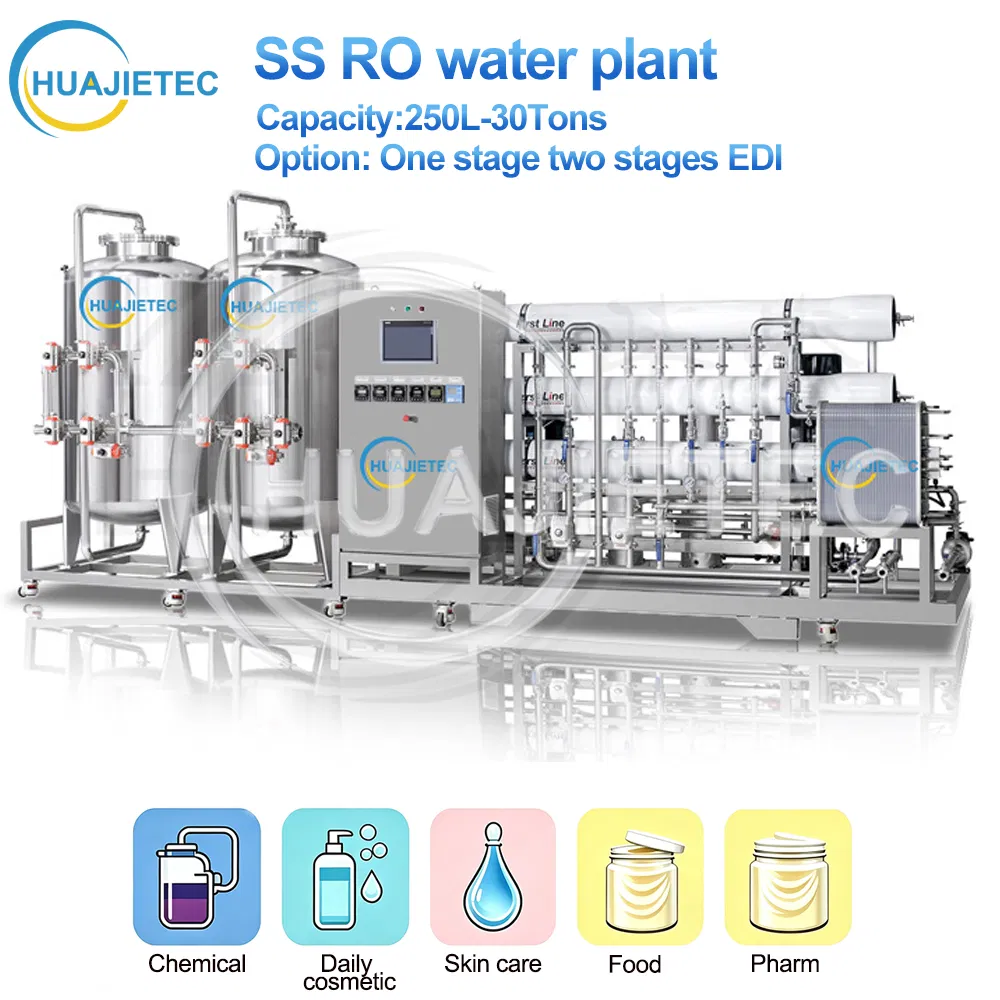
Huajietec 250-50tons Reverse Osmosis RO Water Purifier System Treatment Plant
5.0InStock Source-listed auditby Guangzhou Huajie Intelligent Technology Co., Ltd.
₹2,50,500≈ $3,000 · indicative, confirm with supplier
Payment
Description
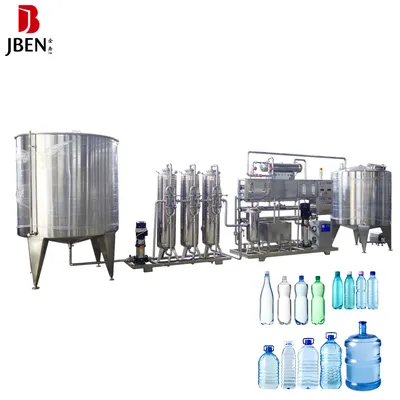
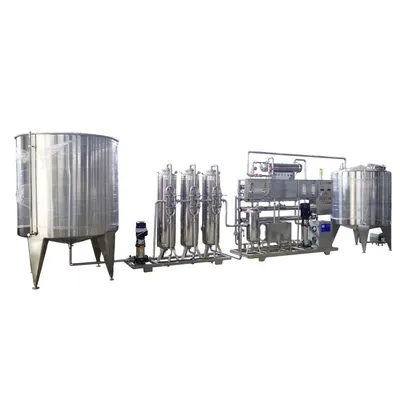
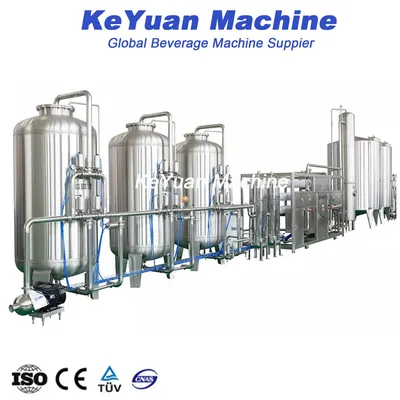
Huajietec 250-50tons Reverse Osmosis RO Water Purifier System Treatment Plant. Wide processing capacity range: Available from 250L per hour up to 50 tons per hour to satisfy different factory water consumption demands. Reliable SEHAO reverse osmosis membrane: Adopt high quality Korea CSMmembrane element for stable desalination and excellent water producing performance. Automatic flushing function: Built in automatic flushing program reduces membrane fouling and extends service life of filter membranes. Flexible material selection: Support stainless steel or FRP glass fiber reinforced plastic material for main equipment according to site environment. Stable water output quality: Effectively remove heavy metals impurities bacteria and soluble salts to reach standard purified water quality. Intelligent running control: Realize automatic start stop and fault alarm to reduce manual operation workload for operators. Compact reasonable structure: Optimized layout saves workshop space and brings convenience for installation and daily maintenance. Low operation cost: Low power consumption and high water recovery rate help factories save long term water and electricity expenses. Strong scene adaptability: Suitable for cosmetic food beverage pharmaceutical and daily chemical factory purified water preparation. Expandable system design: Can connect with pre treatment EDI device to form high purity water treatment solution for higher process requirements.
Specifications
Model NO.HJ-RO
ApplicationIndustry
CertificationCE
CustomizationAvailable
Salt Rejection Rate98.0%