Loading…
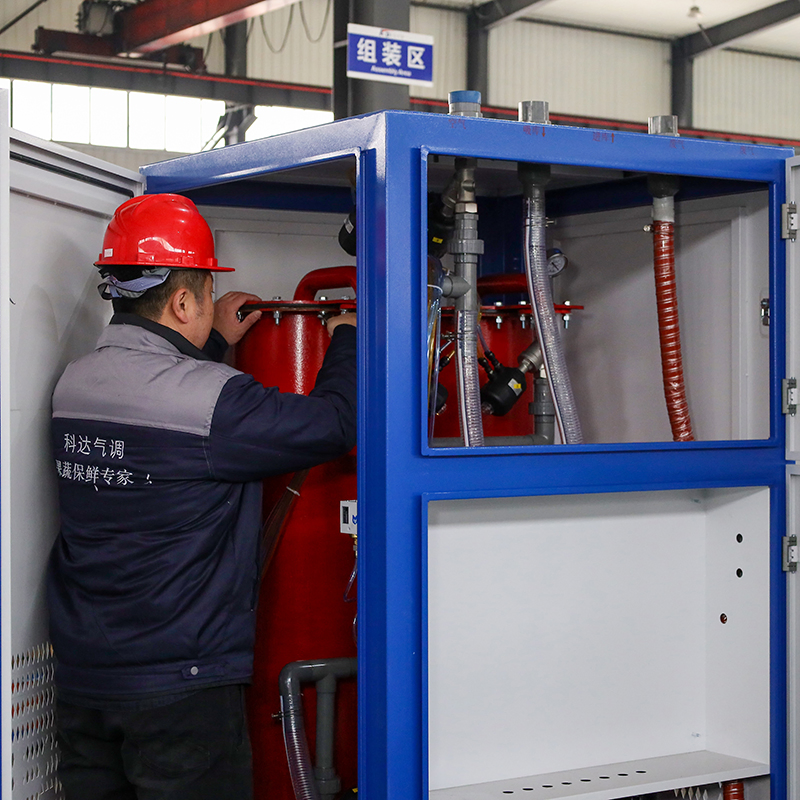
Controlled Atmosphere Cold Room Equipment for Fresh Produce Preservation
5.0InStockby Yantai Keda Zhixian International Trade Co., Ltd
₹6,09,550≈ $7,300 · indicative, confirm with supplier
Payment
T/T, PayPal
Incoterms
Description
Controlled Atmosphere Cold Room Equipment for Fresh Produce Preservation. Integrated Gas Analysis: Combines oxygen removal, carbon dioxide removal, and gas concentration analysis in one machine. Remote Monitoring: Cloud technology enables real-time monitoring via mobile phones and computers with data printing. High Efficiency Technology: Features automatic frequency conversion and voltage transformation for optimal equipment efficiency. Twin-Tower System: Utilizes carbon molecular sieve adsorption vessels for effective gas separation and preservation. Global Support: Provides 24/7 technical assistance and spare parts supply worldwide. Certified Quality: Certified with ISO 9001, CE, and GOST with over 20 patents. Versatile Application: Suitable for preserving fruits, vegetables, and flowers in small to micro warehouses. Custom Configurations: Custom configurations for technical specifications and dimensions are available upon request.
Specifications
ConditionNew
Model NO.KD-200
Noise LevelLow
CertificationCE, ISO
Application FieldsFood, Fruits and Vegetables