Loading…
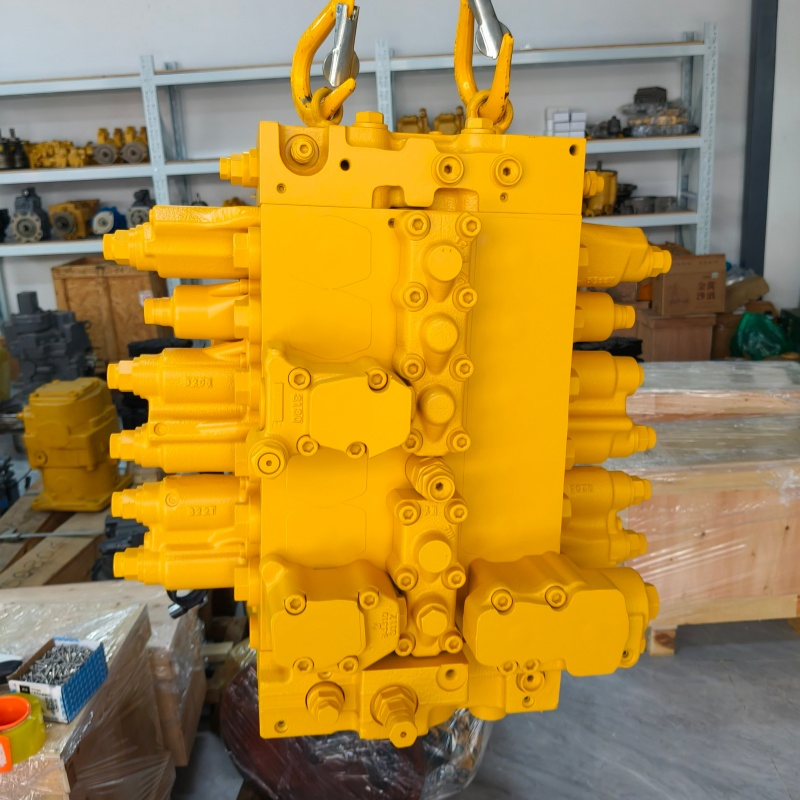
Lab Tested Main Valve Unit Hydraulic Control Valve for Mineral Site Earth Moving Digger
5.0InStock Source-listed auditby Guangzhou Power Parts Co., Limited
₹41,667≈ $499 · indicative, confirm with supplier
Payment
Description
Lab Tested Main Valve Unit Hydraulic Control Valve for Mineral Site Earth Moving Digger. Strict Quality Testing: Full bench flow and pressure testing performed before shipment to ensure stability. Durable Material: Constructed with high-precision hardened spools and rigid alloy cast iron valve body. Wide Compatibility: Well compatible with various excavators and earth-moving equipment for direct-swap installation. OEM Customization: Accepts OEM customized production based on customers' special requirements and technical drawings. Global Certification: Certified with CE and ISO9001: 2000 standards for reliable performance. Efficient Maintenance: Supports convenient on-site maintenance to reduce machine downtime and extend service life. Low Leakage Design: Optimizes system operating efficiency and lowers internal leakage for better hydraulic performance. Professional Manufacturer: Exported to over 70 countries with reliable quality and cost-effective pricing.
Specifications
TypeMain Control Valve
Warranty6 Months Warranty
Model NO.control valve
CustomizationAvailable
After-sales ServiceReplacement or Compensation Within Warranty