Loading…
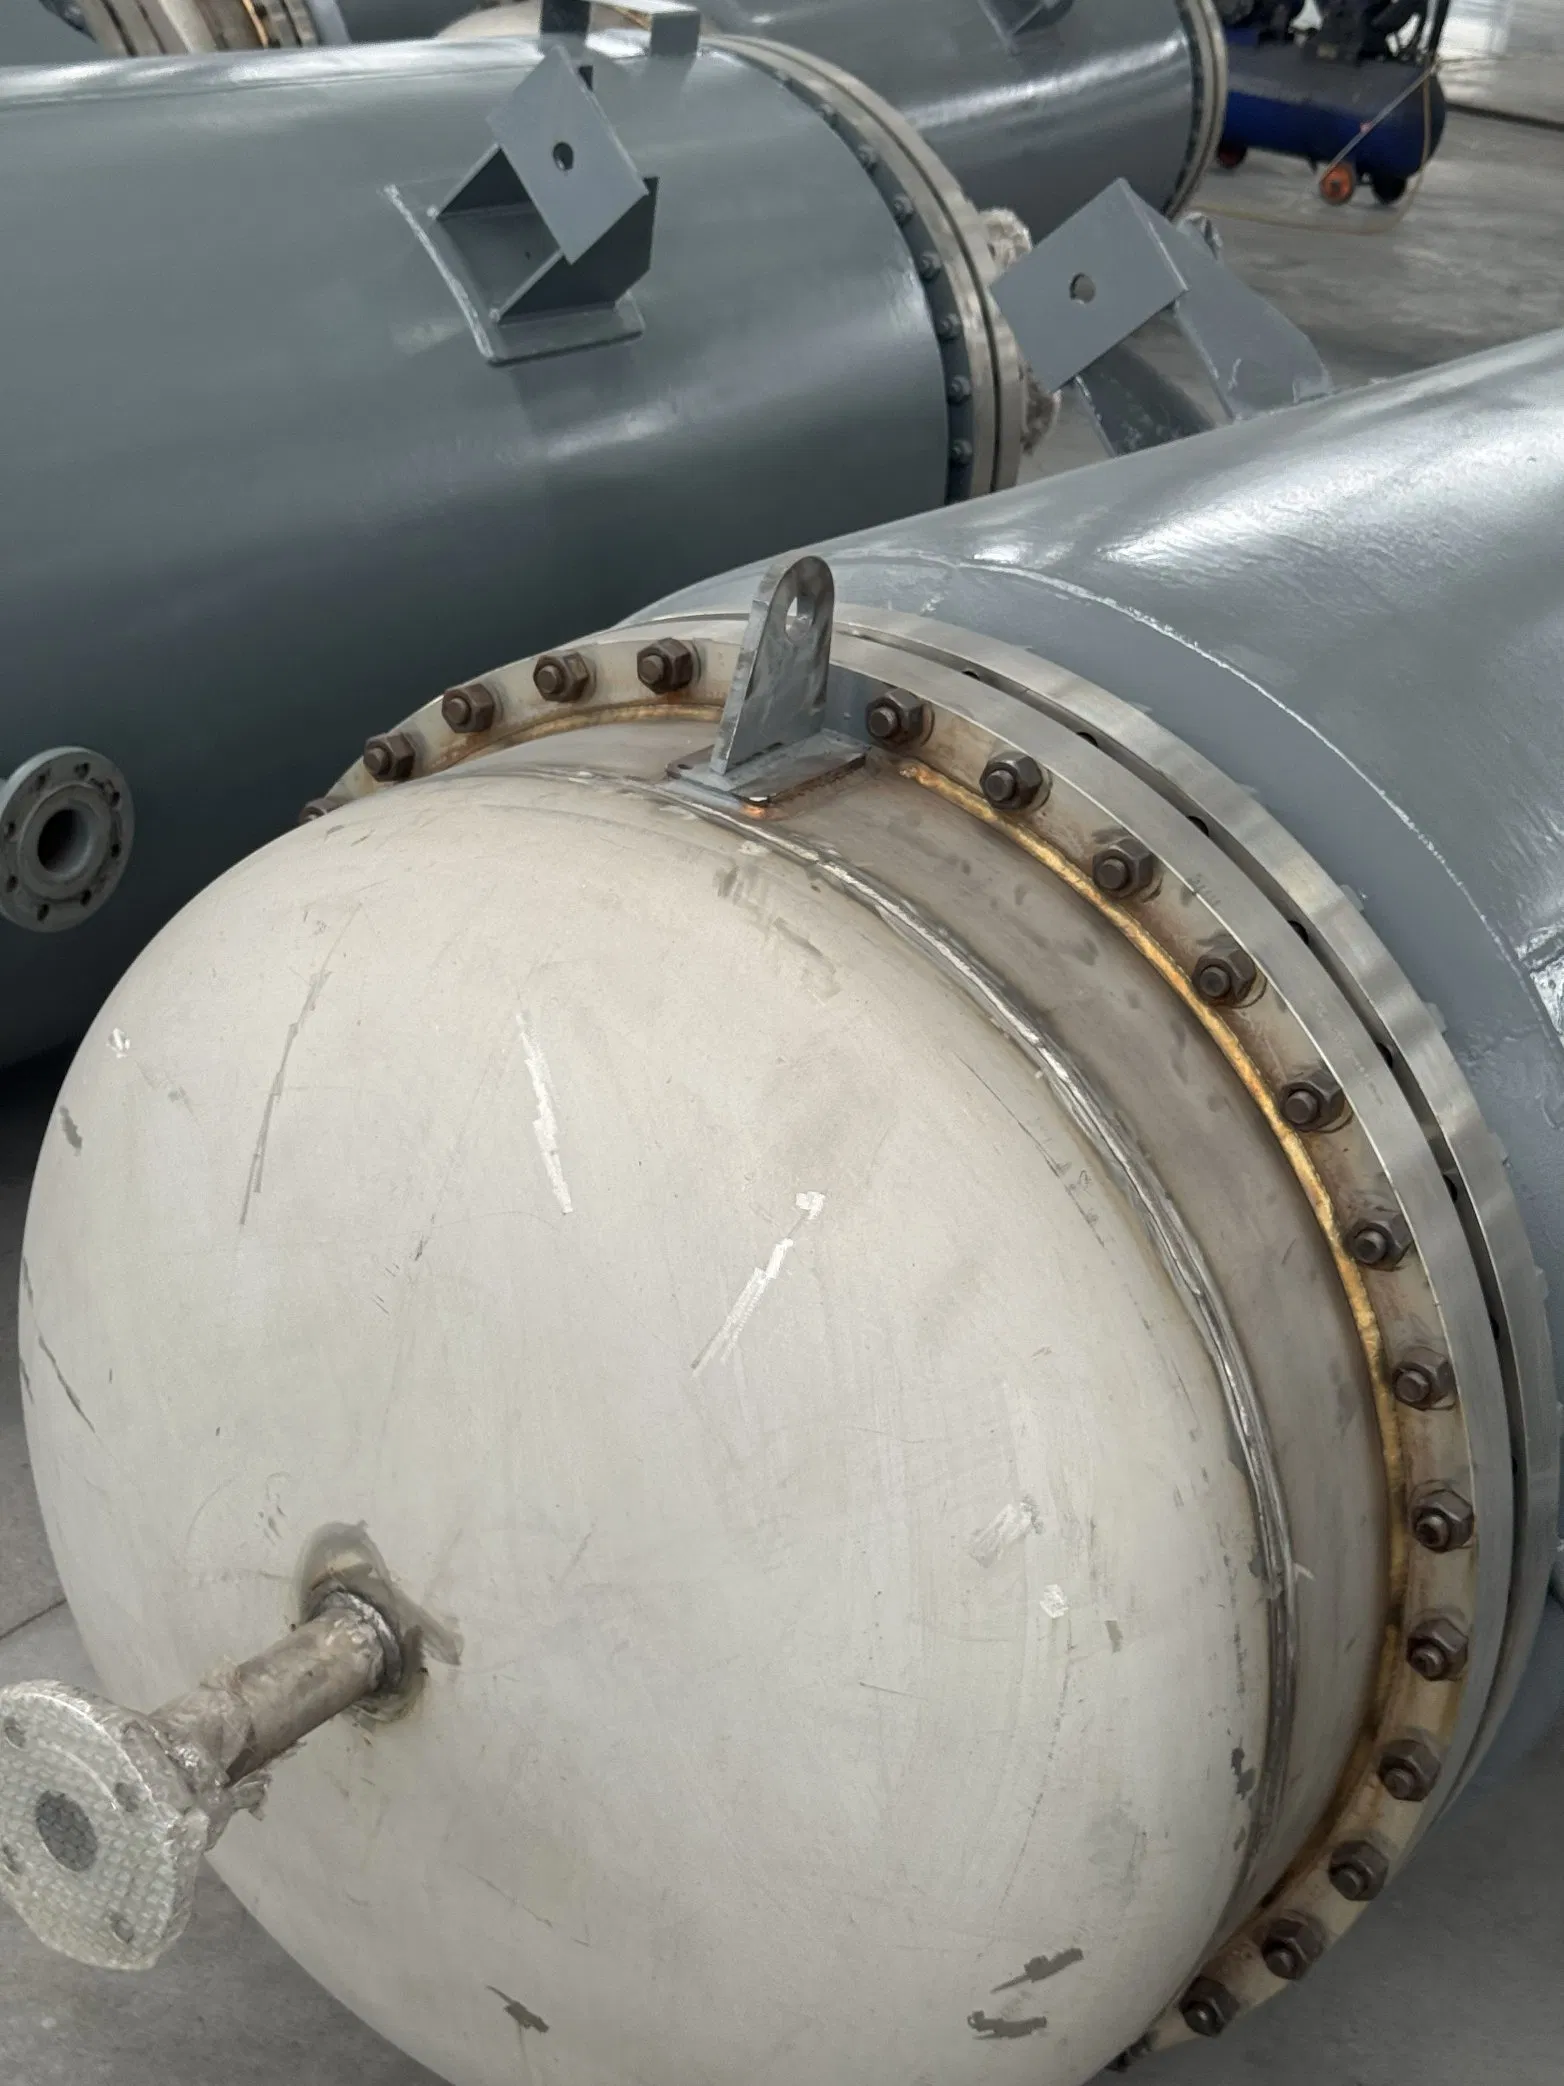
Double Tube-Sheet Heat Exchanger for Pharmaceutical Sterile Processes
5.0InStock Source-listed auditby Jiangsu Xinmen Energy Equipment Co., Ltd.
₹8,35,000≈ $10,000 · indicative, confirm with supplier
Payment
Description
Double Tube-Sheet Heat Exchanger for Pharmaceutical Sterile Processes. 15+ Years R&D Experience: Deep expertise in heat exchanger design for high temp, pressure, and corrosion scenarios. Wide Material Selection: Customizable in 304/316L stainless steel, titanium, nickel alloy, and other specialized materials. Multi-Industry Application: Serves 12 major industries including chemical, energy, pharmaceuticals, and environmental protection. Cost-Effective Design: Design lifespan exceeds industry average, reducing maintenance costs by 50%. Strict Quality Control: Features PMI testing, hydraulic pressure tests, and non-destructive weld inspections. Global Certification: Holds ISO 9001, CE, PED, ASME U Stamp, and FDA compliance for food-grade equipment. Flexible Customization: Offers full customization from samples, designs, or minor adjustments for specific needs. Direct Factory Supply: Manufacturing factory with in-house R&D, production lines, and export license.
Specifications
WarrantyOne Year
ApplicationHeater, Cooler, Vaporizer
CertificationCE
CustomizationAvailable
After-sales ServiceOnline Guidance for Maintenance