Loading…
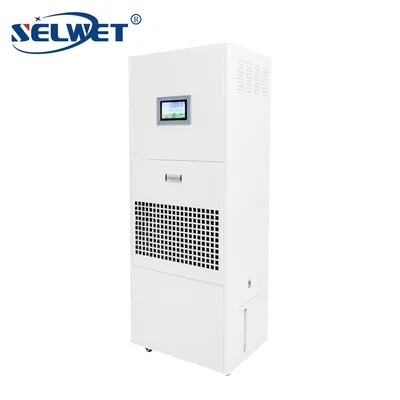
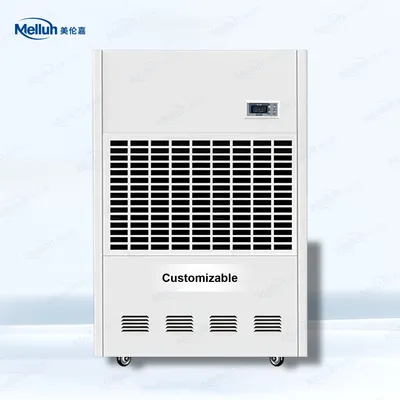
Capacity Industrial Dehumidifier High-Efficiency Humidity Moisture Absorber for Food Processing Plants
5.0InStock Source-listed auditby Shanghai GLOMRO Industrial CO., LTD.
₹35,655≈ $427 · indicative, confirm with supplier
Description
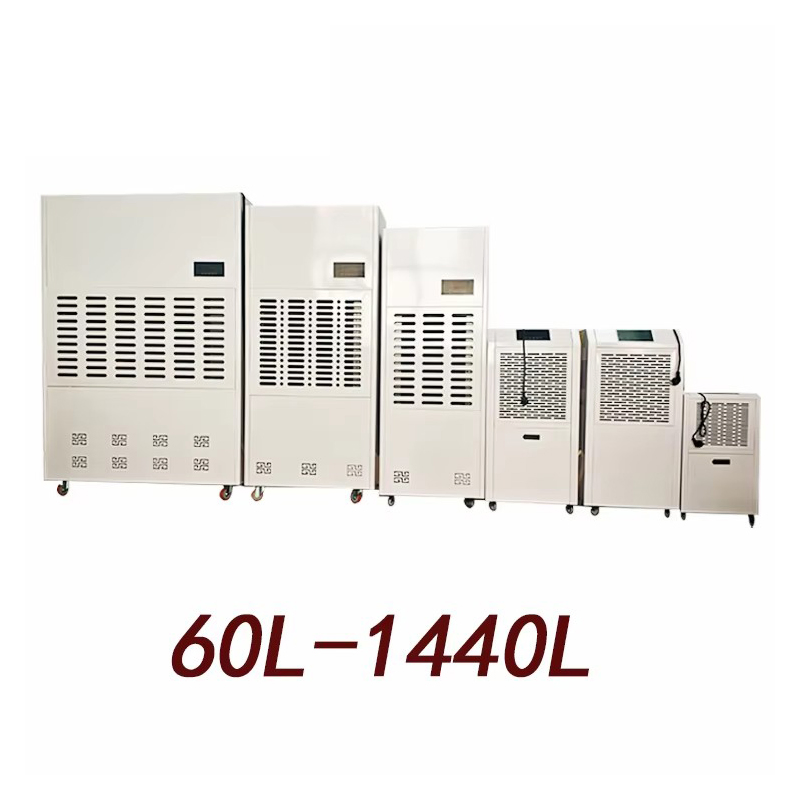
Capacity Industrial Dehumidifier High-Efficiency Humidity Moisture Absorber for Food Processing Plants. High Dehumidification Capacity: Models range from 60L/D to 1440L/D for various industrial needs. Hitachi Twin Rotor Compressor: Ensures low noise, long service life, and lasting power. Precision CNC Body Construction: Tough, impact-resistant sheet metal with neat flame-cut edges. LED Touch Screen Control: Allows adjustable humidity range from 10% to 95% with ease. Dual-Layer Thickened Filters: Double-sided extra-thick filters ensure healthier air quality. Flexible Drainage Options: Supports both direct hose drainage and water tank collection. Full Customization Available: Offers full, minor, and flexible customization from designs or samples. 24-Hour Bidirectional Timer: Automated operation with precise timing control for efficiency.
Specifications
FanWith Fan
Model NO.GLO
CertificationISO, CE
CustomizationAvailable
Dehumidification Capacity720L/D