Loading…
Intelligent Reverse Osmosis Water Purifier for Eco-Friendly Deionization
5.0InStock Source-listed auditby Shandong Yufeng Water Treatment Equipment Co., Ltd.
₹3,93,285≈ $4,710 · indicative, confirm with supplier
Description
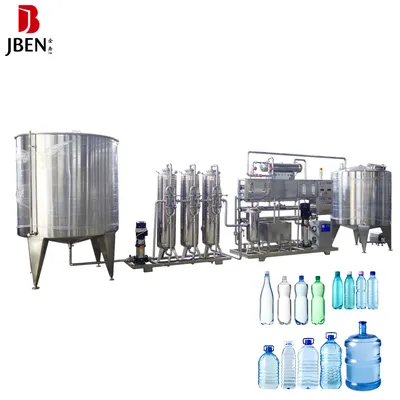
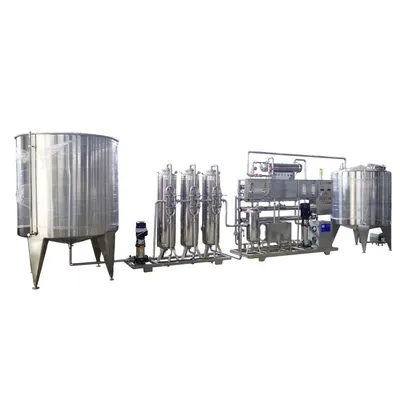
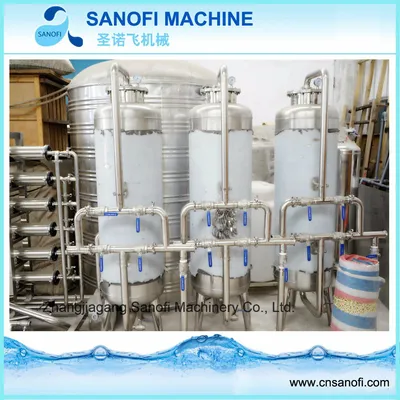
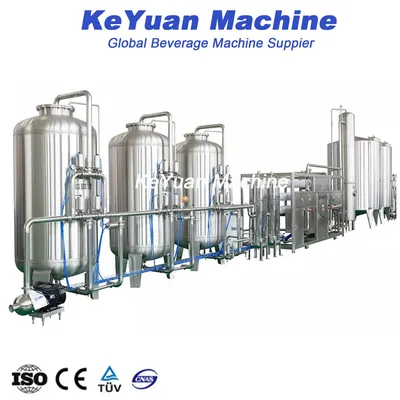
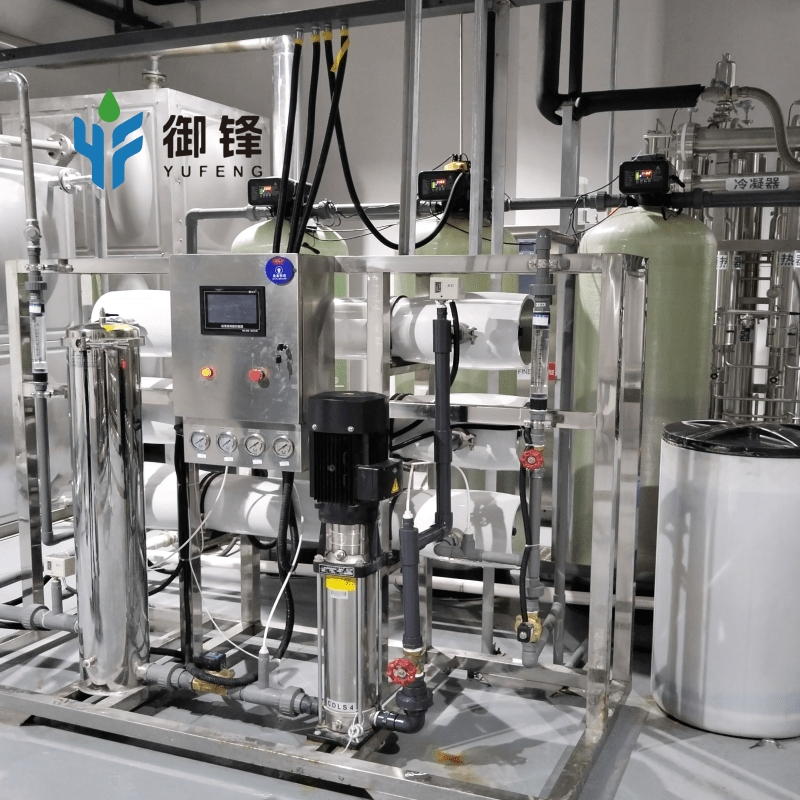
Intelligent Reverse Osmosis Water Purifier for Eco-Friendly Deionization. High-flow 3000L/H industrial reverse osmosis system delivers stable continuous purified water production for large-scale commercial and industrial applications. Advanced RO membrane filtration technology effectively removes dissolved salts, heavy metals, bacteria, chlorine, and organic impurities, ensuring high-purity water quality. Multi-stage pretreatment system including quartz sand filter, activated carbon filter, and precision filtration helps improve purification efficiency and extend RO membrane lifespan. Intelligent automatic control system supports automatic flushing, pressure monitoring, online operation control, and fault alarm functions for reliable and convenient operation. Durable stainless steel modular structure with energy-efficient design supports customized capacity, voltage, and filtration configurations for different industrial water treatment projects.
Specifications
Model NO.Reverse Osmosis Equipment Intelligent Water Purifi
ApplicationIndustry
CertificationISO9001, RoHS, CE, CH
CustomizationAvailable
Salt Rejection Rate99.4%