Loading…
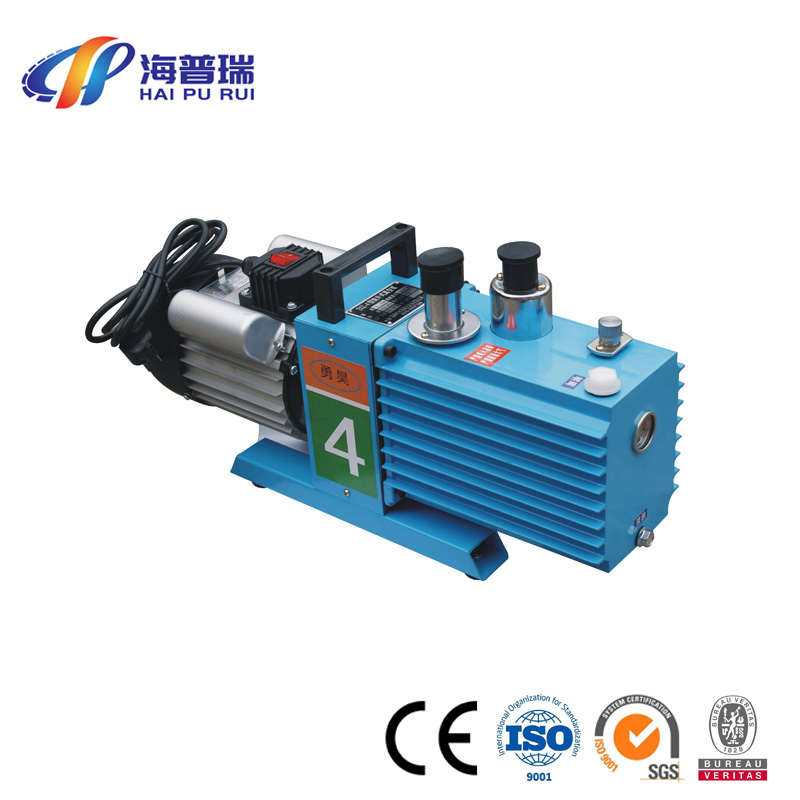
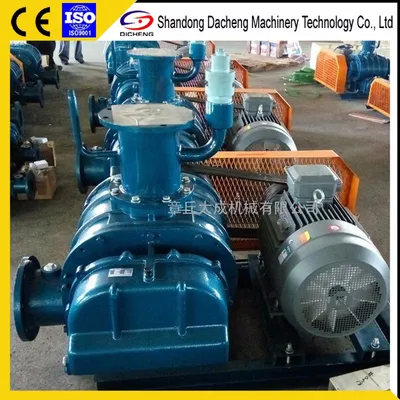
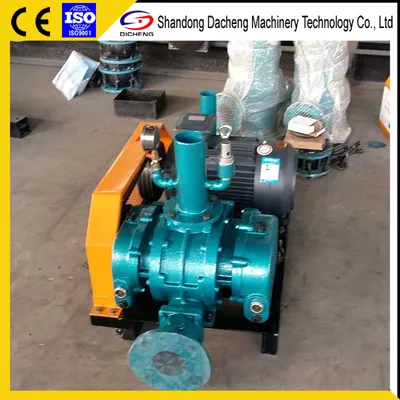
High-Efficiency Industrial Rotary Vane Vacuum Pump for Optimal Performance
5.0InStock Source-listed auditby Shenyang Haipurui Vacuum Technology Co.,Ltd.
₹8,350≈ $100 · indicative, confirm with supplier
Payment
Description
High-Efficiency Industrial Rotary Vane Vacuum Pump for Optimal Performance. Oil-Free Operation: Provides clean vacuum environment without oil contamination for sensitive applications. Explosion-Proof Capability: Available in explosion-proof type for safe use in petroleum, chemical, and mining industries. Anti-Reflux Safety Valve: Automatically cuts off vacuum and fills chamber with air during power loss to prevent oil reflux. Wide Application Scope: Suitable for vacuum welding, food packaging, refrigeration, and laboratory equipment matching. ISO9001 Certified Quality: Manufactured under ISO9001:2015 quality management system with rigorous inspection protocols. Flexible Customization: Offers full customization from samples and designs including flow, speed, and motor power. 1-Year Comprehensive Warranty: Includes 1-year warranty coverage for mechanical defects and performance assurance.
Specifications
Warranty1 Year
Model NO.2XZ
Oil or NotOil Free
CustomizationAvailable
After-sales ServiceThe Best Service