Loading…
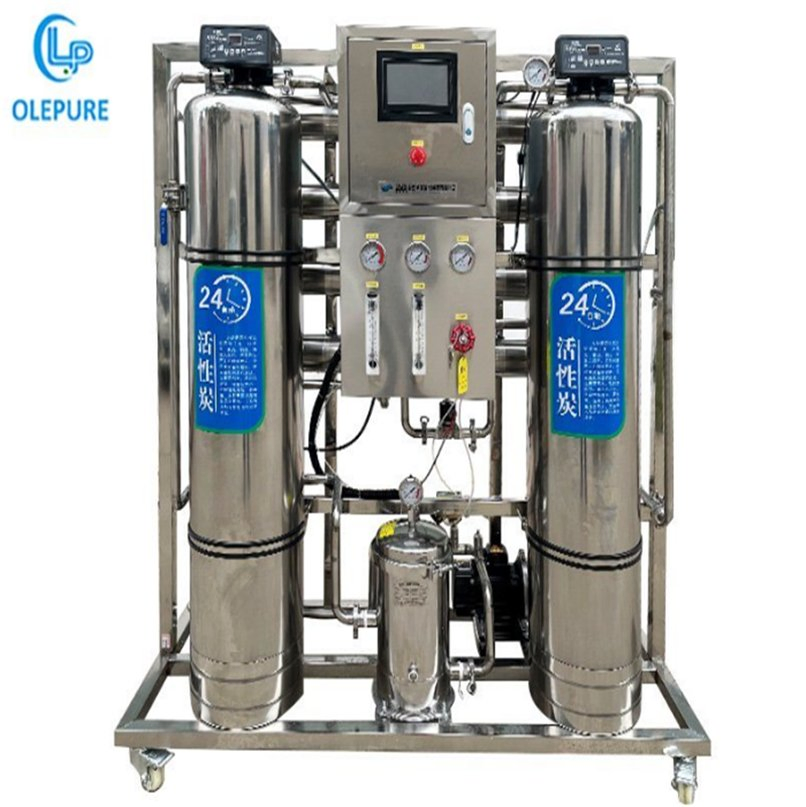
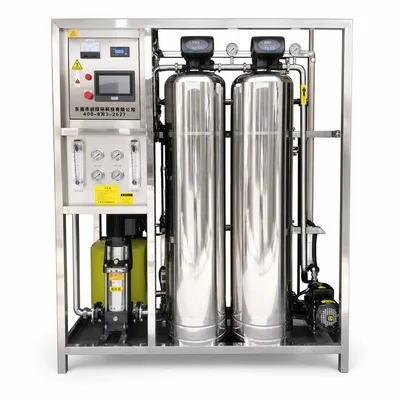
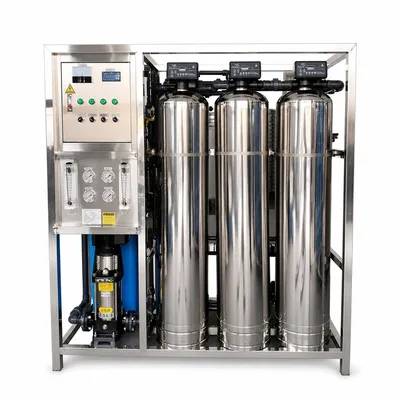
1-100 T Per H Industrial Water Treatment RO System Reverse Osmosis Water Purification System
5.0InStock Source-listed auditby Yancheng Olap Water Purification Equipment Technology Co., Ltd.
₹43,420≈ $520 · indicative, confirm with supplier
Description
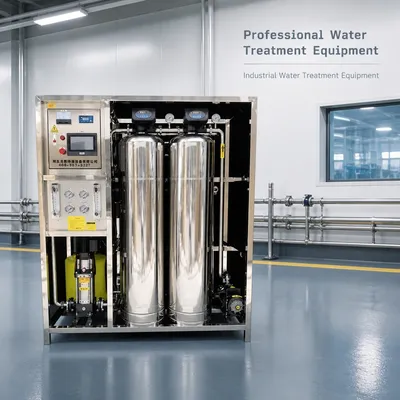
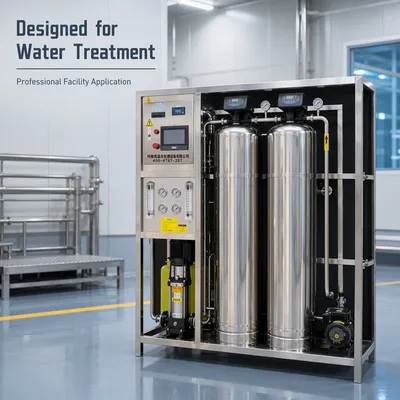
1-100 T Per H Industrial Water Treatment RO System Reverse Osmosis Water Purification System. High Efficiency Filtration: Five-level filtration system with 75% water recovery rate for efficient purification. Versatile Raw Water Adaptability: Suitable for tap, lake, reservoir, river, and underground water with TDS <1000ppm. Real-time Quality Monitoring: Equipped with online monitoring to ensure consistent water safety and quality. Flexible Customization: Accepts customization for capacity (1T-100T/H), raw water quality, and logo embossing. Core Component Quality: Features durable pressure vessel, pump, PLC, and RO membrane for reliable performance. Certified Safety: Product holds CQC certification ensuring compliance with safety and quality standards. Compact Design: Machine size 1800x800x1920mm and weight <=1000kg for easy installation and space saving. Sample Testing Support: Provides sample testing within 2-3 days with free sample cost return on bulk orders.
Specifications
TypeReverse Osmosis
UsageEnvironmental Protection, Chemical Industry
Model NO.OLP-RO
Motive ForceElectric power
CustomizationAvailable