Loading…
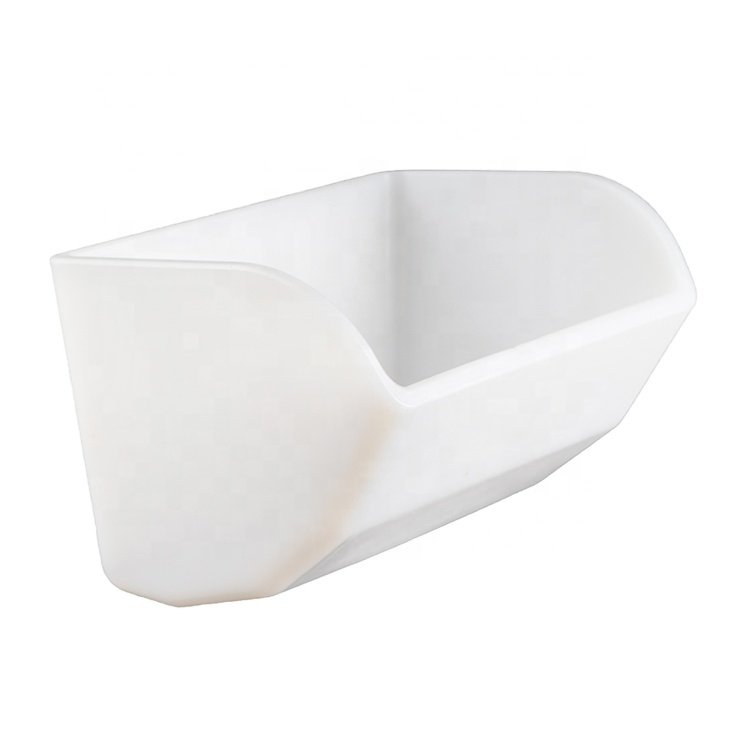
HDPE and Nylon Plastic Elevator Bucket for Vertical Bucket Conveyor
4.0InStock Source-listed auditby Jiangsu Jingwei Conveying Equipment Co., Ltd
₹84≈ $1 · indicative, confirm with supplier
Payment
Description
HDPE and Nylon Plastic Elevator Bucket for Vertical Bucket Conveyor. High Performance Material: HDPE and Nylon options offer impact resistance, abrasion resistance, and no-corrosion properties. Food Grade Safety: Smooth surface and food grade certification ensure safe handling of grain, fodder, and seeds. Durable Design: Less weight prolongs service life of buckets and belts while reducing elevator consumption. Safety Features: No-sparking design avoids dust explosion, suitable for dry conditions and rough materials. Customization Available: Various materials and styles available to choose the proper bucket for specific needs. Extended Warranty Option: Standard one-year warranty can be extended after discussion and agreement. Strict Quality Control: Every single product is tested qualified before shipping with 100% process control. OEM and ODM Service: Own brand and custom manufacturing services available for specific requirements.
Specifications
TypeBucket Conveyor
UsageAgricultural Products Processing
MaterialHDPE/Nylon
Model NO.CC
CustomizationAvailable