Loading…
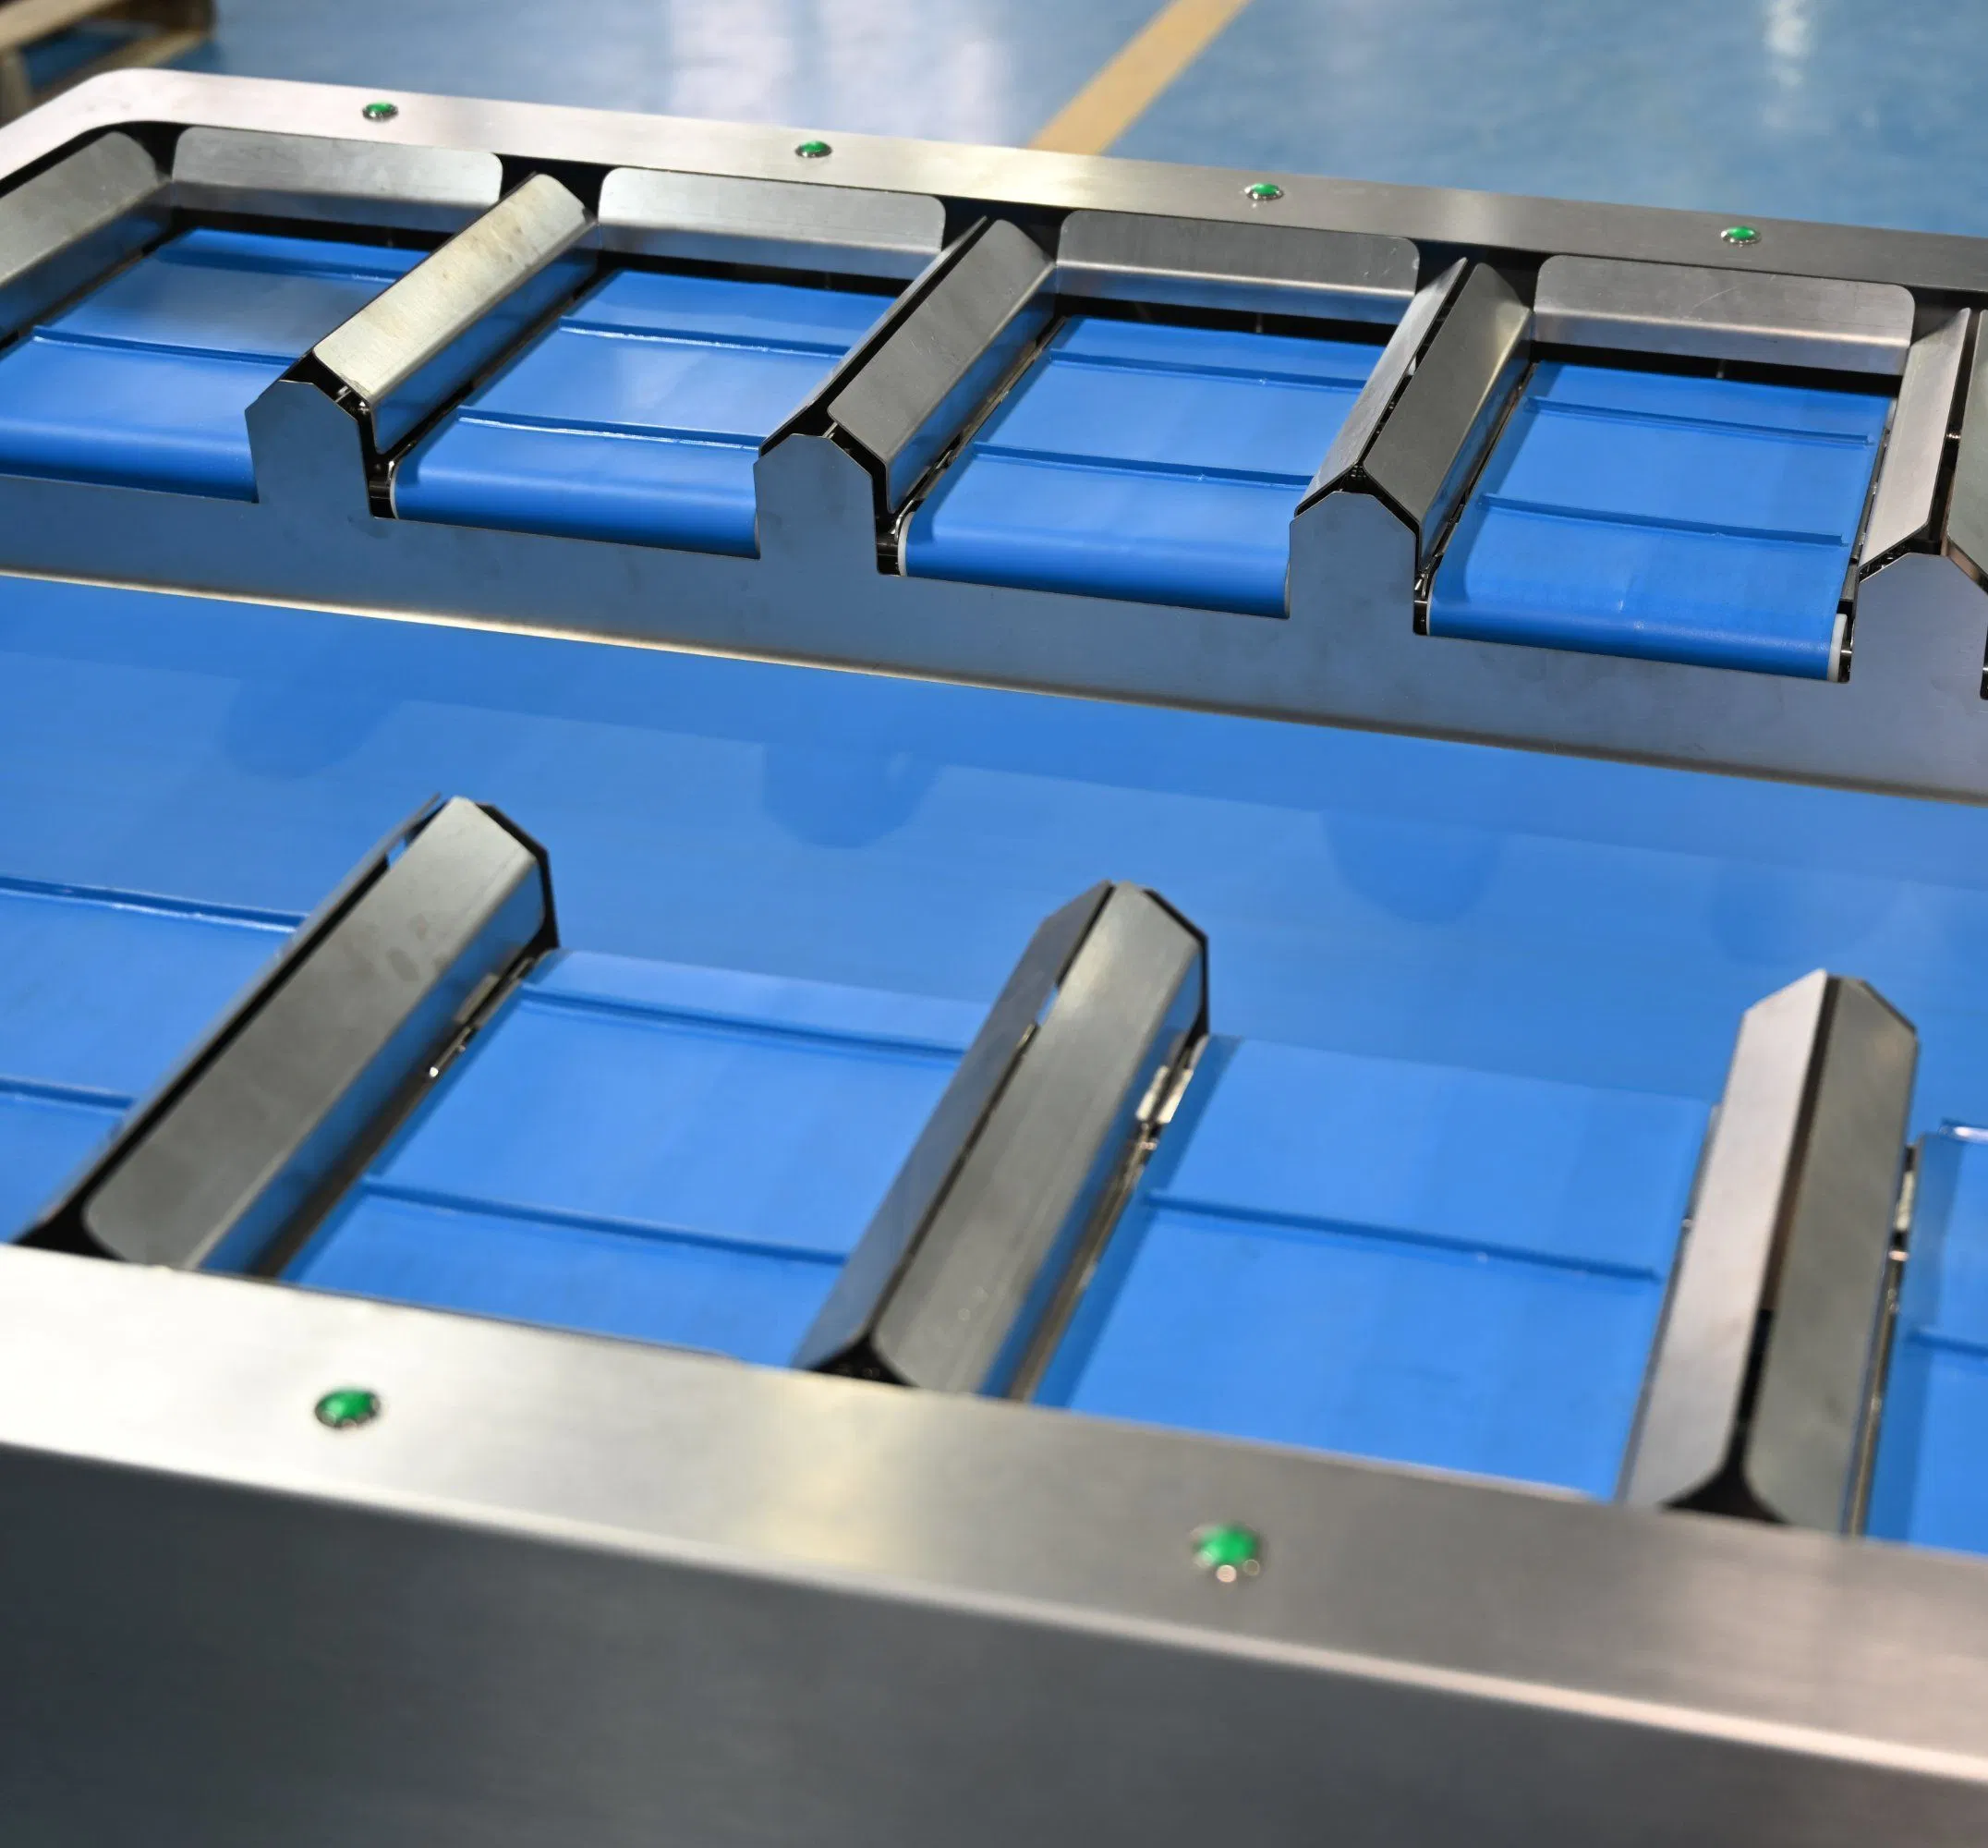
Cost-Effective Belt-Driven Automation Equipment for Food Industry
5.0InStock Source-listed auditby Lishui Hongmeng Import and Export Trading Co., Ltd.
₹8,19,052≈ $9,809 · indicative, confirm with supplier
Payment
LC, T/T, D/P, PayPal, Western Union, Small-amount payment
Description
Cost-Effective Belt-Driven Automation Equipment for Food Industry. High Precision Weighing: 12 independent hoppers with intelligent algorithm ensure stable accuracy and avoid waste. Gentle Material Handling: Belt conveying protects fragile, sticky, or irregular materials from damage and breakage. Wide Material Adaptability: Effectively weighs lumps, strips, flakes, frozen items, and floating materials with ease. CE International Certified: Products pass EU CE certification, ensuring superior quality and safety standards. Hygienic and Easy to Clean: Smooth operation and simple design meet industry hygiene standards for food processing. High Automation Level: Easy integration into automated packaging lines with stable and reliable capacity. 1-Year Warranty Coverage: Comprehensive 1-year warranty with support for installation services included. OEM/ODM Customization: Supports custom logos, designs, and flexible customization from samples or designs.
Specifications
Warranty1 Year Warranty
Model NO.HW-12PW-W160
CustomizationAvailable
Automatic GradeAutomatic
After-sales ServiceSupport Installation