Loading…
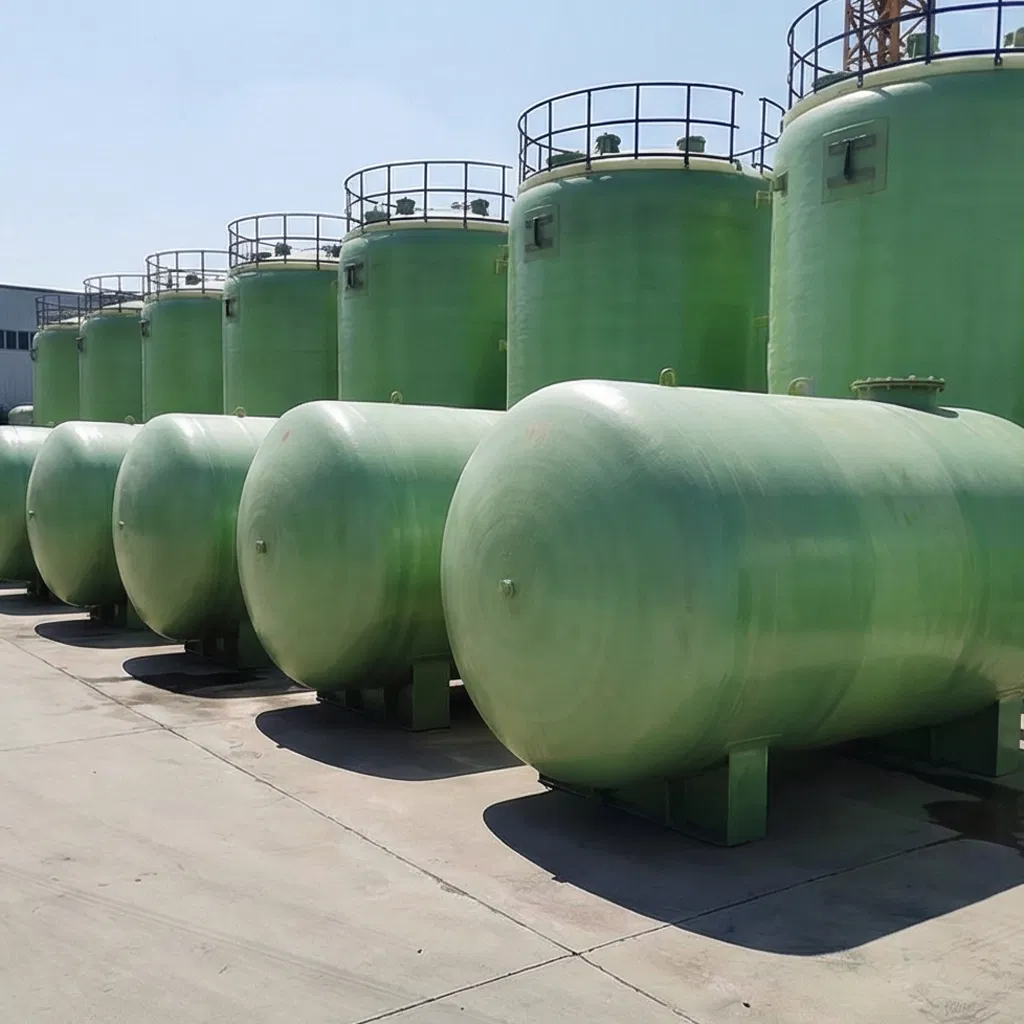
Heavy-Duty FRP Tank for Long-Lasting Industrial Chemical Solutions
InStock Source-listed auditby Hengshui Xinyi Composite Materials Co., Ltd.
₹41,750≈ $500 · indicative, confirm with supplier
Supplier information

Audited supplier
Description
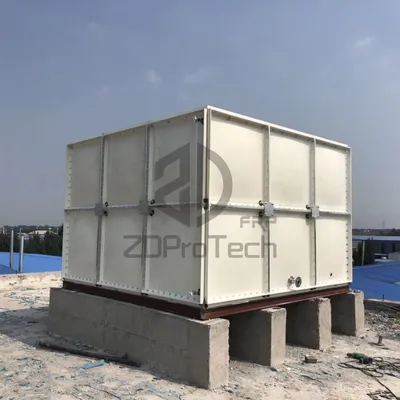
Heavy-Duty FRP Tank for Long-Lasting Industrial Chemical Solutions. Superior Corrosion Resistance: FRP material offers high resistance to acid, alkali, salt, and organic solvents. Lightweight and Strong: Specific gravity 1.5-1.9, far lower than steel, yet with higher mechanical strength. Customizable Design: Wall thickness and shape are designable to meet specific industrial requirements. Wide Application Scope: Suitable for chemical, petroleum, pharmaceutical, food, and water treatment fields. Multiple Certification: Certified with ISO3834, ISO9001, RoHS, and CE standards for quality assurance. Large Capacity Options: Max diameter up to 25000mm with volume reaching 5000m for large-scale needs. Thermal Insulation: Low coefficient of thermal expansion provides excellent thermal insulation properties. Established Manufacturer: Over 35 years experience with 32 national patents and leading domestic strength.
Specifications
MaterialFRP
Model NO.2
InstallationSitting Type
CertificationISO3834, ISO9001, RoHS, CE
Wall ThicknessDesignable