Loading…
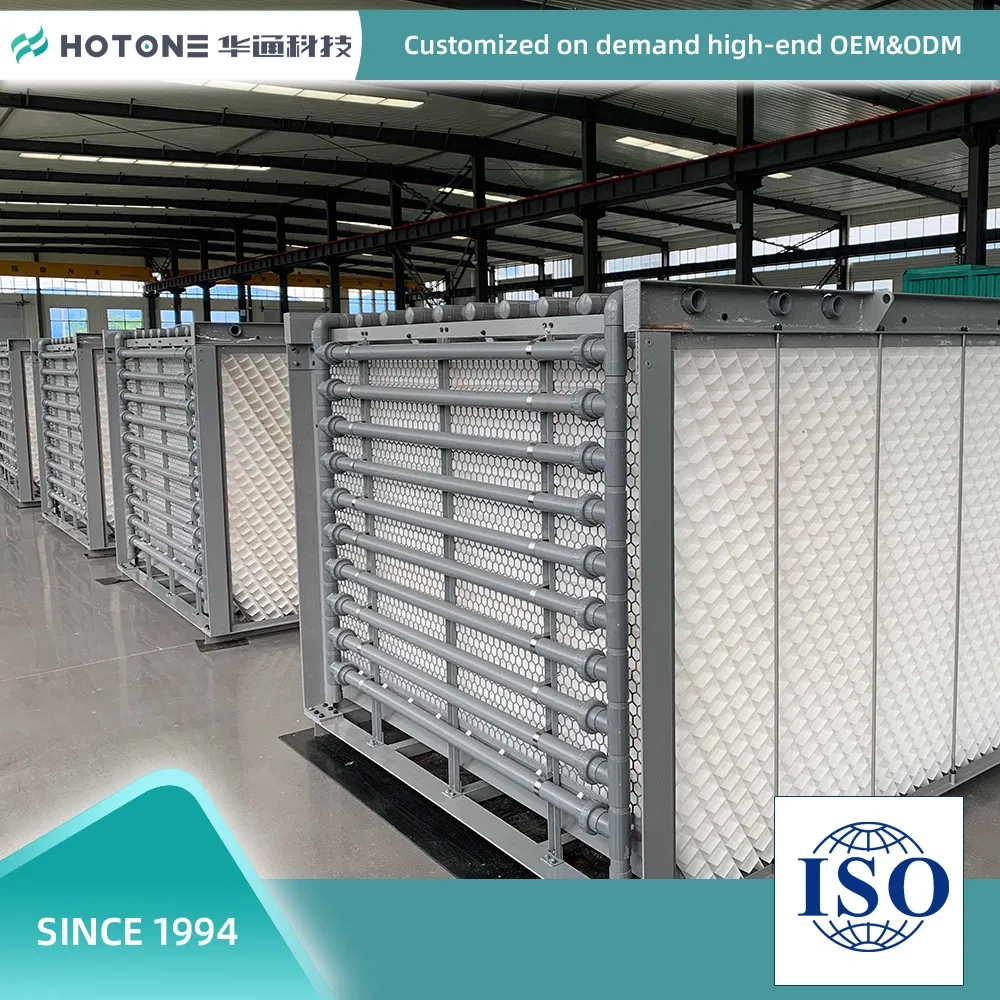
High Efficiency Water Tratment Solution for Chemical Industry Park
4.0InStock Source-listed auditby Shandong Hotone Environmental Technology Co., Ltd.
₹4,17,500≈ $5,000 · indicative, confirm with supplier
Payment
Description
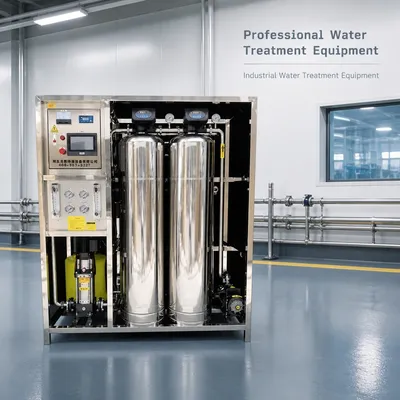
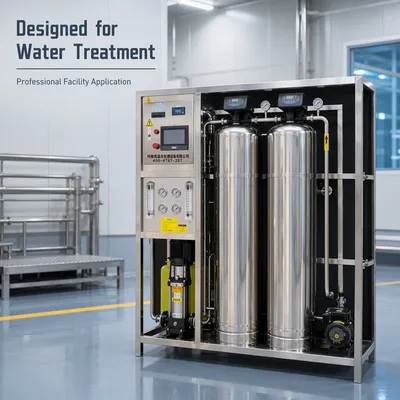
High Efficiency Water Tratment Solution for Chemical Industry Park. Patented Lateral Flow Technology: HOTONE's patented invention improves sedimentation and sludge discharge efficiency. High Efficiency Filtration: Achieves turbidity below 0.5 ntu with a capacity. Anti-Clogging Design: Independent mud-water flow channels prevent sedimentation media from clogging. Automatic Sludge Removal: Equipped with an automatic cleaning system to reduce manual maintenance workload. Customizable Modules: Offers customized sedimentation modules for different flows and limited spaces. Wide Application Scope: Suitable for both low-turbidity and high-turbidity raw water treatment. Durable Material Construction: Constructed with PP material and steel outer shell for long service life. ISO Certified Quality: Manufactured under ISO9001:2015, ISO14001, and ISO45001:2018 standards.
Specifications
TypeSedimentation
UsageWater Treatment Equipmentent
Model NO.50m3/day sedimentaion module-2
Motive ForcePressure
CustomizationAvailable