Loading…
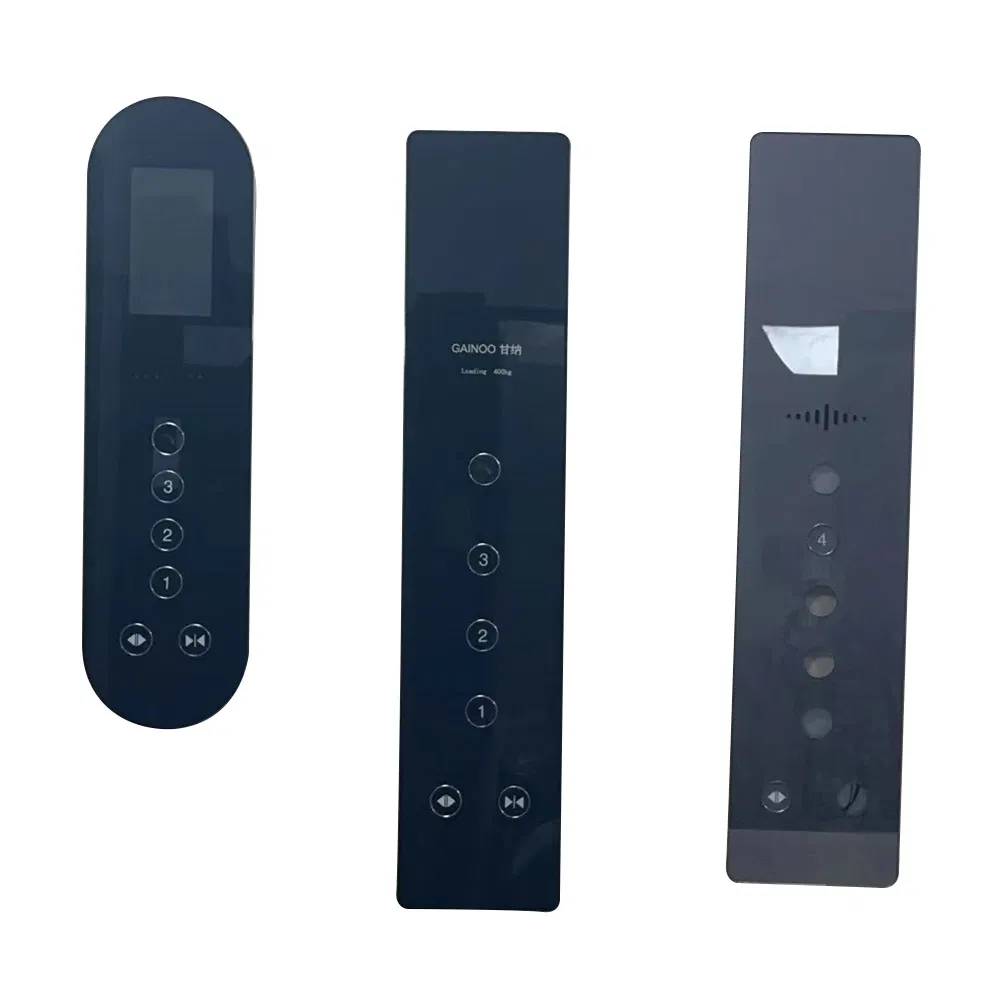
Elevator Spare Parts Manufacturer in China
5.0InStock Source-listed auditby Taicang Xinxing Machinery Factory
₹2,505≈ $30 · indicative, confirm with supplier
Payment
LC, T/T
Incoterms
FOB, EXW, CFR, CIF, DDP, DAP
Supplier information
Description
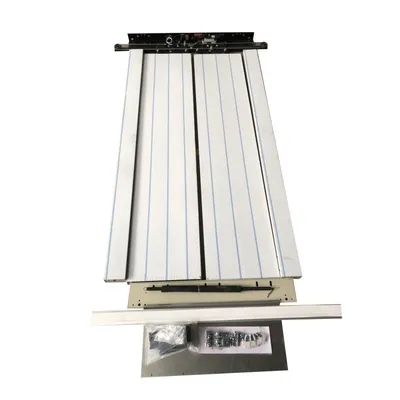
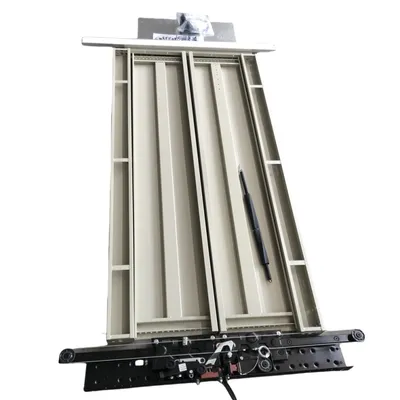
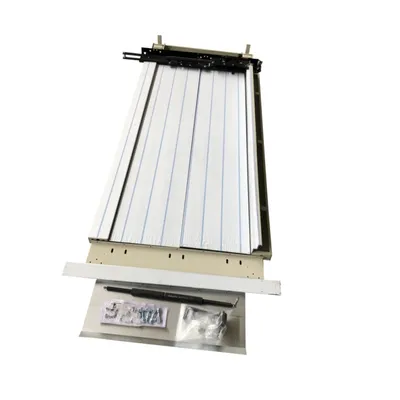
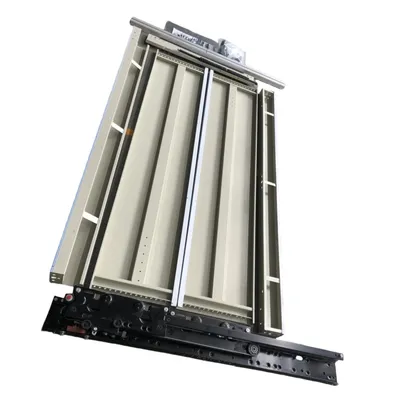
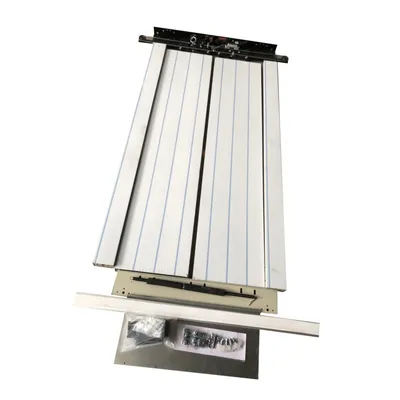
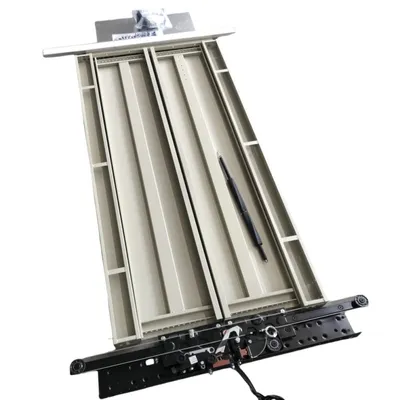
Elevator Spare Parts Manufacturer in China. 30+ Years Experience: Established in 2001 with over three decades of machinery industry expertise. ISO 9001 Certified: Products meet highest quality and reliability standards through rigorous certification. Comprehensive Safety System: Designed to meet highest safety standards for peace of mind during operation. Energy Efficient Electric System: Environmentally friendly design that reduces carbon footprint and saves energy. Global Export Experience: Leading exporter since 2008 with established relationships in worldwide markets. Precision Guide Rails: Built with precision and durability for smooth and reliable elevator operation. Secure Packaging Solutions: Products securely packaged to prevent damage during international transportation. Flexible Shipping Options: Supports EXW, FOB, CFR, CIF, and DDU terms with reliable global logistics partners.
Specifications
TypeSafety System
Warranty1year
Model NO.Elevator Spare Parts
CustomizationAvailable
After-sales Service1year