Loading…
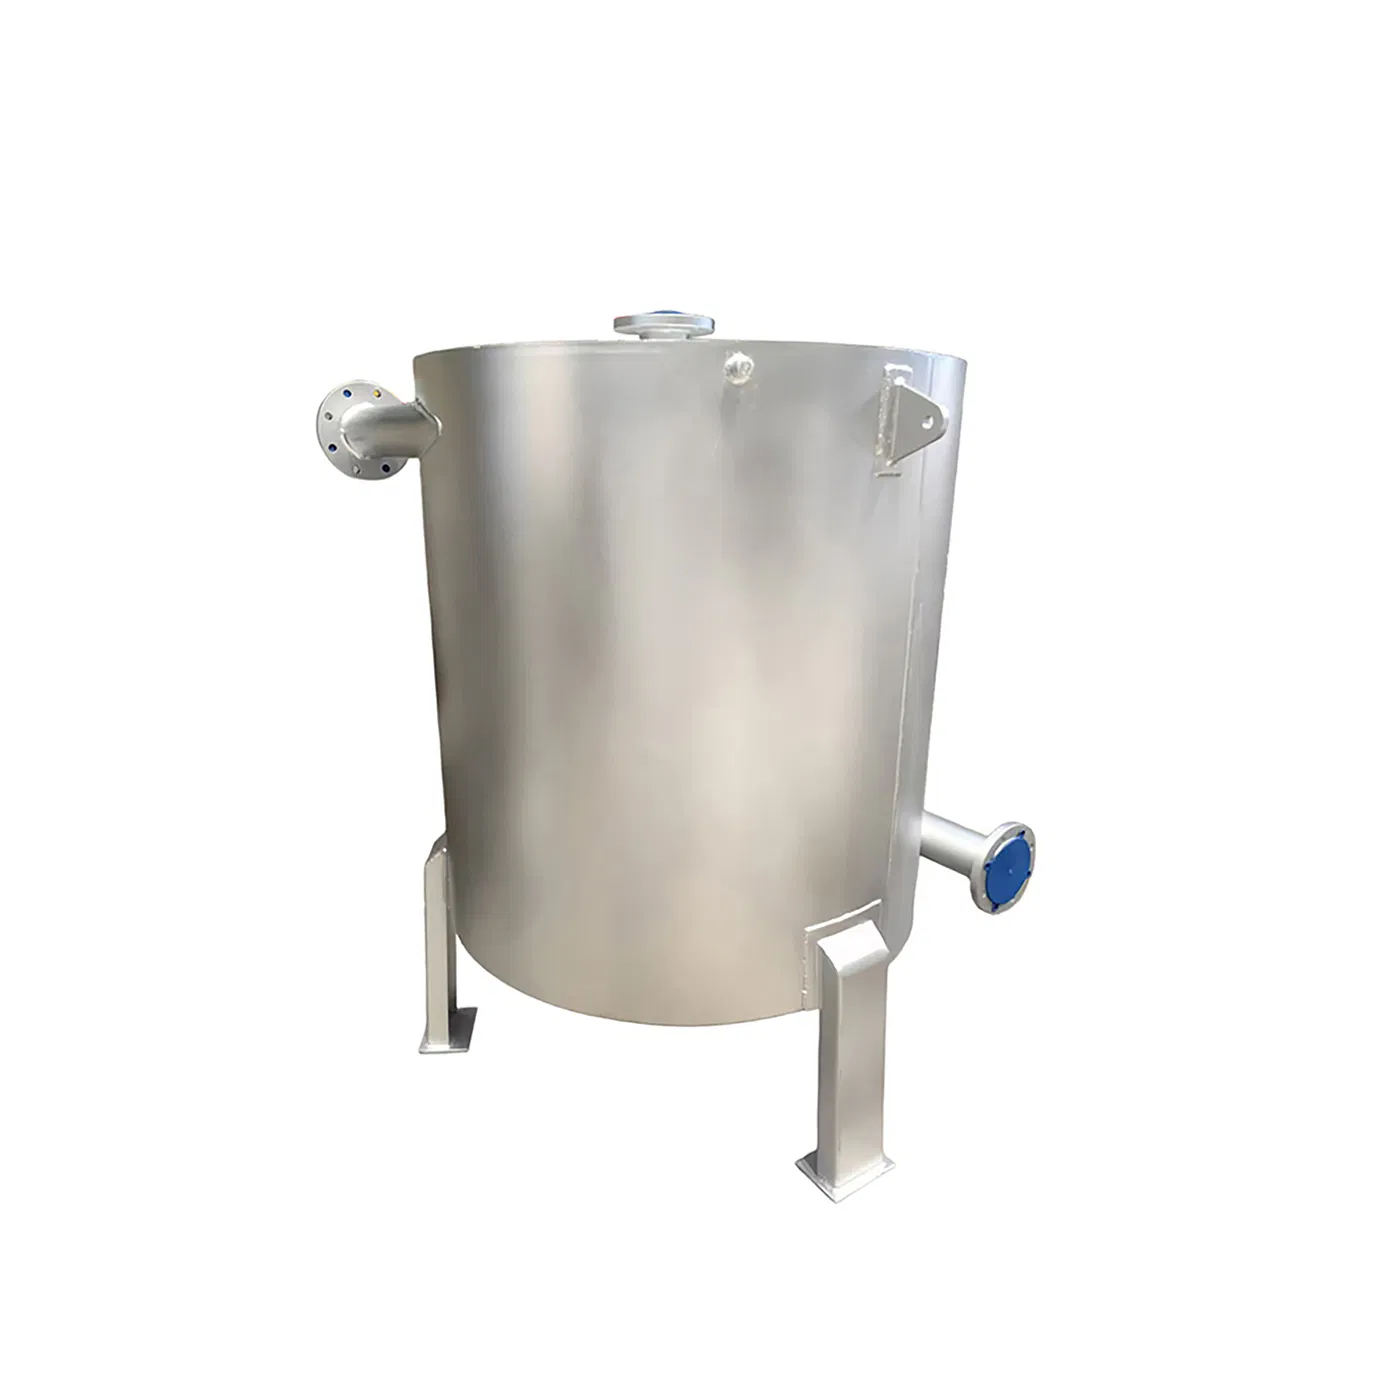
Innovative Spiral Heat Exchanger Equipment for Dairy and Chemical Processing
5.0InStock Source-listed auditby Shanghai Aibao Industrial Co., Ltd.
₹25,050≈ $300 · indicative, confirm with supplier
Payment
Description
Innovative Spiral Heat Exchanger Equipment for Dairy and Chemical Processing. High Efficiency: Delivers 1.5-3x heat-transfer efficiency of traditional shell-and-tube exchangers. Compact Design: Occupies only 1/10 of the volume of traditional units while maintaining performance. Anti-Fouling: Self-cleaning turbulence inhibits fouling and extends cleaning cycles. Wide Material Options: Available in Carbon Steel, Stainless Steel, Titanium, and Special Alloys. Customizable: Supports customization for application, design pressure, and temperature. Low Pressure Drop: Streamlined flow channels reduce resistance and energy consumption. High Sealing Reliability: Dual-seal structure minimizes leakage risk with fewer flange interfaces. Versatile Application: Suitable for viscous, corrosive, and particle-containing fluids.
Specifications
Warranty1 Year
Model NO.Spiral Type Heat Exchanger
CertificationCE, ISO
CustomizationAvailable
After-sales ServiceVideo Technical Support, Online Support