Loading…

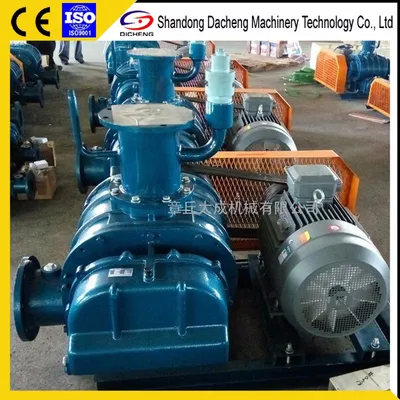
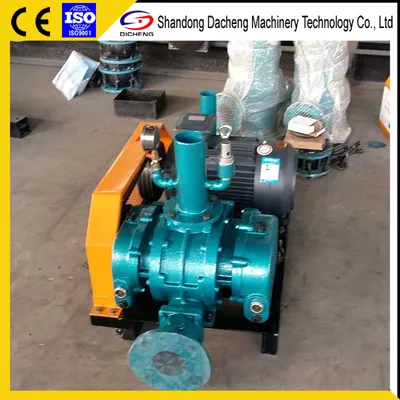
Water Ring Vacuum Pump for Chemical, Chemical Fertilizer, Paper and Pharmaceutical Industry
5.0InStock Source-listed auditby Shandong Kaien Vacuum Technology Co., Ltd.
₹19,623≈ $235 · indicative, confirm with supplier
Description
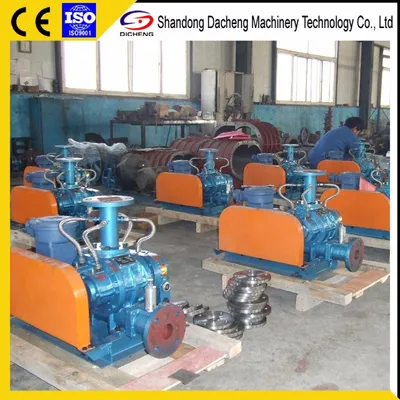
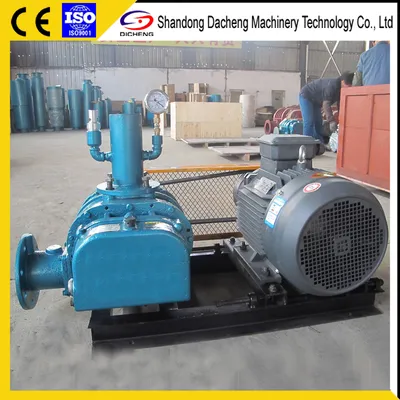
Water Ring Vacuum Pump for Chemical, Chemical Fertilizer, Paper and Pharmaceutical Industry. High Energy Efficiency: Developed with imported magnetic technology for high aiming energy performance. Simple Structure Design: Single machine single action structure ensures convenient maintenance and reliable operation. Corrosion Resistant Materials: Pump tree made of corrosion-resistant material or wrist rot MTS for handling corrosive gases. Explosive Gas Handling: Equipped with clear motor capable of sucking flammable and explosive gases safely. Wide Industry Application: Suitable for petrochemical, pharmaceutical, papermaking, food, and chemical fertilizer industries. High Vacuum Degree: Capable of achieving ultimate vacuum levels less than 0.001 Mbar or 3300 Pa. ISO 9001 Certified: Manufacturing process strictly managed in accordance with ISO 9001 quality system. Lifetime Paid Service: Provides lifetime paid after-sales service for long-term support.
Specifications
WarrantyOne Year
Model NO.2BE1
StructureWater Ring Vacuum Pump
Oil or NotOil Free
After-sales ServiceLifetime Paid Service