Loading…
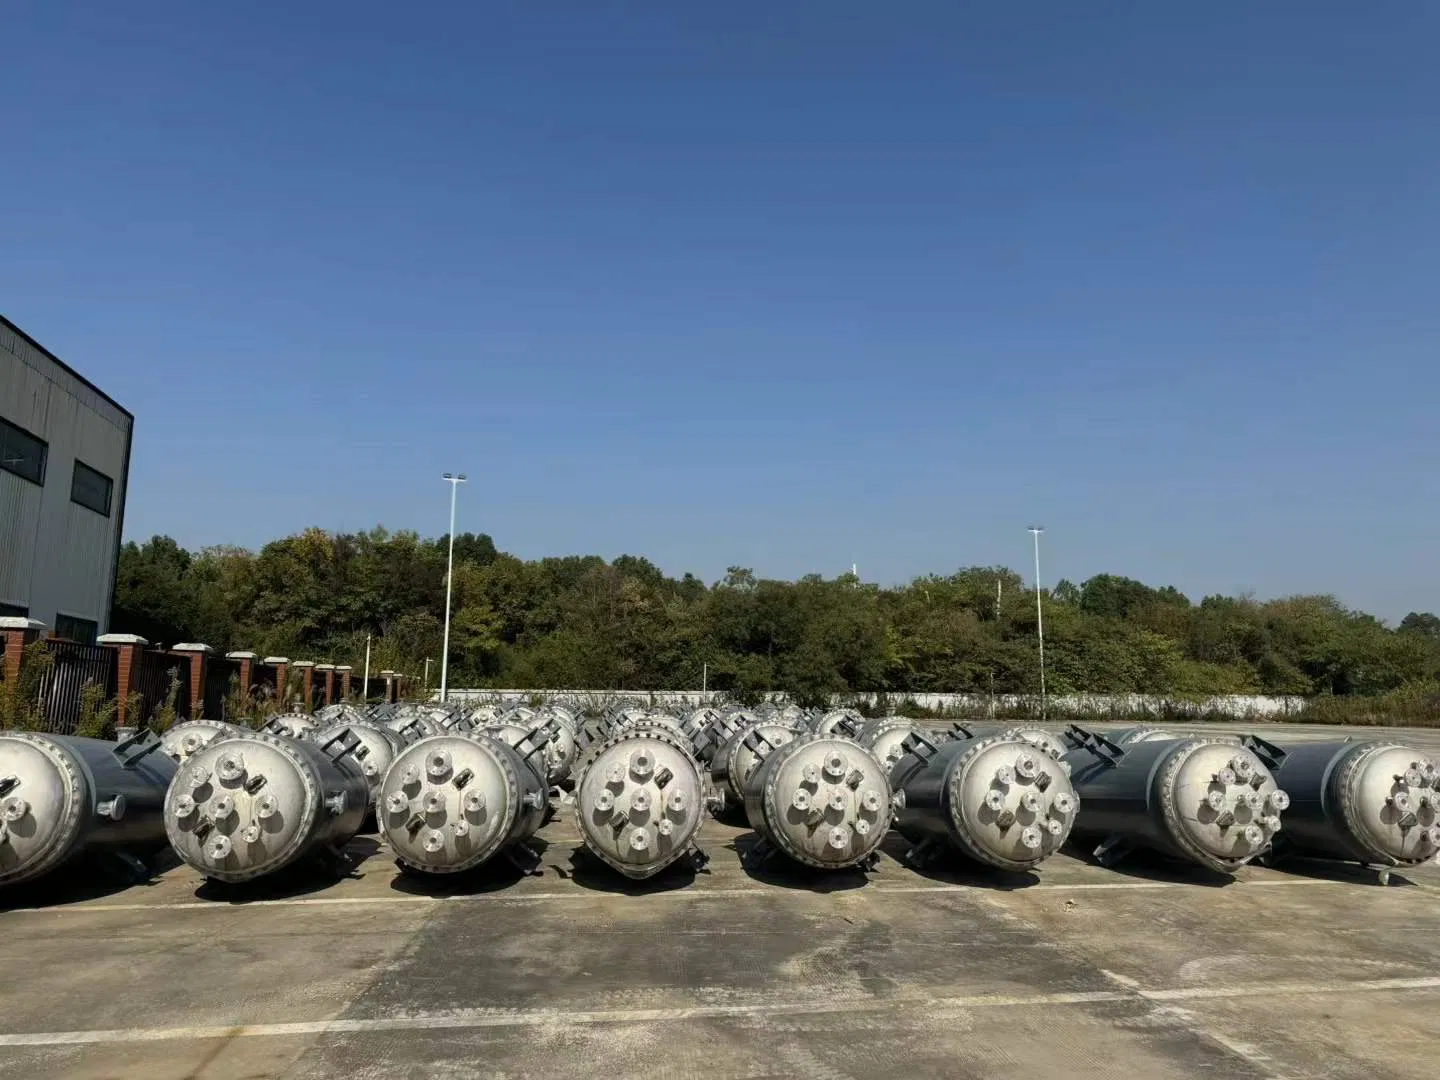
Industrial Double-Effect Heat Exchanger with ASME Certification
5.0InStock Source-listed auditby Jiangsu Xinmen Energy Equipment Co., Ltd.
₹8,35,000≈ $10,000 · indicative, confirm with supplier
Payment
LC, T/T
Incoterms
FOB, CIF, CFR, EXW
Description
Industrial Double-Effect Heat Exchanger with ASME Certification. 15+ Years R&D Experience: Deep expertise in heat exchanger design for high temp, pressure, and corrosion scenarios. Wide Material Selection: Customizable in 304/316L stainless steel, titanium, nickel alloys, and more. Multi-Industry Solutions: Serving 12 major industries including chemical, energy, food, and electronics. Strict Quality Control: 5 PMI machines, hydraulic testing, and non-destructive weld inspection. Global Certifications: Holds CE, ASME U Stamp, ISO 9001, PED, and FDA compliance. Flexible Customization: Supports customization from samples, designs, and full custom solutions. Cost-Effective Design: Design lifespan exceeds industry average with 50% lower maintenance costs. Direct Factory Supply: 15+ years manufacturing experience with in-house R&D and export license.
Specifications
WarrantyOne Year
ApplicationHeater, Cooler, Vaporizer
CertificationCE
CustomizationAvailable
After-sales ServiceOnline Guidance for Maintenance