Loading…
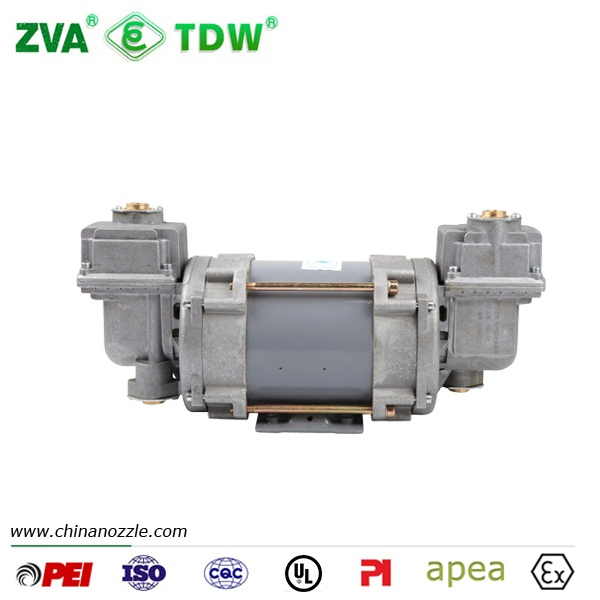
Dull Air Vacuum Vapour Recovery Pump for Vapor Recovery Dispenser
5.0InStock Source-listed auditby China Baotai Science and Technology Co., Ltd.
₹20,875≈ $250 · indicative, confirm with supplier
Payment
LC, T/T, Western Union
Description
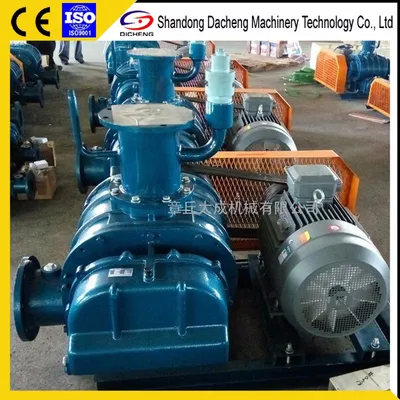
Dull Air Vacuum Vapour Recovery Pump for Vapor Recovery Dispenser. Integrated Flame Arrester: Prevents flame breakthrough in explosion-capable vapor/air mixtures for safety. Oil-Free Rotary Design: Dry working conditions with rotary vacuum pump structure for clean operation. High Flow Capacity: Max flow rate of 70L/min with vacuum degree suitable for vapor recovery. 100% Factory Tested: Every unit undergoes rigorous testing to ensure faultless function before delivery. Flexible Configuration: Available in single or double pump head options to suit different needs. OEM/ODM Support: Customization available for design, pressure settings, and flow rates. Low Noise Operation: Noise level kept below 70dB for a quieter working environment. Wide Voltage Range: Supports 220V/380V voltage inputs with 50Hz frequency compatibility.
Specifications
Model NO.TDW VRP-70
StructureRotary Vacuum Pump
Oil or NotOil Free
CustomizationAvailable
Exhauster MethodEntrapment Vacuum Pump