Loading…
Heavy-Duty Coal Conveyor System for Streamlined Loading Solutions
InStock Source-listed auditby Xuchang Zhihan Machinery Equipment Co., Ltd
₹1,25,250≈ $1,500 · indicative, confirm with supplier
Supplier information

Description
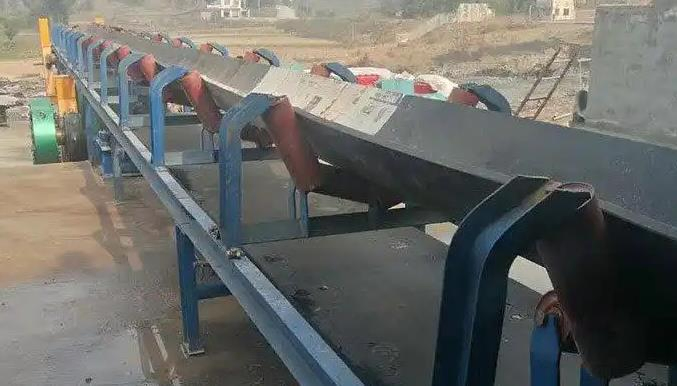
Heavy-Duty Coal Conveyor System for Streamlined Loading Solutions. Explosion-Proof Certification: Equipped with explosion-proof motors and fire-resistant belting for safe operation in coal dust and methane environments. Customizable Specifications: Conveying capacity, belt width, speed, and length can be tailored to specific customer requirements. Versatile Mining Application: Ideal for horizontal roadway transportation in fully mechanized, high-grade, and general conventional mining faces. Flame Retardant Material: Constructed with rubber belts featuring flame retardant and antistatic properties for enhanced safety. Flexible Transfer Integration: Tail section integrates bridge-type or belt-type transfer conveyors for seamless connection with face conveyors or roadheaders. High Capacity Options: Available in models ranging from 100 to 1000 tons per hour to meet diverse throughput needs. OEM and Customization Service: Full OEM support and machine customization available based on individual customer specifications. New Condition Guarantee: All units are supplied in brand new condition with the latest technical models.
Specifications
TypeBelt Conveyor
MaterialRubber
Model NO.DSS80/40/2*40
StructureBelt Conveyor
Material FeatureFlame Retardant/Antistatic