Loading…
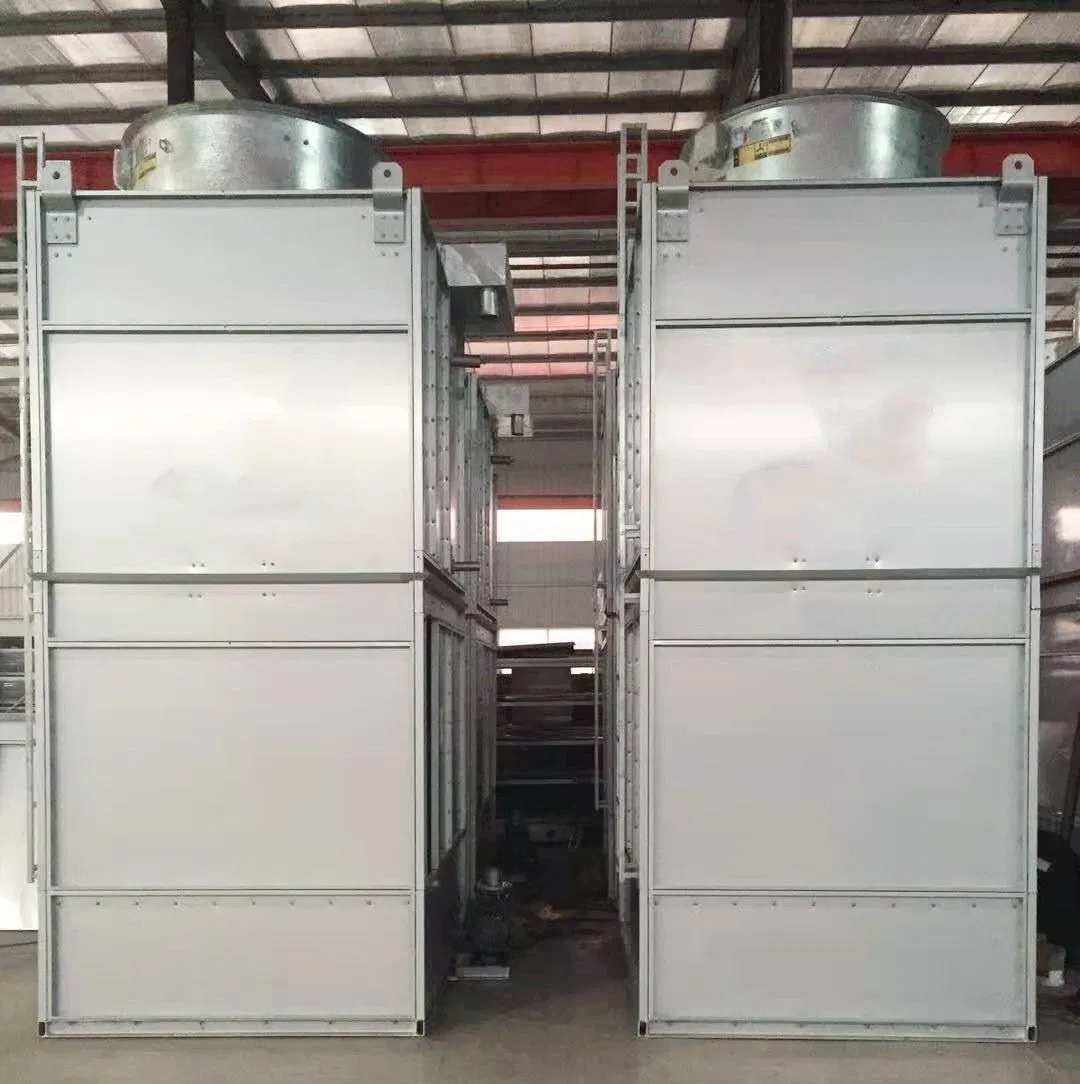
High Quality R717 Ammonia Evaporation Condenser Cold Storage Industrial Refrigeration Equipment Evaporative Condenser Counter Flow
5.0InStock Source-listed auditby Shandong Wanke Machinery Equipment Co., Ltd.
Description
High Quality R717 Ammonia Evaporation Condenser Cold Storage Industrial Refrigeration Equipment Evaporative Condenser Counter Flow. High Energy Efficiency: Condensation temperature approaches wet-bulb temperature, significantly lowering compressor power consumption. 80% Water Saving: Integrates cooling tower and condenser, saving over 80% of circulating water compared to traditional systems. Compact Design: Combines cooling tower and condenser into one unit, requiring a much smaller footprint than separate systems. Low Operating Costs: Eliminates need for separate cooling tower, large pumps, and complex piping, reducing initial investment. Customizable Components: Supports customization for frame, motor, nozzle, fan, casing, and drift eliminator materials. Versatile Applications: Suitable for industrial refrigeration, large-scale air conditioning, and power industry auxiliary cooling. Global After-Sales Support: 24/7 technical assistance, spare parts supply, and optional extended warranty up to 36 months. Tailored Engineering: Engineering team provides tailored designs and detailed CAD drawings for specific project requirements.
Specifications
TypeSteam Condenser
Model NO.SZL-300
Refrigerantas Customer Provide
CustomizationAvailable
Condensation FormsWater-Cooled