Loading…
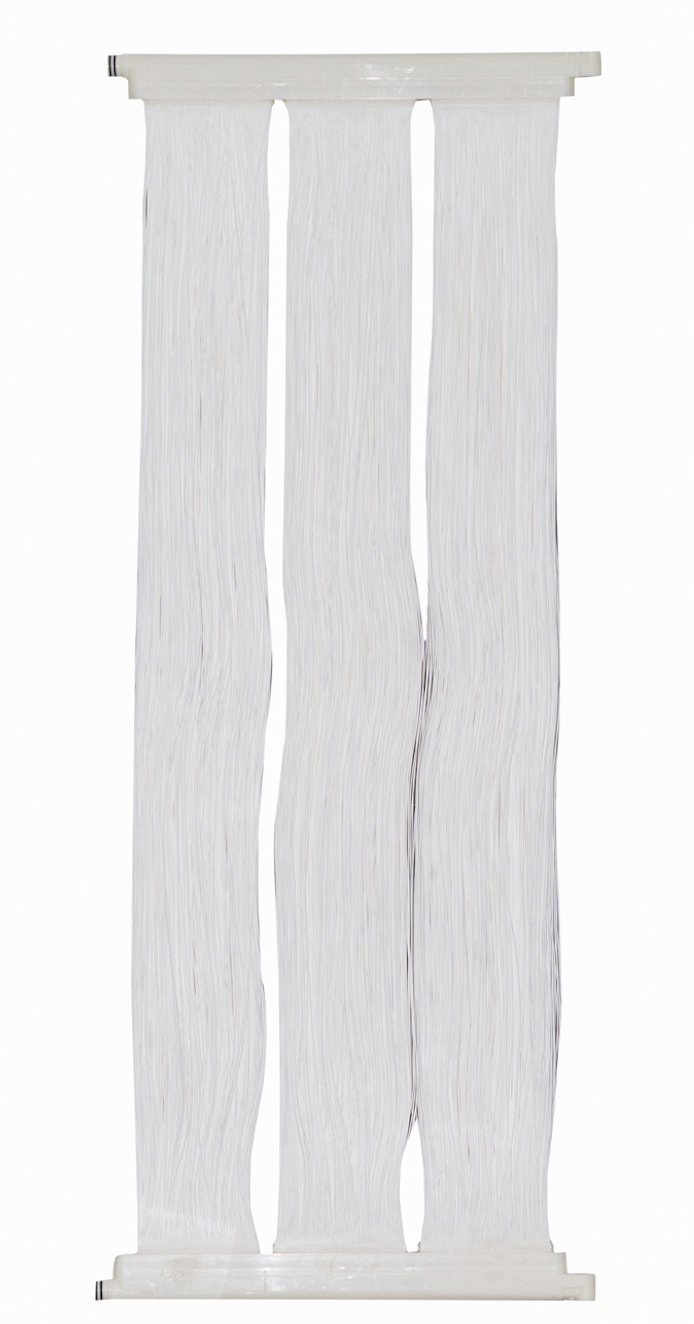
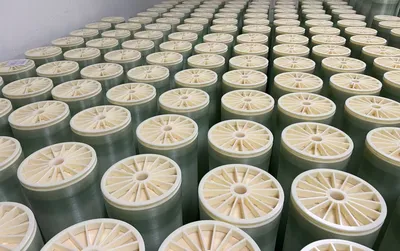
Innovative MBR Membrane Technology for Food and Beverage Wastewater
5.0InStock Source-listed auditby Ningbo Shuiyi Membrane Technology Development Co., Ltd.
₹5,010≈ $60 · indicative, confirm with supplier
Payment
Description
Innovative MBR Membrane Technology for Food and Beverage Wastewater. International Leading Performance: High operating flux, superior anti-fouling ability, and extended service life. High Mechanical Strength: Lining reinforced PVDF hollow fiber membrane ensures slower flux decline. Energy Efficient Design: Lower energy consumption with higher efficiency for cost-effective treatment. Modular & Easy Installation: Standardized modularization design allows for easy installment and replacement. Stable Water Production: Reliable performance with slower contamination speed and longer clean cycles. Versatile Application Scope: Suitable for municipal/industrial wastewater, landfill leachate, and RO pretreatment. Flexible Customization Options: Offers full, minor, and flexible customization from samples or designs. High-Quality Manufacturing: 100% finished product inspection with 8 QA/QC inspectors ensuring quality.
Specifications
TypeMF
MaterialPVDF Hollow Fiber
Model NO.SMU-30A
CustomizationAvailable
Membrane TypeHollow